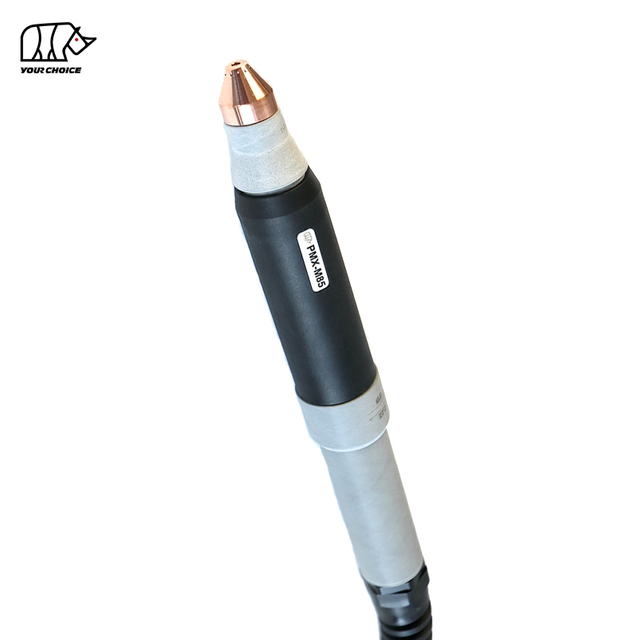
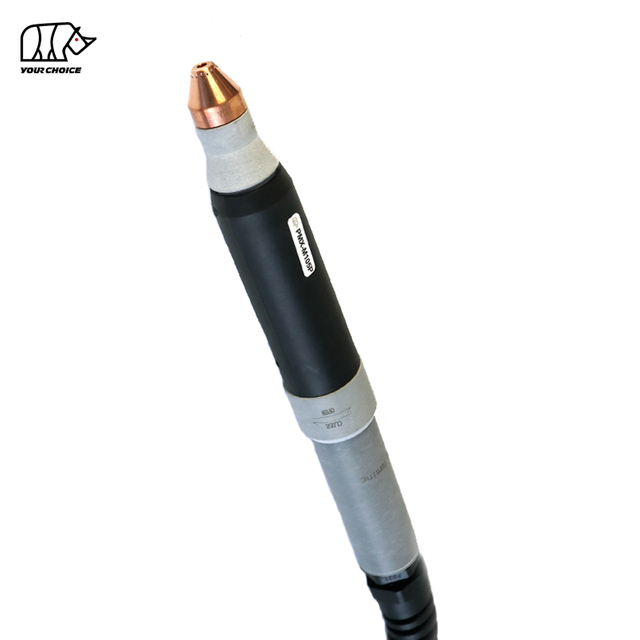
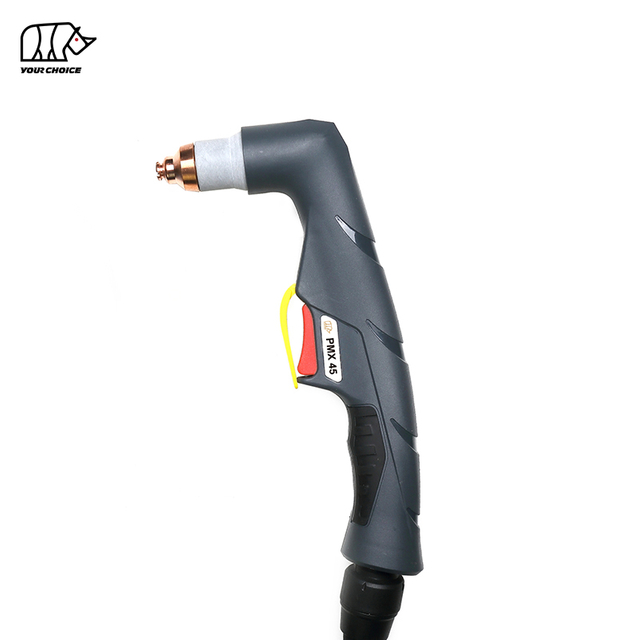
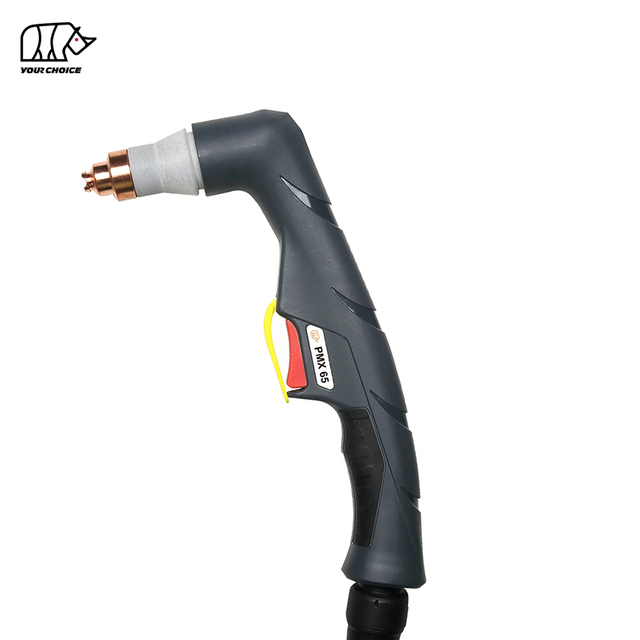
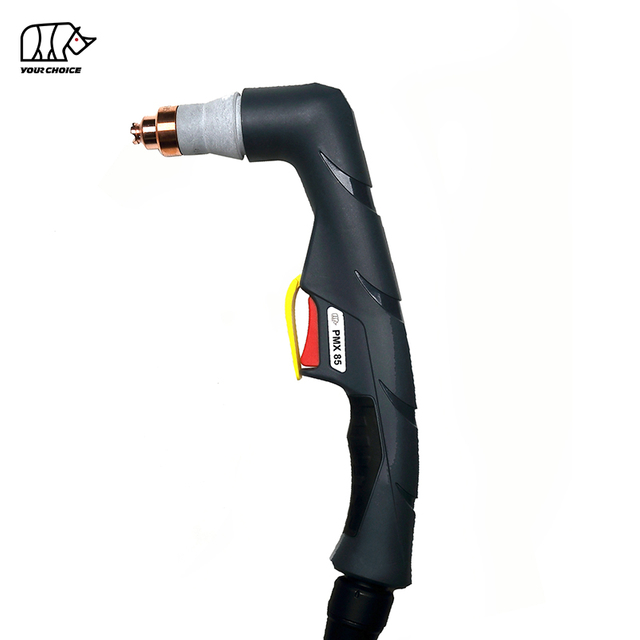
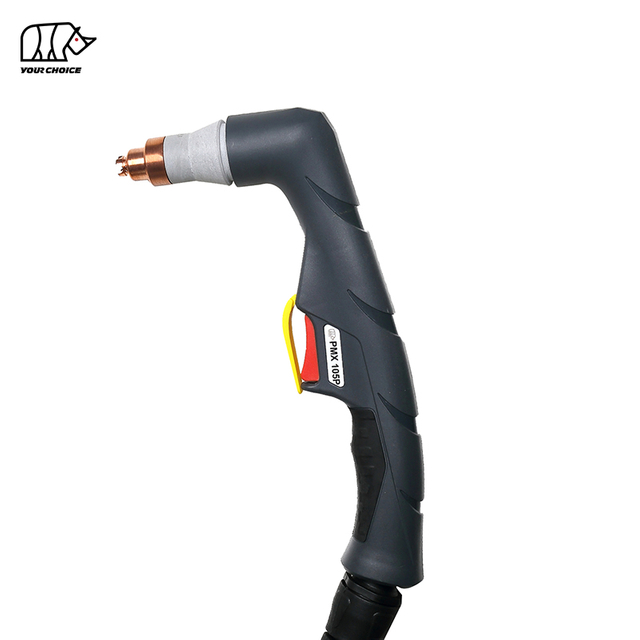
The INWELT PMX Series is a family of air-cooled, non-high-frequency plasma cutting torches designed for professional manual cutting and mechanized CNC applications.
The current range includes two main product groups:
Manual / Handheld Torches
PMX45 – 45A
PMX65 – 65A
PMX85 – 85A
PMX105 – 105A
CNC / Mechanized Torches
PMX-M45 – 45A
PMX-M65 – 65A
PMX-M85 – 85A
PMX-M105 – 105A
The series uses Air/N₂ as the process gas and supports multiple cutting-current levels, consumable configurations, cable assemblies and rear connections.
Manual and machine torches should be treated as separate product configurations even when they share related consumables.
| Model | Operation | Primary Current | Duty Cycle | Starting | Gas | Standard Lead |
|---|---|---|---|---|---|---|
| PMX45 | Manual | 45A | 60% | Non-HF | Air / N₂ | 6 m |
| PMX65 | Manual | 65A | 60% | Non-HF | Air / N₂ | 6 m |
| PMX85 | Manual | 85A | 60% | Non-HF | Air / N₂ | 6 m |
| PMX105 | Manual | 105A | 60% | Non-HF | Air / N₂ | 6 m |
| PMX-M45 | CNC / Machine | 45A | 60% | Non-HF | Air / N₂ | 6 m |
| PMX-M65 | CNC / Machine | 65A | 60% | Non-HF | Air / N₂ | 6 m |
| PMX-M85 | CNC / Machine | 85A | 60% | Non-HF | Air / N₂ | 6 m |
| PMX-M105 | CNC / Machine | 105A | 60% | Non-HF | Air / N₂ | 6 m |
The values above represent the primary current positioning of the current INWELT PMX range.
Higher-current variants such as PMX45P or PMX105P should be treated as separate products only when their technical specifications have been independently verified.
The handheld PMX range is designed for fabrication, repair, maintenance and industrial manual plasma cutting.
Current models include:
PMX45
PMX65
PMX85
PMX105
Manual torches include a hand grip, trigger and front-end consumable system designed for operator-controlled cutting.
Select the model according to:
Plasma power-source output
Cutting current
Starting system
Rear connector
Trigger wiring
Process-gas requirement
Required cutting or gouging process
The PMX45 is the lowest-current handheld model in the current PMX Series.
Current INWELT specifications include:
45A primary rated current
60% duty cycle
Non-HF arc starting
Air / N₂ process gas
Approx. 5.0 bar gas pressure
Approx. 160 L/min gas flow
Approx. 60-second recommended post-flow
6 m standard torch lead
Multiple rear-connector options
Current connection configurations can include:
1/4G integrated
1/4G separated
Central adapter
2-wire control
4-wire control
Coaxial configuration depending on assembly
The PMX45 is suitable for general fabrication, repair and lower-current metal-cutting applications when connected to a compatible plasma power source.
The PMX65 provides additional current capacity while retaining the same non-HF PMX platform concept.
Current specifications include:
65A rated current
60% duty cycle
Non-HF starting
Air / N₂ process gas
Approx. 5.0 bar gas pressure
Approx. 185 L/min gas flow
Approx. 60-second recommended post-flow
6 m standard lead
The PMX65 consumable platform supports lower-current and full-output cutting configurations, including 45A and 65A cutting tips.
This allows the torch to be configured according to the actual operating current rather than using one nozzle size for every application.
The PMX85 is designed for higher-current professional manual plasma cutting.
Current INWELT specifications include:
85A rated current
60% duty cycle
Non-HF arc starting
Air / N₂ process gas
Approx. 5.0 bar gas pressure
Approx. 230 L/min gas flow
Approx. 80-second recommended post-flow
6 m standard lead
The current consumable family covers:
45A
65A
85A
The corresponding typical nozzle diameters are approximately:
45A – Ø0.9 mm
65A – Ø1.1 mm
85A – Ø1.3 mm
Always use the verified tip and shield combination for the selected current.
The PMX105 is the highest-current standard handheld model in the current PMX Series.
It should be positioned primarily as a 105A product, separate from any higher-current PMX105P configuration.
Current INWELT specifications include:
105A primary rated current
60% duty cycle
Non-HF arc starting
Air / N₂ process gas
Approx. 5.0–5.5 bar gas pressure
Approx. 255 L/min gas flow
Approx. 120-second recommended post-flow
6 m standard lead
The current product family includes cutting consumables for several current ranges up to 105A.
A Ø1.5 mm tip is used as the current 105A full-output cutting configuration.
Do not automatically treat 125A-related consumables as the standard PMX105 rating.
The PMX-M models are dedicated machine-torch versions designed for:
CNC plasma tables
Automated profile cutting
Plate-processing systems
Mechanized fabrication
Production cutting cells
Current models include:
PMX-M45
PMX-M65
PMX-M85
PMX-M105
Machine torches use a straight-body configuration intended for fixed mounting rather than handheld operation.
The PMX-M45 is the lowest-current mechanized model in the current PMX-M range.
Current specifications include:
45A primary product positioning
60% duty cycle
Non-HF arc starting
Air / N₂ process gas
Approx. 5.0 bar operating pressure
Approx. 160 L/min gas flow
Approx. 60-second recommended post-flow
6 m standard lead
Machine / CNC torch configuration
Available complete-torch configurations currently include:
1/4G integrated / 2-wire
1/4G separated / 2-wire
Central adapter / 2-wire
Central adapter / coaxial cable
Any higher-current PMX-M45P configuration should remain separate unless technically verified.
The PMX-M65 is designed for 65A-class mechanized plasma cutting.
Current INWELT specifications include:
65A rated current
60% duty cycle
Non-HF starting
Air / N₂
Approx. 5.0 bar gas pressure
Approx. 185 L/min gas flow
Approx. 60-second recommended post-flow
6 m standard lead
Current consumables include both 45A and 65A machine-cutting configurations.
The full-output 65A PRO tip uses approximately a Ø1.1 mm nozzle orifice in the current INWELT system.
The PMX-M85 provides higher mechanized cutting capacity for CNC tables and automated plate processing.
Current INWELT specifications include:
85A rated current
60% duty cycle
Non-HF starting
Air / N₂
Approx. 5.0 bar gas pressure
Approx. 230 L/min gas flow
Approx. 80-second recommended post-flow
6 m standard lead
The current machine consumable family includes:
45A – approximately Ø0.9 mm
65A – approximately Ø1.1 mm
85A – approximately Ø1.3 mm
The exact INWELT tip, shield and retaining-component combination should be confirmed for each current level.
The PMX-M105 is the highest-current standard CNC model in the current PMX-M range.
It should be positioned primarily as:
PMX-M105 = 105A Non-HF CNC Plasma Cutting Torch
Current specifications include:
105A primary rated current
60% duty cycle
Non-HF starting
Air / N₂
Approx. 5.0–5.5 bar gas pressure
Approx. 255 L/min gas flow
Approx. 120-second recommended post-flow
6 m standard lead
Related cutting-current configurations include:
45A
65A
85A
105A
Any separate 125A PMX-M105P product should have its own product entity and technical page rather than being mixed into the standard PMX-M105 specification.
The main difference is how the torch is operated and mounted.
| Feature | PMX Manual Torch | PMX-M Machine Torch |
|---|---|---|
| Operation | Handheld | CNC / Mechanized |
| Torch Body | Operator handle | Straight machine body |
| Start Control | Torch trigger | Machine / CNC control |
| Mounting | Handheld | Torch holder / Z-axis |
| Cutting Height | Operator controlled | Machine controlled |
| Typical Models | PMX45 / 65 / 85 / 105 | PMX-M45 / 65 / 85 / 105 |
Do not install a manual torch as a substitute for a dedicated machine torch without verifying the complete system requirements.
The correct current class depends on the plasma power source and cutting requirement.
Primary current:
45A
Primary current:
65A
Primary current:
85A
Primary current:
105A
A higher-current torch does not automatically mean it should be used at full output for every cut.
The nozzle, shield and other consumables must be matched to the selected operating current.
The current INWELT PMX consumable system follows a current-specific nozzle approach.
Typical full-current relationships include:
| Cutting Current | Typical Tip Diameter |
|---|---|
| 45A | Ø0.9 mm |
| 65A | Ø1.1 mm |
| 85A | Ø1.3 mm |
| 105A | Ø1.5 mm |
The exact part number depends on torch model, manual/machine configuration and consumable family.
Do not select a plasma cutting tip only by physical appearance.
The cutting nozzle constricts the plasma arc.
Nozzle diameter affects:
Plasma-jet shape
Gas velocity
Kerf width
Current capacity
Consumable temperature
Using a low-current nozzle at excessive amperage can result in:
Rapid nozzle wear
Enlarged orifice
Unstable arc
Wider kerf
Poor cut quality
Use the nozzle specified for the selected current.
The electrode transfers electrical energy into the plasma arc.
The current PMX family uses replaceable electrodes matched to the relevant torch and consumable platform.
Inspect the electrode for:
Excessive central pit depth
Burning
Cracking
Contamination
Mechanical damage
An excessively worn electrode can accelerate nozzle wear and reduce arc-starting reliability.
The swirl ring controls the distribution and rotation of process gas around the electrode.
Correct gas swirl helps stabilize and constrict the plasma arc.
Different current classes can require different swirl-ring configurations.
Do not assume one swirl ring is correct for every PMX45–105 process.
Use the verified INWELT consumable relationship.
Manual and mechanized plasma cutting can require different front-end shield configurations.
Typical hand processes can include:
Drag cutting
Stand-off cutting
Gouging
Mechanized processes can require:
Machine cutting shield
Stand-off configuration
CNC retaining components
Process-specific front end
Do not automatically install a hand shield on a machine torch or a machine shield on a manual torch.
Selected PMX configurations can support plasma gouging when the correct consumables are installed.
Cutting consumables are designed to create a narrow plasma jet for material separation.
Gouging consumables create a wider arc for controlled metal removal.
Typical gouging applications include:
Weld removal
Defect removal
Back-gouging
Joint preparation
Repair and rework
Use the correct gouging nozzle and shield for the selected current.
The current INWELT PMX Series is positioned around non-high-frequency arc-starting systems.
This distinction is important for replacement projects.
A non-HF PMX torch should not automatically replace:
An HF torch
A different pilot-arc architecture
A torch with incompatible control wiring
Before replacement, confirm:
Starting method
Pilot-arc circuit
Plasma power-source output
Rear connector
Trigger or CNC wiring
CNC plasma systems can include sensitive electronics such as:
CNC controller
Torch-height controller
Motor drives
Computer interfaces
Signal cables
Non-HF plasma starting avoids the conventional high-frequency ignition architecture used by HF-start plasma systems.
However, non-HF operation alone does not guarantee CNC compatibility.
The complete power-source, torch and control system still needs to match.
Current INWELT PMX torches use:
Air / N₂
as the listed process-gas options.
Approximate current-category values are:
| Current Class | Pressure | Gas Flow |
|---|---|---|
| 45A | ~5.0 bar | ~160 L/min |
| 65A | ~5.0 bar | ~185 L/min |
| 85A | ~5.0 bar | ~230 L/min |
| 105A | ~5.0–5.5 bar | ~255 L/min |
Use clean, dry process gas according to the plasma power-source requirements.
Contaminated or moisture-laden compressed air can negatively affect consumable life and cutting consistency.
Current INWELT configurations list different recommended post-flow periods according to torch class.
| Current Class | Recommended Post-Flow |
|---|---|
| 45A | ~60 sec |
| 65A | ~60 sec |
| 85A | ~80 sec |
| 105A | ~120 sec |
Post-flow helps remove residual heat from the torch and consumables after cutting.
Allow the power source to complete its normal cooling cycle whenever possible.
The PMX range supports multiple rear-connection arrangements depending on the specific torch.
Available configurations can include:
1/4G integrated
1/4G separated
Central adapter
Custom adapter
2-wire control
4-wire control
Coaxial cable
Compatibility should never be determined only from thread size or connector appearance.
Confirm the complete interface.
Do not select a replacement torch only because the plasma cutter is labeled 45A, 65A, 85A or 105A.
Confirm the following.
The power source must operate within the verified range of the selected torch and consumables.
Confirm that the machine uses a compatible non-HF architecture.
Pilot-arc design can differ between plasma systems.
Check:
Thread
Central adapter
Power/gas path
Pilot connection
Manual and machine configurations can use different:
Trigger wires
Start signals
CNC interfaces
Confirm pressure and flow requirements.
For PMX-M machine torches, physical mounting dimensions are critical.
INWELT should publish first-party dimension drawings showing:
Torch-body diameter
Overall torch length
Clamping-zone length
Nozzle-to-clamp distance
Cable exit
Minimum clearance
These dimensions should be measured from actual INWELT production torches.
Do not copy another manufacturer's machine-torch drawing.
CNC plasma tables can use torch-height-control systems to manage cutting height.
Depending on the complete plasma system, height control can involve:
Initial-height sensing
Arc-voltage THC
Mechanical floating head
Other machine-specific sensing methods
Do not claim ohmic sensing compatibility unless the exact:
Shield
Retaining component
Electrical connection
CNC interface
has been verified for the INWELT configuration.
Mechanized plasma cutting commonly uses different torch heights during piercing and cutting.
The torch remains farther from the plate while molten material is expelled during arc penetration.
After piercing, the torch moves to the programmed cutting height.
Incorrect height can contribute to:
Excessive bevel
Dross
Nozzle damage
Poor dimensional accuracy
Reduced consumable life
Use verified process data from the complete plasma system.
A plasma torch alone does not define one universal cutting thickness.
Cutting capacity depends on:
Plasma power source
Current
Material
Nozzle
Gas pressure
Gas flow
Travel speed
Pierce height
Cutting height
Consumable condition
Required cut quality
Professional data should distinguish between:
Productive cutting with acceptable speed and edge quality.
Thicker material that can still be cut at lower speed.
Maximum thickness that can be separated, usually with reduced edge quality.
Do not publish one generic thickness figure for all PMX torches.
One of the strongest future SEO and GEO improvements would be verified INWELT cut charts.
Recommended fields include:
| Parameter | Data |
|---|---|
| Torch | PMX45 / 65 / 85 / 105 |
| Operation | Hand / Machine |
| Material | Mild Steel / Stainless / Aluminum |
| Thickness | mm |
| Current | A |
| Tip Part Number | INWELT Code |
| Tip Diameter | mm |
| Pressure | bar |
| Gas Flow | L/min |
| Travel Speed | mm/min |
| Pierce Height | mm |
| Cut Height | mm |
| Pierce Delay | sec |
| Kerf Width | mm |
| Result | Recommended / Maximum / Severance |
Use measured INWELT data rather than competitor cut charts.
When connected to a compatible plasma power source, PMX Series torches can cut electrically conductive materials including:
Mild steel
Carbon steel
Stainless steel
Aluminum
Copper
Brass
Galvanized steel
Actual cut performance depends on the complete plasma system.
Handheld PMX torches can be used for:
General fabrication
Repair
Maintenance
Structural steel
Agricultural equipment
Construction equipment
Automotive fabrication
Metal workshops
Field cutting
Select the torch according to the required current and power-source compatibility.
PMX-M machine torches are intended for:
CNC plasma tables
Automated plate cutting
Profile cutting
Sheet-metal production
Structural fabrication
Machinery components
Production cutting cells
Industrial automation
Machine integration should always consider torch dimensions, connector, starting system and control interface.
The PMX family is particularly suitable for aftermarket programs because one product family includes both complete torches and recurring replacement parts.
A professional distributor range can include:
Complete manual PMX torches
Complete PMX-M machine torches
45A cutting tips
65A cutting tips
85A cutting tips
105A cutting tips
Electrodes
Swirl rings
Shields
Retaining components
Torch heads
Cable assemblies
Central adapters
Gouging consumables
Exact part-number mapping helps reduce ordering errors.
Some PMX hand and machine configurations can share selected internal consumables.
However, the complete front-end system should not automatically be treated as identical.
Clearly distinguish:
Hand shield
Machine shield
Drag-cut configuration
Mechanized configuration
Gouging configuration
This is especially important on 45A, 65A, 85A and 105A product pages.
Replace electrodes before excessive erosion affects arc starting.
Check for:
Enlarged opening
Oval orifice
Heat damage
Burn damage
Replace cracked or damaged gas-distribution components.
Check for:
Damage
Blockage
Incorrect installation
Replace hardened or damaged seals.
Check for:
Abrasion
Heat damage
Tight bends
Loose fittings
Check:
Electrode
Cutting tip
Starting-system compatibility
Gas pressure
Work connection
Pilot-arc circuit
Check:
Travel speed
Current
Cutting height
Consumable condition
Gas flow
Check:
Torch angle
Nozzle wear
Cutting height
Machine-torch perpendicularity
Possible causes include:
Contaminated air
Incorrect current-to-nozzle combination
Excessive piercing
Incorrect height
Worn electrode
Check:
Torch mounting
Height control
Consumables
Kerf compensation
Motion-system accuracy
Travel speed
INWELT supplies PMX Series plasma cutting torches and consumables to professional B2B customers including:
Plasma power-source manufacturers
CNC plasma machine manufacturers
Welding and cutting equipment brands
CNC system integrators
Importers
Distributors
Wholesalers
Industrial suppliers
Aftermarket consumable brands
OEM and ODM configurations can be developed according to the target plasma system.
Customization may include:
Customer branding
Product labels
Manual or machine torch configuration
Cable length
Rear connector
Control wiring
Central adapter
Custom adapter
Consumable kits
Private-label packaging
Technical labels
Barcodes and cartons
For OEM projects, provide the plasma power-source model, output current, starting system, connector, control interface and estimated purchasing quantity.
The INWELT PMX Series combines four current classes with both handheld and CNC machine-torch configurations.
The current category includes:
PMX45
PMX65
PMX85
PMX105
PMX-M45
PMX-M65
PMX-M85
PMX-M105
45A–105A primary current classes
Non-HF starting
Air / N₂ operation
6 m standard torch leads
Manual and mechanized consumables
Cutting and gouging components
Multiple connector options
OEM and private-label supply
For equipment manufacturers and distributors, sourcing complete torches and related consumables from one manufacturer can simplify procurement and aftermarket support.
The current range includes:
Manual
PMX45
PMX65
PMX85
PMX105
CNC / Machine
PMX-M45
PMX-M65
PMX-M85
PMX-M105
The current INWELT PMX Series is positioned as a non-HF plasma torch family.
The main current classes are:
45A
65A
85A
105A
PMX models are handheld/manual torches.
PMX-M models are straight-body CNC/mechanized torches.
The current INWELT configurations list:
Air / N₂
as process-gas options.
Current standard configurations use approximately:
6 m
A typical current PMX configuration uses an approximately:
Ø0.9 mm tip
A typical current PMX configuration uses an approximately:
Ø1.1 mm tip
A typical current PMX configuration uses an approximately:
Ø1.3 mm tip
A typical current PMX configuration uses an approximately:
Ø1.5 mm tip
Exact part numbers depend on torch and process configuration.
The standard PMX105 should be treated as a 105A-class torch.
Higher-current PMX105P / 125A-related components should be treated as a separate configuration unless explicitly verified.
The standard PMX45 should be treated primarily as a 45A product.
Any PMX45P / 65A configuration should be verified and treated separately.
Some internal consumables can be related, but hand shields, machine shields and process-specific front-end components may differ.
Always confirm the complete consumable stack.
No.
Starting system, pilot-arc circuit, connector, control wiring and gas requirements must also match.
Yes, when used with a compatible plasma power source and appropriate process settings.
Yes.
Aluminum is electrically conductive and can be plasma cut with an appropriate plasma system.
There is no universal torch-only thickness.
Cutting capacity depends on the complete plasma system, material, operating current and process parameters.
Yes.
OEM/ODM, private-label, connector, cable, control-interface and consumable-kit configurations are available for qualified B2B customers.
For faster product selection and compatibility confirmation, provide:
Plasma power-source manufacturer
Machine model
Rated output current
Existing torch model
Manual or CNC application
Starting-system type
Main connector photograph
Control-connector photograph
Required cable length
Cutting or gouging requirement
Required consumables
Estimated purchasing quantity
INWELT or private-label branding
INWELT can then recommend the appropriate PMX or PMX-M torch, cable, connector and consumable configuration for your plasma cutting system.