The INWELT BZL Series is a family of MB-style MIG/MAG welding torches developed for professional fabrication, production welding, maintenance and industrial aftermarket applications.
The current product range includes:
MB15 – 180A CO₂ gas-cooled MIG torch
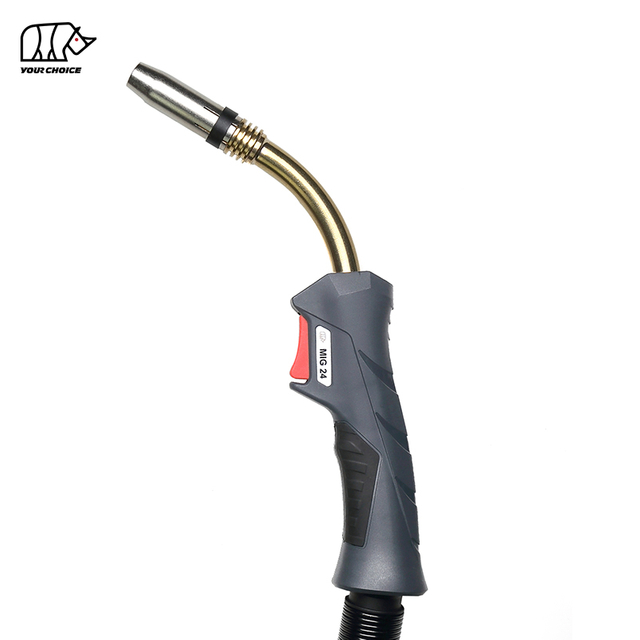
MB24 – 250A CO₂ gas-cooled MIG torch
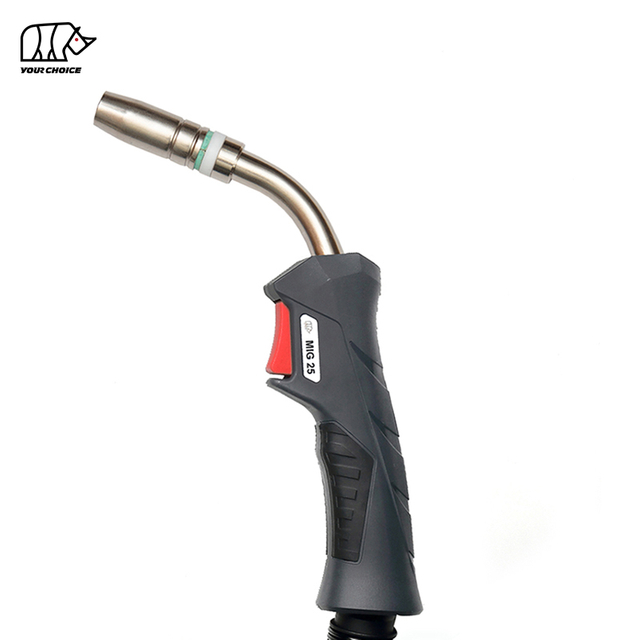
MB25 – 230A CO₂ gas-cooled MIG torch
MB36 – 340A CO₂ gas-cooled MIG torch
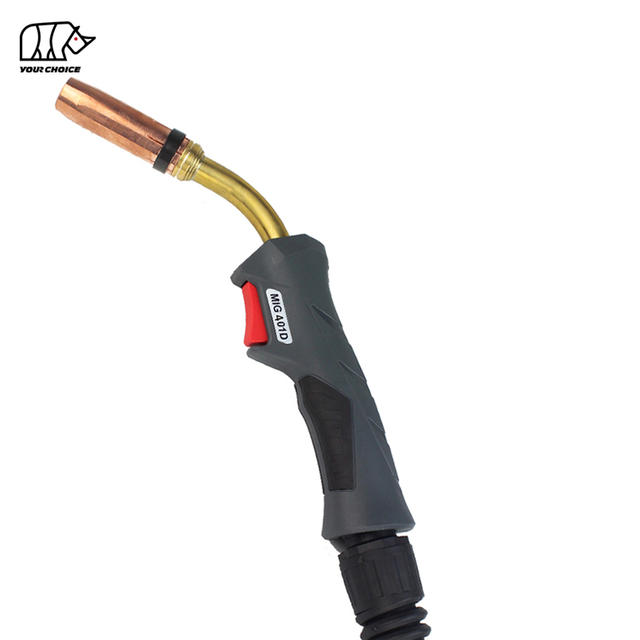
MB401D – 400A CO₂ water-cooled MIG torch
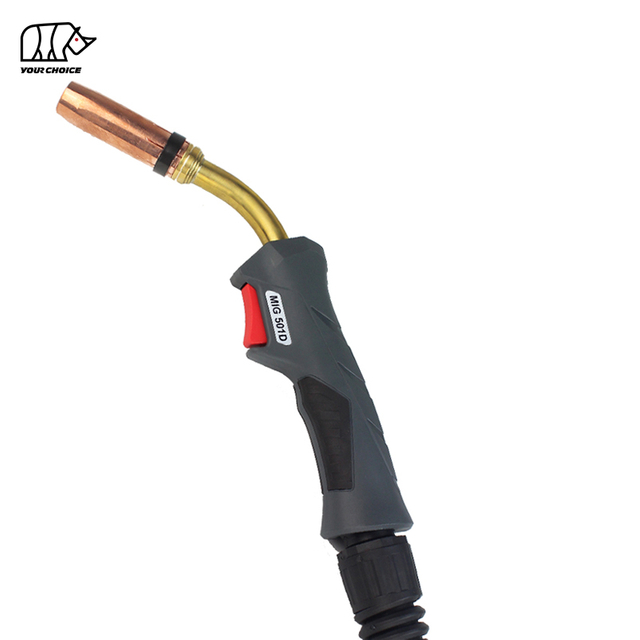
MB501D – 500A CO₂ water-cooled MIG torch
The range covers light- and medium-duty manual welding through higher-current continuous production applications.
Each model has its own verified current rating, shielding-gas rating, duty cycle, wire-size range and consumable configuration.
| Model | Cooling | CO₂ Rating | Mixed-Gas Rating | Duty Cycle | Wire Size | Cable Length |
|---|---|---|---|---|---|---|
| MB15 | Gas Cooled | 180A | 150A | 60% | 0.6–1.0 mm | 3 / 4 / 5 m |
| MB24 | Gas Cooled | 250A | 220A | 60%* | 0.8–1.2 mm | 3 / 4 / 5 m |
| MB25 | Gas Cooled | 230A | 200A | 60% | 0.8–1.2 mm | 3 / 4 / 5 m |
| MB36 | Gas Cooled | 340A | 300A | 60% | 0.8–1.6 mm | 3 / 4 / 5 m |
| MB401D | Water Cooled | 400A | 350A | 100% | 0.8–1.2 mm | 3 / 4 / 5 m |
| MB501D | Water Cooled | 500A | 450A | 100% | 1.0–1.6 mm | 3 / 4 / 5 m |
*Ratings shown above are current INWELT product specifications. Always use the individual INWELT product page and technical data when selecting a torch.
Gas-cooled torches provide a relatively simple and lightweight solution because they do not require a separate coolant circulation system.
The current INWELT gas-cooled range includes MB15, MB24, MB25 and MB36.
The MB15 is the most compact torch in the current BZL Series.
Current INWELT specifications include:
180A with CO₂
150A with mixed gas
60% duty cycle
0.6–1.0 mm welding wire
3 m / 4 m / 5 m cable options
Euro central connector
The MB15 is particularly suitable where lower torch weight and maneuverability are important.
Typical applications include:
Sheet-metal fabrication
Automotive repair
General maintenance
Light structural work
Workshop welding
The MB24 provides additional welding-current capacity while retaining a compact gas-cooled structure.
Current INWELT specifications include:
250A with CO₂
220A with mixed gas
60% duty cycle
0.8–1.2 mm welding wire
3 m / 4 m / 5 m cable options
Euro central connector
The MB24 is suited to medium-duty fabrication and production welding.
Because MB24 ratings can vary between manufacturers and product platforms, use the INWELT specification rather than assuming all MB24-style torches have identical duty-cycle ratings.
The MB25 combines medium-current welding capability with an air-cooled torch body.
Current specifications include:
230A with CO₂
200A with mixed gas
60% duty cycle
0.8–1.2 mm welding wire
3 m / 4 m / 5 m cable options
Euro central connector
The MB25 is suitable for general fabrication, machinery repair, production welding and industrial maintenance.
The MB36 is the highest-current gas-cooled model in the current INWELT BZL category.
Current specifications include:
340A with CO₂
300A with mixed gas
60% duty cycle
0.8–1.6 mm welding wire
3 m / 4 m / 5 m cable options
Euro central connector
Its higher current rating makes it relevant for heavier fabrication where a gas-cooled torch is preferred.
The torch, contact tip, liner, wire feeder and shielding gas should always be matched to the actual welding current and wire diameter.
Water-cooled MIG torches use circulating coolant to manage heat during higher-current or longer-duration welding.
The current INWELT water-cooled BZL range includes MB401D and MB501D.
A compatible welding-water cooler is required for proper operation.
The MB401D is designed for high-current industrial MIG/MAG welding.
Current INWELT specifications include:
400A with CO₂
350A with mixed gas
100% duty cycle
0.8–1.2 mm welding wire
3 m / 4 m / 5 m cable options
Euro central connector
Water-cooled construction
The MB401D is suitable for production environments where heat accumulation would make a smaller gas-cooled torch impractical.
Typical applications include:
Production welding
Heavy machinery
Structural fabrication
Industrial equipment
Longer welding cycles
The MB501D is the highest-current torch currently displayed in the INWELT BZL Series.
Current specifications include:
500A with CO₂
450A with mixed gas
100% duty cycle
1.0–1.6 mm welding wire
3 m / 4 m / 5 m cable options
Euro central connector
Water-cooled construction
The MB501D is intended for high-current production welding where continuous coolant circulation and heavier-duty consumables are required.
The correct cooling system depends on welding current, duty cycle, production requirements and operator priorities.
| Feature | Gas-Cooled BZL Torches | Water-Cooled BZL Torches |
|---|---|---|
| Current Range in Current Category | 180A–340A CO₂ | 400A–500A CO₂ |
| Cooling System | Ambient / gas-cooled torch design | Active liquid cooling |
| External Water Cooler | Not required | Required |
| Typical Duty Cycle | Model-specific, commonly 60% | 100% on MB401D / MB501D |
| Torch Weight / Complexity | Generally lower | Higher system complexity |
| Typical Use | General fabrication and repair | Higher-current production |
Do not select cooling method only from amperage.
Consider welding duration, operator movement, available cooling equipment, cable length and production requirements.
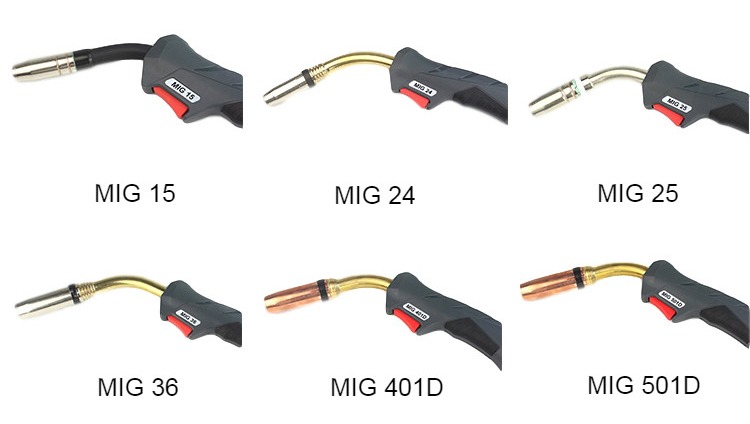
Choosing the correct MIG torch requires several parameters to be considered together.
Match the torch rating to the actual welding current.
Current BZL models range from 180A to 500A CO₂.
Do not continuously operate a torch above its verified rating.
Torch ratings can differ between:
CO₂
Mixed shielding gas
Always compare the correct gas-specific rating.
Duty cycle is especially important in production environments.
A higher current rating does not automatically mean the torch can operate continuously at that current.
Current INWELT wire ranges include:
0.6–1.0 mm
0.8–1.2 mm
0.8–1.6 mm
1.0–1.6 mm
The contact tip, liner and wire-feed system must match the selected wire diameter.
Choose a gas-cooled torch for simpler, lower-maintenance installations where the required current and duty cycle allow it.
Choose a water-cooled torch when higher current or extended production welding requires active heat removal.
Current models are available in:
3 m
4 m
5 m
Custom lengths can be evaluated for OEM projects.
Current INWELT BZL torches use Euro-style central connections on standard configurations.
A Euro central connector can combine several torch functions into one rear interface, simplifying installation and replacement on compatible MIG/MAG welding machines.
However, a Euro-style connector alone does not guarantee complete compatibility.
Before ordering, confirm:
Connector geometry
Wire-feed interface
Trigger circuit
Gas connection
Water connections on water-cooled models
Liner and wire size
For replacement projects, send photographs of the existing torch connector and machine interface.
The INWELT BZL range is supported by replacement consumables and service parts.
Depending on model, components include:
Gas nozzles
Contact tips
Contact-tip holders
Gas diffusers
Insulators
Torch necks
Liners
Handles
Triggers
Cable assemblies
Euro central adapters
Water connections
Cooling hoses
Exact components should always be selected by torch model and part number.
The contact tip transfers welding current to the electrode wire and guides the wire into the welding arc.
Select the contact tip according to:
Welding wire diameter
Wire material
Torch model
Contact-tip thread
Welding current
Common BZL configurations use model-specific M6 or M8 contact-tip systems.
Do not select a contact tip only by wire diameter.
The thread and tip-holder design must also match.
The liner guides welding wire through the torch cable assembly.
Correct liner selection is important for stable wire feeding.
Consider:
Wire diameter
Wire material
Torch length
Wire-feed system
Liner internal diameter
Steel, stainless and aluminum welding applications may require different liner materials or configurations.
A worn, contaminated or incorrectly sized liner can contribute to:
Irregular wire feeding
Bird-nesting
Increased wire resistance
Arc instability
Premature contact-tip wear
The gas nozzle directs shielding gas around the welding arc and molten weld pool.
The diffuser distributes shielding gas through the front end of the torch.
Correct selection and maintenance help support consistent shielding.
Inspect the nozzle and diffuser for:
Heavy spatter
Distortion
Heat damage
Blocked gas passages
Loose installation
Cleaning frequency should be based on actual welding conditions rather than a universal operating-hour interval.
There is no single replacement interval that applies to every BZL torch or welding application.
Consumable life depends on factors including:
Welding current
Duty cycle
Wire type
Wire diameter
Shielding gas
Spatter level
Welding position
Liner condition
Contact-tip quality
Operator technique
Replace components based on wear and welding performance.
Typical signs that inspection is required include:
Unstable arc
Irregular wire feeding
Excessive spatter
Burned contact tip
Damaged gas nozzle
Poor gas coverage
Increased electrical resistance
BZL MIG/MAG torches can be configured for different welding-wire systems.
Common applications include:
Carbon steel
Stainless steel
Aluminum
The torch itself does not determine weldability.
Wire type, liner, contact tip, shielding gas, wire feeder, welding machine and process parameters must all be selected for the base material.
For aluminum welding, pay particular attention to liner material and wire-feed resistance.
Depending on model and welding rating, the BZL Series can support applications including:
General metal fabrication
Automotive manufacturing and repair
Structural fabrication
Agricultural machinery
Construction equipment
Truck and trailer production
Machinery manufacturing
Metal furniture
Industrial maintenance
Production welding
The correct torch should be selected according to current, duty cycle, wire size and production requirements rather than industry name alone.
The four gas-cooled models serve different welding-current requirements.
| Model | CO₂ Rating | Mixed Gas | Wire Size | Positioning |
|---|---|---|---|---|
| MB15 | 180A | 150A | 0.6–1.0 mm | Compact / lower-current |
| MB25 | 230A | 200A | 0.8–1.2 mm | General fabrication |
| MB24 | 250A | 220A | 0.8–1.2 mm | Medium-current fabrication |
| MB36 | 340A | 300A | 0.8–1.6 mm | Higher-current gas-cooled |
This table uses current INWELT ratings.
Other manufacturers may publish different ratings for similarly named MB-style torches.
The main difference is welding-current capacity and supported wire range.
| Model | CO₂ Rating | Mixed Gas | Duty Cycle | Wire Size |
|---|---|---|---|---|
| MB401D | 400A | 350A | 100% | 0.8–1.2 mm |
| MB501D | 500A | 450A | 100% | 1.0–1.6 mm |
Choose MB401D when 400A-class capacity is sufficient.
Choose MB501D for higher-current welding within the verified 500A-class rating.
Both require a compatible water-cooling system.
Do not select a replacement torch from the model name alone.
Confirm:
Compare the required CO₂ or mixed-gas current with the torch rating.
Make sure the torch can support the required welding duration.
Match wire, contact tip and liner.
Verify the Euro central connection and machine interface.
For MB401D and MB501D, confirm water-cooler availability and coolant connections.
Select the appropriate 3 m, 4 m or 5 m cable.
Confirm the torch neck, contact-tip thread, tip holder, gas diffuser and nozzle configuration.
INWELT supplies MIG/MAG welding torches and consumables to professional B2B customers including:
Welding machine manufacturers
Welding equipment brands
Importers
Distributors
Wholesalers
Industrial suppliers
Repair companies
Aftermarket consumable brands
OEM and ODM configurations can be evaluated according to the target welding system and market.
Customization may include:
Customer branding
Handle color
Product labels
Cable length
Rear connector
Consumable kits
Wire-liner configuration
Private-label packaging
Manuals
Barcodes
Carton requirements
For OEM projects, provide the target welding machine, required current, wire size, connector and estimated order quantity.
The INWELT BZL program combines multiple current classes, cooling methods and replacement parts within one supply system.
The current category includes:
180A gas-cooled torch
230A gas-cooled torch
250A gas-cooled torch
340A gas-cooled torch
400A water-cooled torch
500A water-cooled torch
3 m / 4 m / 5 m cable options
Euro central connectors
Contact tips
Gas nozzles
Diffusers
Liners
Torch heads
Cable assemblies
OEM/private-label supply
For equipment brands and distributors, sourcing complete torches and replacement consumables through the same supplier can simplify inventory and aftermarket support.
The current range includes:
MB15
MB24
MB25
MB36
MB401D
MB501D
The current gas-cooled models are:
MB15
MB24
MB25
MB36
The current water-cooled models are:
MB401D
MB501D
The current INWELT MB501D is rated at 500A with CO₂ and 450A with mixed gas at 100% duty cycle.
The MB15 is rated at 180A with CO₂ and 150A with mixed gas.
Current standard configurations include:
3 m
4 m
5 m
OEM lengths can be evaluated separately.
Current standard INWELT BZL configurations use Euro-style central connectors.
Always verify the actual machine interface before ordering.
No.
MB15, MB24, MB25, MB36, MB401D and MB501D use model-specific combinations of tips, holders, diffusers, nozzles and liners.
Yes, when configured with the correct welding wire, liner, contact tip, shielding gas and welding parameters.
They can be configured for aluminum MIG welding, but wire-feed components such as liners and contact tips must be selected appropriately.
No.
BZL Series is an INWELT product range using common MB-style torch formats. References to third-party model names or trademarks are used only to describe compatibility or replacement format where applicable.
Not necessarily.
Current ratings, duty cycles, wire ranges and component configurations may differ between manufacturers.
Use INWELT technical data when selecting an INWELT torch.
Yes.
OEM/ODM, private labeling, cable customization, connector options, consumable kits and packaging customization are available for qualified B2B customers.
For faster model selection and compatibility confirmation, provide:
Welding machine manufacturer and model
Required welding current
CO₂ or mixed-gas application
Welding wire diameter
Wire material
Existing torch model
Connector photo
Required cable length
Gas- or water-cooled requirement
Required consumables
Estimated purchasing quantity
INWELT or private-label branding
INWELT can then recommend the appropriate MB15, MB24, MB25, MB36, MB401D or MB501D configuration for your welding system.