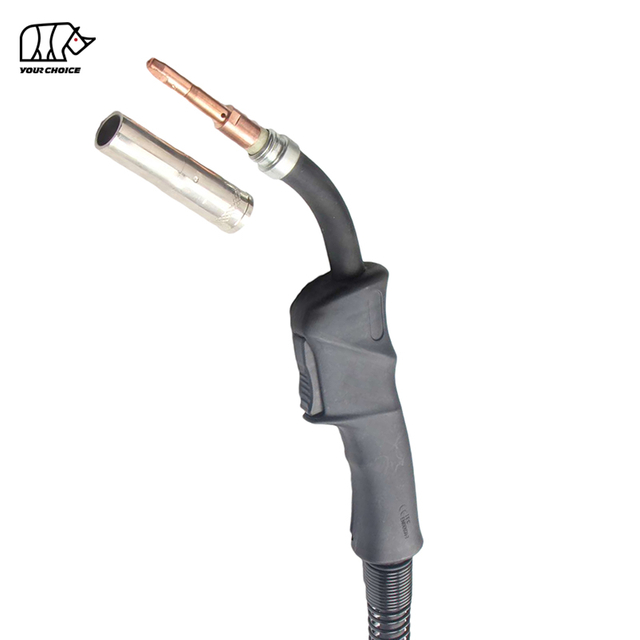
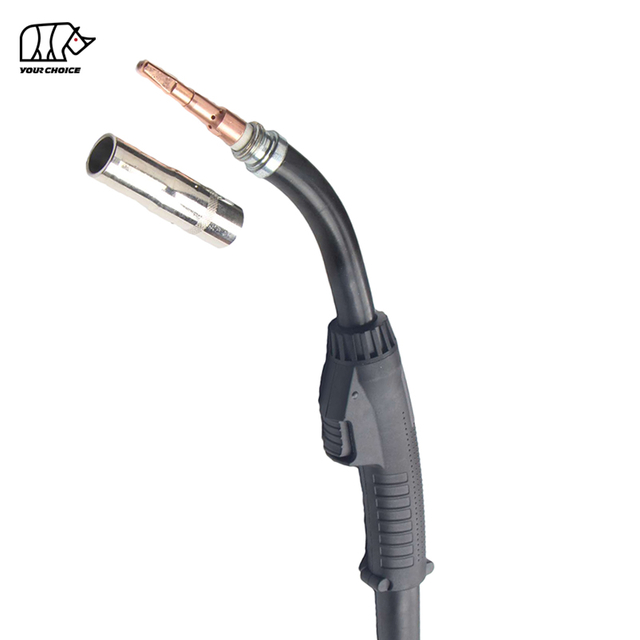
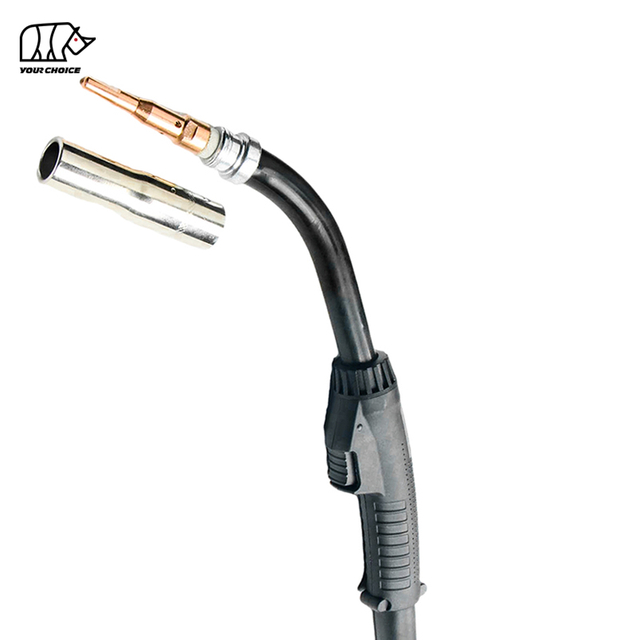
PSF305 ESAB-Style MIG Welding Torch Overview
The INWELT PSF305 ESAB-Style MIG Welding Torch is a gas-cooled MIG/MAG welding gun designed for manual industrial welding applications. It is rated at 290A with CO₂ shielding gas and 260A with mixed shielding gas at a 60% duty cycle.
The PSF305 supports Ø0.8–1.2 mm welding wire and is available with 3 m, 4 m and 5 m cable assemblies. Its Euro central connection, swan neck configuration and replaceable front-end components make it an option for welding equipment distributors, fabrication workshops and industrial maintenance operations.
As part of the INWELT PSF Series, the PSF305 offers a higher listed current rating than the PSF250 while retaining a gas-cooled handheld welding gun configuration.
INWELT supplies complete PSF305 MIG welding torches, matching consumables and replacement components for wholesale, OEM/ODM and international B2B purchasing projects.
PSF305 MIG Welding Torch Technical Specifications
The following specifications describe the current INWELT PSF305 product configuration.
| Specification | INWELT PSF305 |
| Brand | INWELT |
| Model | PSF305 |
| Product Type | ESAB-Style MIG Welding Torch |
| Welding Process | MIG / MAG (GMAW) |
| Cooling Method | Gas Cooled / Air Cooled |
| Rated Current with CO₂ | 290A |
| Rated Current with Mixed Gas | 260A |
| Duty Cycle | 60% |
| Welding Wire Diameter | Ø0.8–1.2 mm |
| Cable Length | 3 m / 4 m / 5 m |
| Connection Type | Euro Central Adapter |
| Torch Design | Swan Neck MIG Welding Gun |
| Standard Contact Tip | Ø1.0 mm, M8 × 37 |
| Standard Consumables | Gas Nozzle, Contact Tip, Gas Diffuser |
| Supply | Wholesale / OEM / ODM |
The rated welding current must be considered together with the shielding gas and duty cycle. The PSF305 model designation should not be used as a substitute for the actual rated-current specification.
For replacement orders, confirm the complete torch configuration, connector dimensions and consumable requirements before purchasing.
Key Features of the INWELT PSF305 MIG Gun
290A CO₂ and 260A Mixed-Gas Ratings
The standard INWELT PSF305 is listed with the following ratings:
The specified ratings help buyers evaluate the welding gun according to their welding process and operating requirements.
The intended welding current should be selected according to the welding wire, shielding gas, welding procedure and expected arc-on time.
Gas-Cooled Swan Neck Design
The PSF305 uses a gas-cooled swan neck welding gun configuration.
The torch does not require a separate circulating water-cooling circuit.
Its curved front-end design allows the operator to position the contact tip and gas nozzle at the required working angle during manual MIG/MAG welding.
The correct welding current and operating duty cycle must be observed to prevent excessive torch heating.
Euro Central Connector
The PSF305 is supplied in a Euro central connector configuration according to the standard INWELT product listing.
The connector forms the interface between the welding torch and a compatible wire feeder.
It combines the required mechanical attachment and connections for welding current, wire feeding, shielding gas and trigger control.
Actual compatibility depends on the corresponding machine connection and pin configuration.
3 m, 4 m and 5 m Cable Assemblies
INWELT supplies PSF305 welding guns in three standard cable lengths:
The appropriate cable length depends on the welding workstation, workpiece size and distance between the operator and wire feeder.
A shorter cable may simplify cable routing in compact welding areas. A longer cable offers greater reach but requires appropriate installation to reduce unnecessary bending and feeding resistance.
Replaceable Front-End Components
The PSF305 includes replaceable components for welding current transfer, gas distribution and wire feeding.
These components include the contact tip, gas nozzle, gas diffuser, torch head and wire liner.
Using the correct replacement parts helps maintain the intended front-end configuration and simplifies maintenance.
Understanding the PSF305 Duty Cycle
The INWELT PSF305 is specified at a 60% duty cycle.
Duty cycle describes the percentage of a standard ten-minute operating period during which a welding torch can operate at the specified rated current under the relevant test conditions.
At a 60% duty cycle, the welding gun can operate for six minutes during a ten-minute period at the applicable rated load.
PSF305 with CO₂ Shielding Gas
Rated current: 290A
Duty cycle: 60%
Cooling: Gas Cooled
PSF305 with Mixed Shielding Gas
Rated current: 260A
Duty cycle: 60%
Cooling: Gas Cooled
The current rating is not identical for every shielding-gas mixture.
Actual operating conditions, including ambient temperature, electrical connections, cable condition and welding duration, should also be considered.
What Happens If the PSF305 Duty Cycle Is Exceeded?
Operating beyond the specified duty cycle may cause excessive heating of the welding gun and its components.
Possible symptoms include:
Excessive torch neck temperature
Increased contact-tip wear
Hot cable or electrical connections
Damage to front-end components
Unstable welding performance
If overheating occurs, stop welding and allow the equipment to cool before inspection.
PSF305 Complete Torch Models and Ordering Codes
INWELT lists three standard PSF305 complete torch codes according to cable length.
| Complete Torch Code | Product Description | Cable Length |
| ICT1673 | PSF305 MIG Welding Torch, Euro Type | 3 m |
| ICT1674 | PSF305 MIG Welding Torch, Euro Type | 4 m |
| ICT1675 | PSF305 MIG Welding Torch, Euro Type | 5 m |
The standard product listing describes these configurations as Euro-type torch assemblies with a spring-pin connection.
For repeat orders, customers should provide the complete torch code and confirm the corresponding connector and cable assembly.
PSF305 3 m MIG Welding Torch
The 3 m version is suitable for welding workstations where the wire feeder is positioned relatively close to the welding area.
PSF305 4 m MIG Welding Torch
The 4 m version provides additional working reach for general fabrication and industrial workshop applications.
PSF305 5 m MIG Welding Torch
The 5 m version is intended for workstations requiring additional distance between the operator and the wire feeder.
All cable lengths should be selected with consideration for wire-feeding conditions and cable routing.
PSF305 MIG Torch Consumables and Spare Parts
The PSF305 uses a serviceable consumable and replacement-part system.
INWELT provides a component list for identifying the front-end consumables, torch head, handle, cable assembly and Euro central connection.
PSF305 Replacement Parts Reference Table
| Position | Component | Standard Description |
| 1 | Gas Nozzle | Threaded nozzle, listed as PSF315 type, reference 366-854-882 |
| 2 | Contact Tip | Ø1.0 mm, M8 × 37 |
| 3 | Gas Diffuser | M8, PSF305/315/400/405 style |
| 4 | Torch Head | PSF305 |
| 5 | Trigger Button | PSF305/405 style |
| 6 | Switch Base | ESAB-style configuration |
| 7 | Torch Handle | Black handle, PSF305/405 style |
| 8 | Cable Joint | Joint with Spring |
| 9 | Coaxial Cable | 3 m standard assembly |
| 10 | Cable Support | Protective Spring |
| 11 | Rear Connection Component | Back Box Hole |
| 12 | Gun Plug Nut | Rear Connector Component |
| 13 | Euro Central Adapter | Euro Central Gas Connector Body |
| 14 | Wire Liner | Insulated Steel Liner, listed as Ø1.4 mm × 3.5 m |
| 15 | Tool | MIG Spanner |
The component descriptions reflect the current INWELT PSF305 parts list. Similar model names do not automatically establish component interchangeability.
For replacement orders, confirm the dimensions and corresponding part references of the actual torch assembly.
Threaded Gas Nozzle and M8 Contact Tip
The gas nozzle directs shielding gas toward the welding area and surrounds the contact tip and welding arc.
The current INWELT parts list identifies a threaded nozzle under the PSF315-style designation, reference 366-854-882.
The standard listed contact tip is:
For Ø0.8 mm or Ø1.2 mm wire applications, select a contact tip with the corresponding wire-size specification.
Gas Diffuser and Torch Head
The gas diffuser distributes shielding gas through the front-end assembly.
The PSF305 product listing identifies an M8 gas diffuser associated with PSF305/315/400/405-style consumable configurations.
The torch head supports the contact tip, gas diffuser and nozzle assembly.
Before replacing either part, verify the exact dimensions, installation interface and product reference.
Wire Liner and Cable Assembly
The wire liner guides welding wire from the feeder through the torch cable toward the contact tip.
The standard parts list identifies an insulated steel liner with a listed Ø1.4 mm designation and 3.5 m length.
The liner specification must be confirmed against the actual welding wire diameter, liner construction and torch cable length.
A liner intended for one cable configuration should not automatically be assumed suitable for every 3 m, 4 m or 5 m torch assembly.
Handle, Trigger and Connector Parts
The PSF305 includes replaceable handle and trigger components.
The rear assembly includes the Euro central adapter, gun plug nut and supporting parts.
For maintenance or replacement, verify the component arrangement and electrical connection before installing new parts.
PSF305 ESAB-Style MIG Torch Compatibility
The INWELT PSF305 is an ESAB-style MIG welding torch intended for use with an appropriately configured MIG/MAG welding machine and wire feeder.
However, ESAB-style does not guarantee universal compatibility with every ESAB welding machine or every machine from another manufacturer.
The complete connection system must be checked before purchasing.
PSF305 Compatibility Checklist
| Item | What to Verify |
| Existing Torch | Model and Configuration |
| Welding Machine | Manufacturer and Model |
| Wire Feeder | Connection Interface |
| Euro Connector | Mechanical and Electrical Compatibility |
| Trigger Wiring | Control-Pin Arrangement |
| Shielding Gas | Gas Connection and Supply |
| Cable Length | 3 m / 4 m / 5 m |
| Welding Wire | Ø0.8–1.2 mm |
| Contact Tip | Wire Size and M8 × 37 Configuration |
| Gas Nozzle | Threaded Attachment and Dimensions |
| Gas Diffuser | M8 Front-End Configuration |
| Wire Liner | Wire Size, Type and Length |
Can a PSF305 Replace an ESAB MIG Welding Torch?
The INWELT PSF305 can be evaluated for replacement applications involving a corresponding ESAB-style torch configuration.
Compatibility must be verified through the connector, cable assembly, trigger wiring, torch head and front-end consumables.
For replacement orders, customers should provide the original torch model, connector photographs, existing part numbers or a reference sample.

| Position | Description |
| 1 | Gas nozzle threaded PSF315(366-854-882) |
| 2 | Contact tip/Φ1.0mm//M8×37/ESAB |
| 3 | Gas diffuser M8/PSF305/315/400/405/ESAB |
| 4 | Torch head PSF305/ESAB |
| 5 | Switch button/PSF305/405/ESAB |
| 6 | Switch base/ESAB |
| 7 | Torch handle/black/PSF305/405/ESAB |
| 8 | Joint with spring |
| 9 | Coaxial cable 3M/ESAB |
| 10 | Spring/cable support/black |
| 11 | Back box hole |
| 12 | Gun plug nut |
| 13 | Euro central adapter body/gas/ESAB |
| 14 | Insulated steel liner Φ1.4mm 3.5M black/ESAB |
| 15 | Spanner for MIG |
| Complete Torch |
|
| ICT1673 | Mig torch ESAB PSF305/ 3m /with spring pin/euro type |
| ICT1674 | Mig torch ESAB PSF305/ 4m /with spring pin/euro type |
| ICT1675 | Mig torch ESAB PSF305/ 5m /with spring pin/euro type |
Our Catalog:
 INWELT MIG WELDING TORCH.pdf
How to Choose the Correct PSF305 MIG Torch
Selecting the correct PSF305 welding gun requires checking the welding process, current rating and equipment connection.
Step 1: Confirm the Welding Current
The standard INWELT PSF305 is listed at 290A CO₂ and 260A mixed gas with a 60% duty cycle.
The required welding parameters should remain within the applicable operating limits.
Step 2: Confirm the Shielding Gas
Identify whether the welding process uses CO₂ or mixed shielding gas.
The allowable current differs according to the specified gas and thermal conditions.
Step 3: Check the Welding Wire Diameter
The PSF305 supports Ø0.8–1.2 mm welding wire.
Select the corresponding contact tip and liner for the actual wire diameter and type.
Step 4: Select the Cable Length
Choose a 3 m, 4 m or 5 m cable according to the required working reach.
Step 5: Verify the Euro Connection
Confirm the power, gas, trigger and mechanical connections between the welding gun and wire feeder.
Step 6: Identify the Required Consumables
Verify the contact tip, gas nozzle, diffuser, torch head and liner specifications.
For distributor orders, identify the required consumable references before placing a bulk order.
PSF250 vs. PSF305 vs. PSF405 MIG Welding Torches
The PSF250, PSF305 and PSF405 are gas-cooled MIG welding torch models in the INWELT PSF Series.
They differ in current rating and supported welding wire diameter.
| Specification | PSF250 | PSF305 | PSF405 |
| Cooling | Gas Cooled | Gas Cooled | Gas Cooled |
| CO₂ Current | 230A | 290A | 350A |
| Mixed-Gas Current | 200A | 260A | 320A |
| Duty Cycle | 60% | 60% | 60% |
| Wire Diameter | Ø0.8–1.2 mm | Ø0.8–1.2 mm | Ø0.8–1.6 mm |
| Cable Options | 3 / 4 / 5 m | 3 / 4 / 5 m | 3 / 4 / 5 m |
These values describe the standard configurations currently listed by INWELT. Ratings should be verified against the relevant product specification before final procurement.
When Should You Choose PSF250?
Consider the PSF250 for applications requiring a lower welding-current range while using Ø0.8–1.2 mm welding wire.
When Should You Choose PSF305?
Choose the PSF305 when the welding application requires more current capacity than the PSF250 while retaining an air-cooled torch and Ø0.8–1.2 mm wire range.
When Should You Choose PSF405?
Consider the PSF405 when the application requires a higher current rating or welding wire up to Ø1.6 mm.
Model selection should always consider actual welding current, duty cycle, shielding gas, connector type and consumable requirements.
Industrial Applications of the PSF305 MIG Gun
The PSF305 is intended for compatible industrial manual MIG/MAG welding applications.
General Metal Fabrication
The PSF305 can be used for welding fabricated steel components, frames and assemblies where the selected welding current and wire diameter fall within its operating limits.
Machinery Manufacturing
Manufacturing workshops may use the PSF305 for suitable MIG welding of machinery frames, brackets and fabricated parts.
Structural Component Fabrication
The torch can be considered for structural component welding when the qualified welding procedure and thermal requirements are compatible with its specifications.
Equipment Repair and Maintenance
The PSF305 can be used in maintenance and repair applications with compatible MIG/MAG equipment and the correct connector arrangement.
Industrial Production Workshops
The 3 m, 4 m and 5 m cable options allow buyers to select a suitable working reach for different industrial workstations.
Actual suitability depends on welding procedure requirements, operator conditions and duty-cycle limitations.
Common PSF305 MIG Torch Problems and Solutions
Regular inspection and correct consumable selection can help reduce avoidable welding interruptions.
| Problem | Possible Cause | Recommended Check |
| Torch Overheating | Excessive current, duty cycle or poor connection | Verify operating rating and electrical connections |
| Irregular Wire Feeding | Worn liner, incorrect contact tip or excessive cable bends | Inspect liner, tip and cable routing |
| Contact Tip Burnback | Wire feeding or welding parameter issues | Check tip size and welding settings |
| Excessive Spatter | Incorrect welding parameters or shielding conditions | Inspect settings, gas flow and consumables |
| Poor Shielding Gas Coverage | Nozzle blockage or gas leakage | Inspect nozzle, diffuser and gas connections |
| Unstable Welding Arc | Poor current transfer or feeding irregularities | Check contact tip, liner and connections |
| Trigger Failure | Switch or control connection problem | Inspect trigger assembly and connector |
| Cable Damage | Abrasion, excessive bending or mechanical stress | Inspect and replace damaged parts |
Why Does a PSF305 MIG Torch Overheat?
The torch may overheat if the welding current or duty cycle exceeds the specified operating conditions.
Damaged cables, loose electrical connections and worn front-end components can also contribute to heating.
Stop welding and allow the equipment to cool before inspection.
Why Does the PSF305 Have Wire Feeding Problems?
Wire feeding problems may be caused by a worn liner, incorrect contact-tip size, cable bends or feeder-related issues.
Check the complete wire-feeding path rather than replacing the contact tip alone.
Why Is Shielding Gas Coverage Poor?
A blocked or damaged gas nozzle, loose gas connection or diffuser problem may affect shielding-gas delivery.
Inspect the gas system and front-end components to identify the cause.
PSF305 MIG Torch Maintenance
Regular maintenance helps keep the PSF305 welding gun in appropriate working condition.
Inspect the Gas Nozzle
Remove excessive spatter and check the nozzle for deformation or damage.
Check the Contact Tip
Inspect the contact-tip bore for wear or damage.
Replace the tip when its condition affects wire feeding or welding-current transfer.
Inspect the Gas Diffuser
Check the diffuser for damage, contamination or incorrect installation.
Check the Wire Liner
Inspect the liner if wire-feeding resistance increases or feeding becomes inconsistent.
Use a liner suitable for the wire diameter and cable assembly.
Inspect the Cable and Connector
Check the cable jacket, rear connector and electrical connections for wear or damage.
Inspect the Handle and Trigger
Verify that the trigger operates correctly and inspect the handle assembly for visible damage.
Disconnect the welding equipment and allow the torch to cool before maintenance or replacement of components.
PSF305 MIG Welding Guns for Distributors and OEM Buyers
INWELT supplies PSF305 MIG welding torches and replacement components for international B2B customers.
Typical buyers include:
Welding equipment distributors
Industrial welding suppliers
Importers and wholesalers
Welding equipment manufacturers
OEM and private-label brands
Industrial fabrication companies
Maintenance and repair suppliers
Wholesale PSF305 MIG Torch Supply
INWELT offers standard PSF305 torch assemblies in 3 m, 4 m and 5 m configurations.
For bulk orders, buyers should specify:
OEM and Private-Label PSF305 MIG Torches
INWELT supports OEM/ODM inquiries based on the customer's technical and commercial requirements.
Customization discussions may include:
Nonstandard requests should be supported by a drawing, specification or reference sample for technical review.
Replacement Consumables for Distributor Inventory
For long-term distributor purchasing, replacement components can be identified according to the corresponding PSF305 torch configuration.
Consistent product codes and technical specifications help purchasing teams organize repeat orders and consumable inventory.
Frequently Asked Questions About PSF305 MIG Torches
What is a PSF305 MIG welding torch?
The INWELT PSF305 is an ESAB-style gas-cooled MIG/MAG welding torch designed for industrial manual welding. Its listed rating is 290A CO₂ and 260A mixed gas at a 60% duty cycle.
Is the INWELT PSF305 a 305A or 315A welding gun?
PSF305 is the product model designation. The current INWELT technical specification lists 290A with CO₂ and 260A with mixed shielding gas at a 60% duty cycle.
What is the duty cycle of the PSF305?
The standard INWELT PSF305 is specified at a 60% duty cycle at its stated welding-current ratings.
Is the PSF305 air-cooled or water-cooled?
The INWELT PSF305 is a gas-cooled, also called air-cooled, MIG welding gun. It does not require a separate water-cooling circuit.
What welding wire sizes does the PSF305 support?
The PSF305 supports Ø0.8–1.2 mm welding wire. Contact tips and liners must be selected to match the wire diameter and material.
What cable lengths are available for the PSF305?
INWELT lists 3 m, 4 m and 5 m complete torch assemblies.
What are the complete PSF305 torch codes?
The listed codes are ICT1673 for 3 m, ICT1674 for 4 m and ICT1675 for 5 m Euro-type configurations.
Does the PSF305 use an M8 contact tip?
The current INWELT parts list includes a Ø1.0 mm contact tip with M8 × 37 dimensions. Other wire sizes require corresponding compatible contact tips.
What gas nozzle does the PSF305 use?
The current INWELT parts list identifies a threaded gas nozzle under the PSF315-style designation, with reference 366-854-882. The required dimensions should be confirmed for the specific torch assembly.
Does the PSF305 use a Euro connector?
Yes. The standard INWELT PSF305 complete torch listing specifies a Euro central connector configuration.
Can an INWELT PSF305 replace an ESAB welding gun?
The PSF305 can be evaluated as an alternative for an appropriately configured ESAB-style MIG welding torch. Connector, trigger, cable and consumable compatibility must be verified.
Are PSF305 and PSF315 consumables interchangeable?
Some components may share design features or specifications, but model names alone do not establish interchangeability. Compare the actual part number, dimensions and front-end attachment before ordering.
What is the difference between PSF250 and PSF305?
The standard INWELT PSF250 is listed at 230A CO₂ and 200A mixed gas, while the PSF305 is listed at 290A CO₂ and 260A mixed gas. Both are specified at a 60% duty cycle.
What is the difference between PSF305 and PSF405?
The PSF405 has a higher listed current rating and supports wire up to Ø1.6 mm, compared with Ø1.2 mm for the PSF305.
Does INWELT supply PSF305 spare parts?
Yes. INWELT lists consumables and replacement components for the PSF305, including gas nozzles, contact tips, gas diffusers, torch heads, handles, triggers and liners.
Can INWELT supply OEM PSF305 MIG welding torches?
Yes. INWELT supports OEM/ODM inquiries involving product configuration, handle color, labeling, packaging and bulk supply.
Can distributors order PSF305 MIG guns in bulk?
Yes. INWELT supplies PSF305 welding torches for wholesale, distributor and industrial purchasing requirements.
Request a PSF305 MIG Welding Torch Quote
Looking for an ESAB-style PSF305 MIG welding torch manufacturer or wholesale supplier?
INWELT supplies PSF305 gas-cooled MIG welding guns and matching replacement components for distributors, importers, OEM brands and industrial buyers.
For an accurate quotation, please provide:
Product Model: PSF305
Cable Length: 3 m / 4 m / 5 m
Welding Machine and Wire Feeder Model
Euro Connector Configuration
Welding Wire Diameter
Required Consumables and Spare Parts
Order Quantity
OEM/ODM or Private-Label Requirements
Destination Market
Contact INWELT for PSF305 MIG Welding Torch Specifications, Bulk Pricing, Replacement Parts and OEM/ODM Inquiries.
 English
 简体中文
 العربية
 Français
 Русский
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 ភាសាខ្មែរ
 Bahasa Melayu
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Čeština
 Монгол
 қазақ
 Српски
 हिन्दी
 فارسی
 Slovenčina
 Slovenščina
 Norsk
 Svenska
 українська
 Ελληνικά
 Suomi
 Latine
 Dansk
 বাংলা
 Hrvatski
 Afrikaans
 Gaeilge
 Eesti keel
 नेपाली
 Oʻzbekcha
 latviešu
 Azərbaycan dili
 Беларуская мова
 Bosanski
 Български
 ქართული
 Lietuvių