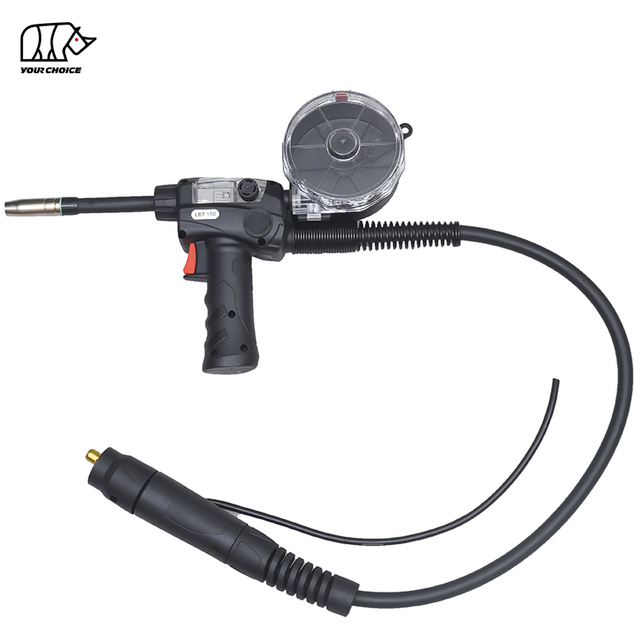
The INWELT LB250 is a gas-cooled MIG spool gun with an integrated wire-spool holder and gun-mounted wire-feeding system. It is rated at 200A with CO₂ and 180A with mixed shielding gas at a 60% duty cycle, supports Ø0.8–1.2 mm welding wire and offers 3 m, 4 m, 6 m and 8 m cable options. Designed for compatible aluminum MIG welding and general fabrication applications, the LB250 is available for wholesale and OEM/ODM supply.
The INWELT LB250 MIG Spool Gun is a gas-cooled welding gun featuring an integrated wire-spool holder and gun-mounted wire-feeding assembly. It is designed for compatible MIG/MAG welding applications, particularly those requiring more controlled feeding of aluminum and other welding wires that can be difficult to feed through a conventional long torch liner.
The LB250 is rated at 200A with CO₂ shielding gas and 180A with mixed shielding gas at a 60% duty cycle. It supports welding wire diameters from Ø0.8 mm to Ø1.2 mm and is available with 3 m, 4 m, 6 m and 8 m cable assemblies.
Unlike a conventional MIG welding torch that receives wire through a long cable liner from a remote wire feeder, a spool gun carries a small wire spool close to the welding gun. Its local feeding mechanism delivers wire through a shorter feed path near the torch head.
This configuration can help reduce wire-feeding resistance and the risk of wire buckling when the equipment is properly set up.
INWELT supplies the LB250 MIG spool gun and matching replacement components for welding equipment distributors, OEM brands, importers and industrial buyers.
LB250 MIG Spool Gun Technical Specifications
The following specifications are based on the standard INWELT LB250 product listing.
Specification
INWELT LB250
Brand
INWELT
Model
LB250 / LBT250
Product Type
MIG/MAG Welding Spool Gun
Welding Process
MIG / MAG (GMAW)
Cooling Method
Gas Cooled / Air Cooled
Rated Current with CO₂
200A
Rated Current with Mixed Gas
180A
Duty Cycle
60%
Welding Wire Diameter
Ø0.8–1.2 mm
Standard Cable Lengths
3 m / 4 m / 6 m / 8 m
Wire Feeding Configuration
Gun-Mounted Spool Feeding
Standard Gas Nozzle
Φ15 mm, 25AK Type
Listed Contact Tip
Ø1.0 mm E-Cu, M6 × 28
Listed Gas Diffuser
M6 × 35 mm, 25AK Type
Torch Head
LBT250
Connector Component
Euro Central Adapter Body
OEM/ODM
Available
Standard Packaging
1 Piece per Box
Important: The published electrical ratings refer to the specified CO₂ and mixed-gas operating conditions. For aluminum MIG welding with argon-based shielding gas, the allowable current and duty cycle should be confirmed for the intended application.
The welding gun model number does not establish an automatic 250A continuous or rated output.
How Does the LB250 MIG Spool Gun Work?
A MIG spool gun places the welding wire supply close to the torch feeding mechanism.
During operation, the gun-mounted feeding assembly draws welding wire from the installed spool and delivers it through the short internal wire path to the contact tip.
The welding current is transferred through the contact tip to the continuously fed electrode wire, while shielding gas is directed toward the weld area through the gas nozzle.
Integrated Wire Spool and Gun-Mounted Feeding
The LB250 features a spool holder mounted on the welding gun body.
The spool is positioned near the feeding mechanism rather than at a distant wire feeder.
This arrangement reduces the length of wire that must be pushed through a liner before reaching the contact tip.
It can be especially useful when feeding relatively soft welding wires, including aluminum wire, provided that the drive roll, contact tip, shielding gas and welding parameters are correctly selected.
Spool Gun vs. Push-Pull MIG Gun
Although both systems can improve welding wire delivery, a spool gun and a push-pull MIG gun use different feeding arrangements.
Feature
MIG Spool Gun
Push-Pull MIG Gun
Wire Supply
Small spool mounted on the gun
Usually supplied from a remote spool
Wire Feeding
Gun-mounted feeding assembly
Coordinated feeder and gun-mounted pull motor
Wire Path
Short local feed path
Wire travels through a longer cable system
Common Application
Aluminum and specialized MIG welding
Aluminum welding where remote wire supply is required
Equipment Requirements
Compatible spool-gun power and control interface
Compatible push-pull feeder and control system
The INWELT LB250 should be identified as a MIG spool gun based on its integrated spool-holder configuration. Push-pull functionality should only be specified when the complete drive system has been technically verified.
Key Features of the INWELT LB250
200A CO₂ and 180A Mixed-Gas Ratings
The LB250 has the following published ratings:
200A with CO₂ shielding gas
180A with mixed shielding gas
60% duty cycle
Duty cycle describes the permitted arc-on time at the rated current under specified test conditions.
At a 60% duty cycle, the standard reference is six minutes of welding during a ten-minute operating period at the applicable rated load.
The correct operating current must be selected according to the shielding gas, welding procedure and thermal requirements.
Ø0.8–1.2 mm Welding Wire Range
The LB250 supports Ø0.8–1.2 mm welding wire.
This stated range describes the torch's supported wire diameters. The drive roll, contact tip and other feeding components must be configured for the specific wire material and diameter.
For aluminum welding, confirm the correct feeding components for the selected aluminum wire.
For steel or stainless steel welding, verify the drive system and shielding-gas requirements before use.
3 m, 4 m, 6 m and 8 m Cable Options
The LB250 is available with four cable lengths:
3 m
4 m
6 m
8 m
Cable length should be selected according to the workstation layout, reach requirements and compatible welding equipment.
Because the spool gun carries its wire supply near the torch, its wire-feeding arrangement differs from that of a conventional MIG torch supplied from a remote feeder.
However, longer cable assemblies still require correct electrical connections, trigger wiring and cable management.
Integrated Spool Holder
The LB250 includes a gun-mounted spool assembly, allowing welding wire to be supplied directly from the spool installed on the gun.
The correct spool dimensions, mounting arrangement and permissible spool weight should be confirmed before ordering replacement wire spools.
Replaceable Front-End Components
The LB250 uses replaceable front-end MIG welding consumables, including a gas nozzle, contact tip and gas diffuser.
The standard parts list identifies a 25AK-type front-end configuration.
For maintenance and repeat purchasing, replacement parts should be selected by verified size, thread and product reference.
LB250 Spool Gun for Aluminum Welding
The LB250 is intended for applications that include compatible aluminum MIG welding.
Aluminum welding wire is generally softer and more susceptible to feeding problems than conventional solid steel welding wire.
A spool gun reduces the distance between the wire spool and the welding gun's feeding mechanism, making it a useful configuration for some aluminum MIG welding applications.
Why Use a Spool Gun for Aluminum?
A spool gun can help address several common wire-feeding challenges:
Wire buckling inside a long liner
Excessive feed resistance
Inconsistent wire delivery
Wire deformation caused by unsuitable drive-roll pressure
Feeding difficulties associated with soft aluminum wire
The result still depends on the complete welding system, correct wire selection and appropriate setup.
Choosing Aluminum Welding Wire
Common aluminum MIG filler wire families include ER4043 and ER5356.
The appropriate filler metal should be selected according to the base material, required mechanical properties and qualified welding procedure.
Before using a particular aluminum wire with the LB250, verify:
Wire diameter
Drive-roll groove and size
Contact-tip specification
Spool dimensions
Feed mechanism compatibility
Shielding gas
Welding power source settings
Shielding Gas for Aluminum MIG Welding
Aluminum MIG welding commonly uses argon-based shielding gas, with the specific gas selected according to the welding procedure.
CO₂ shielding gas should not be treated as the standard shielding gas for aluminum MIG welding.
The LB250's published CO₂ and mixed-gas current ratings must not be interpreted as a separately verified current rating for every argon-based aluminum welding procedure.
Confirm the permitted operating conditions for the selected shielding gas and application.
LB250 Wire Spool, Drive Roll and Liner Selection
Correct wire-feeding configuration is essential to spool gun performance.
Wire Spool Compatibility
Before purchasing welding wire for the LB250, confirm the spool diameter, hub dimensions and mounting requirements.
Spool size and capacity should be verified against the actual LB250 reel assembly.
Do not assume that any small MIG welding wire spool will fit the gun.
Drive Roll Selection
The drive roll must match the welding wire diameter and material.
For soft aluminum wire, an appropriate groove design and feed pressure help reduce wire deformation.
For other welding wires, a different drive-roll configuration may be required.
Excessive drive pressure can deform soft wire, while insufficient pressure may cause slippage.
Contact Tip Selection
The contact tip must correspond to the welding wire diameter and front-end configuration.
The LB250 standard parts list includes an Ø1.0 mm E-Cu contact tip with M6 × 28 dimensions.
For Ø0.8 mm or Ø1.2 mm wire, confirm the corresponding contact-tip size and bore specification.
Liner Selection
The LB250 spare parts list includes a short liner identified as 4.0 × 2.0 × 200 mm.
Replacement liner dimensions and material should match the corresponding feeding arrangement.
The correct liner should be selected based on the actual torch assembly rather than the cable length alone.
Specification
Position
Code
Ref.
Description
1
IJDT0089
Gas nozzleΦ15mm 25AK
2
IJDV0015-10
Contact tip/Φ1.0mm E-CU/M6*28
3
IJDG0072
GAS DIFFUSER M6/35MM/25AK
4
IJDA0693
TORCH HEAD/LBT250
5
IJIK0526
Switch cap/PC
6
IJIK0190
Wire drawing gun reel assembly/2018
7
IJIR0081
Trigger red
8
IJDW0611
Mig grip handle/100/150/PA66+30%GF
9
IJIK0788
Joint for MIG grip handle
10
IJGU0881
Spring/cable support 401D-501D/black
11
IJD00541
Cable cable/diameter 5mm/4 wires/3m
12
IJGU0971
Spring support/MIG water cooling/black
13
IJIK0951
Back box hole for gas and water cooling torch/black
INWELT provides complete LB250 welding gun assemblies in several standard lengths.
Complete Torch Code
Model
Cable Length
IJDM0224
LBT250 / LB250
3 m
IJDM0225
LBT250 / LB250
4 m
IJDM0227
LBT250 / LB250
6 m
IJDM0229
LBT250 / LB250
8 m
The listed configurations are described as integrated four-wire control assemblies.
For OEM or replacement orders, confirm the cable assembly, electrical connector and control-wire configuration before production.
Choosing the Right Cable Length
3 m LB250 Spool Gun
An option for compact workstations where the welding machine is positioned close to the welding area.
4 m LB250 Spool Gun
Provides additional reach for fabrication benches and general workshop applications.
6 m LB250 Spool Gun
Can be considered where the welding operator requires greater movement around larger workpieces.
8 m LB250 Spool Gun
Provides extended working reach, subject to suitable welding equipment, electrical connections and cable management.
LB250 MIG Spool Gun Consumables and Replacement Parts
INWELT provides a component reference list for the LB250 spool gun assembly.
LB250 Spare Parts Reference Table
Component
INWELT Code
Specification
Gas Nozzle
IJDT0089
Φ15 mm, 25AK Type
Contact Tip
IJDV0015-10
Ø1.0 mm E-Cu, M6 × 28
Gas Diffuser
IJDG0072
M6 × 35 mm, 25AK Type
Torch Head
IJDA0693
LBT250
Switch Cap
IJIK0526
PC
Wire Spool Assembly
IJIK0190
Wire Drawing Gun Reel Assembly
Trigger
IJIR0081
Red Trigger
MIG Handle
IJDW0611
PA66 + 30% GF
Handle Joint
IJIK0788
MIG Grip Handle Joint
Cable Support Spring
IJGU0881
Cable Support Component
Cable Assembly
IJD00541
Listed 3 m Four-Wire Component
Rear Support Component
IJGU0971
Spring Support
Rear Housing Component
IJIK0951
Back-Box Component
Control Wire
IJIR0378
4 × 0.5 mm²
Euro Adapter Body
IJUC0060-02
Without Spring Pins
Short Liner
IJJD0646
4.0 × 2.0 × 200 mm
MIG Spanner
IJDH6011
Service Tool
The original component descriptions may include shared parts used across several torch families. These references do not imply that the LB250 is water-cooled or universally compatible with other torch models.
25AK Gas Nozzle and Contact Tip
The LB250 includes a standard Φ15 mm 25AK-type gas nozzle.
The contact tip is specified as an Ø1.0 mm E-Cu part with an M6 × 28 configuration.
These components work together to direct shielding gas and transfer welding current to the wire.
For bulk replacement orders, confirm the dimensions and component references.
Spool Assembly, Trigger and Torch Head
The gun-mounted spool assembly supports the welding wire supply.
The trigger provides the operator control input for the connected welding system.
The torch head supports the front-end welding components.
These parts should be matched to the specified LB250 assembly when ordering replacements.
Cable, Connector and Control Wires
The LB250 includes a control-wire system associated with the gun-mounted wire feeder.
The current parts list includes a four-core control cable and a Euro central adapter body.
However, the actual power-source compatibility depends on the complete connector, control wiring and spool-gun motor requirements.
LB250 MIG Spool Gun Compatibility Guide
The LB250 should only be connected to a welding power source and control system suitable for the selected spool-gun assembly.
An ordinary MIG welding machine with a Euro connector is not necessarily spool-gun compatible.
What Should Buyers Verify?
Component
Required Check
Welding Power Source
Manufacturer and model
Spool Gun Control
Supported motor and control requirements
Power Connection
Electrical and mechanical interface
Trigger Control
Control-wire arrangement
Wire Feed Control
Speed control and feeder compatibility
Shielding Gas
Gas connection and supply arrangement
Cable Length
3 / 4 / 6 / 8 m
Wire Spool
Size and hub compatibility
Drive Roll
Diameter and material compatibility
Contact Tip
Thread, bore and wire size
Is the LB250 Compatible with Every Euro-Connector MIG Welder?
No.
The appearance of a Euro connector is not sufficient evidence of complete spool-gun compatibility.
The power source must support the required electrical, mechanical and wire-feeder control functions.
For replacement or OEM projects, buyers should provide the welding machine model, connector drawings and control requirements.
How to Set Up an LB250 MIG Spool Gun
The following general procedure should be used together with the instructions for the particular welding machine and LB250 configuration.
Step 1: Confirm Equipment Compatibility
Verify the welding power source, connector and spool-gun control requirements.
Do not connect unverified control wiring to the welding equipment.
Step 2: Disconnect the Welding Equipment
Turn off and isolate the power source before installing or changing the spool gun and its components.
Step 3: Install the Correct Welding Wire Spool
Use a spool with verified dimensions and a suitable welding wire type.
Follow the manufacturer's spool mounting instructions.
Step 4: Check the Drive Roll
Confirm that the drive-roll groove and size match the welding wire.
Set the drive-roll pressure according to the applicable equipment instructions.
Step 5: Install the Correct Contact Tip
Select the contact tip according to wire diameter and front-end specifications.
Step 6: Connect the Welding Gun
Connect the power, gas and control interfaces according to the verified equipment configuration.
Step 7: Set the Shielding Gas and Welding Parameters
Select shielding gas and welding parameters suitable for the wire and material.
For aluminum welding, use a qualified argon-based gas configuration as required by the procedure.
Step 8: Verify Wire Feeding
Perform the equipment manufacturer's wire-feed check and verify that the wire moves smoothly.
After confirming safe operation, make a test weld and adjust the welding parameters according to the application.
LB150 vs. LB250 MIG Spool Gun
INWELT supplies both LB150 and LB250 models in its Spool Gun series.
Specification
LB150
LB250
Product Type
MIG Spool Gun
MIG Spool Gun
Cooling
Gas Cooled
Gas Cooled
CO₂ Current Rating
150A
200A
Mixed-Gas Current Rating
130A
180A
Duty Cycle
60%
60%
Wire Diameter
Ø0.8–1.0 mm
Ø0.8–1.2 mm
Cable Length
3 / 4 / 6 / 8 m
3 / 4 / 6 / 8 m
Wire Feeding
Integrated Spool System
Integrated Spool System
When Should You Choose LB150?
Consider LB150 where the required welding current and wire diameter fall within the LB150 operating range.
When Should You Choose LB250?
Consider LB250 where a higher published current rating or a wire diameter up to Ø1.2 mm is required.
The selection should also account for shielding gas, welding process, spool dimensions and equipment compatibility.
Industrial Applications of the LB250 Spool Gun
The LB250 can be considered for compatible MIG welding applications where a gun-mounted wire-feeding system is beneficial.
Aluminum Fabrication
The LB250 can be used for suitable aluminum fabrication operations when the required wire, shielding gas and welding parameters are correctly selected.
Automotive Aluminum Repair
A spool gun can be useful in automotive repair applications involving suitable aluminum components.
Welding procedures and material specifications must be followed, especially for safety-critical components.
Marine Aluminum Fabrication
For compatible aluminum fabrication and repair operations in marine environments, the LB250 can be evaluated according to the welding procedure and equipment requirements.
General Metal Fabrication
The LB250 can be used with suitable welding wires for general metal fabrication, subject to the correct feeding and welding configuration.
Industrial Maintenance
The spool-gun configuration can be considered for maintenance and repair operations where wire feeding and workpiece accessibility are important.
Common LB250 Spool Gun Problems and Solutions
Problem
Possible Cause
Recommended Check
Wire birdnesting
Incorrect drive-roll pressure or wire-feed blockage
Inspect drive roll, wire path and contact tip
Wire slipping
Insufficient roll pressure or unsuitable groove
Check drive-roll setup
Wire deformation
Excessive feed pressure
Adjust according to wire and equipment requirements
Irregular feeding
Damaged tip, spool drag or control issue
Inspect spool, tip and feeding assembly
Excessive spatter
Incorrect welding parameters or shielding conditions
Check wire, gas and welding settings
Burnback
Incorrect tip, wire speed or arc settings
Inspect tip and process parameters
Poor gas coverage
Nozzle blockage or gas leakage
Inspect gas nozzle, diffuser and gas connections
Spool gun not feeding
Control connection or motor supply problem
Verify electrical compatibility and control wiring
Torch overheating
Duty cycle or rated current exceeded
Check current, shielding gas and operating time
Why Does an LB250 Spool Gun Jam Welding Wire?
Wire jams may result from unsuitable drive-roll tension, spool drag, a damaged contact tip or misalignment in the wire path.
For aluminum wire, the feeding components must be suitable for the selected soft wire.
Why Does the LB250 Spool Gun Feed Wire Irregularly?
Irregular feeding may be caused by drive-roll slippage, excessive spool resistance, an incorrect contact tip or an electrical control problem.
Check the mechanical feeding components before replacing the complete welding gun.
Why Does the LB250 Spool Gun Overheat?
Excessive heating can occur when the welding current or operating duty cycle exceeds the specified conditions.
Poor electrical connections or damaged cable components may also contribute to overheating.
Stop welding and allow the equipment to cool before inspection.
LB250 Spool Gun Maintenance
Regular inspection can help maintain the feeding system and front-end components.
Inspect the Spool Holder
Check for damage, contamination or mechanical interference that could affect spool movement.
Inspect the Drive Roll
Remove accumulated wire debris and inspect the groove for wear or damage.
Check the Contact Tip
Replace the contact tip if wear or damage affects wire feeding or current transfer.
Clean the Gas Nozzle
Remove spatter buildup and inspect the nozzle for deformation.
Inspect the Cable and Control Wires
Check the cable jacket, electrical connectors and control wiring for damage.
Follow the Correct Maintenance Procedure
Use the maintenance instructions applicable to the specific LB250 assembly.
Do not apply lubricants to the drive system or wire path unless permitted by the manufacturer.
Disconnect the welding equipment before performing maintenance.
OEM and Wholesale LB250 MIG Spool Gun Supply
INWELT supplies LB250 MIG spool guns and related components for international B2B purchasing.
Typical customers include:
Welding equipment distributors
Welding equipment importers
Industrial welding suppliers
OEM welding equipment brands
Wholesale welding product companies
Industrial fabrication businesses
Welding equipment service providers
Standard LB250 Wholesale Supply
Standard purchasing options include:
LB250 complete spool guns
3 m, 4 m, 6 m and 8 m cable lengths
Matching front-end consumables
Replacement torch components
Bulk and wholesale purchasing
Distributor packaging requirements
OEM and Private-Label Spool Guns
INWELT supports OEM/ODM inquiries for spool-gun supply projects.
Technical and commercial requirements may include:
Cable assembly configuration
Connector requirements
Product marking
Private-label packaging
Replacement-parts supply
Order-specific documentation
Packaging quantities
Sample approval before bulk production
For nonstandard configurations, customers should provide relevant drawings, connector specifications or reference samples.
LB250 Spare Parts for Distributors
The availability of model-specific consumables and mechanical components helps distributors organize replacement stock.
Customers can include contact tips, gas nozzles, diffusers and other confirmed LB250 components in their purchasing plans.
Using verified part numbers reduces the risk of incorrect replacement orders.
Frequently Asked Questions About LB250 Spool Guns
What is the INWELT LB250 MIG spool gun?
The LB250 is a gas-cooled MIG welding spool gun with an integrated wire-spool holder and gun-mounted feeding system. It supports Ø0.8–1.2 mm welding wire and is available with 3 m, 4 m, 6 m and 8 m cables.
Is the LB250 a 250A spool gun?
LB250 is the model designation. The current INWELT product specification lists 200A with CO₂ and 180A with mixed shielding gas at a 60% duty cycle. Any other rating must be separately confirmed.
Can the LB250 spool gun weld aluminum?
The LB250 is designed for compatible aluminum MIG welding applications. The correct wire, drive roll, contact tip, shielding gas and power-source configuration must be selected.
What welding wire sizes does the LB250 support?
The published wire diameter range is Ø0.8–1.2 mm.
What shielding gas should I use for aluminum MIG welding?
Aluminum MIG welding commonly uses argon-based shielding gas. The exact gas and operating parameters depend on the welding procedure and base material.
Does the LB250 have a built-in wire spool?
The LB250 includes a gun-mounted wire-spool holder and feeding arrangement. The spool dimensions and capacity should be confirmed before purchasing replacement wire spools.
Is the LB250 a push-pull MIG welding gun?
The LB250 is identified as a spool gun with a wire spool mounted on the welding gun. It should not be described as a conventional remote-spool push-pull system without verification of its complete drive arrangement.
What cable lengths are available for the LB250?
INWELT offers 3 m, 4 m, 6 m and 8 m cable assemblies.
What contact tip does the LB250 use?
The standard parts list includes an Ø1.0 mm E-Cu contact tip with M6 × 28 dimensions, product code IJDV0015-10.
What gas nozzle does the LB250 use?
The standard parts list specifies a Φ15 mm 25AK-type gas nozzle, product code IJDT0089.
Is the LB250 compatible with every MIG welding machine?
No. Compatibility depends on the welding power source, connector, control wiring, spool-gun motor and gas connection requirements.
Can the LB250 weld stainless steel?
The LB250 is listed for stainless steel welding applications. The wire-feeding components, shielding gas and welding parameters must be suitable for the particular wire and material.
What is the difference between LB150 and LB250?
The LB150 is rated at 150A CO₂ and 130A mixed gas at a 60% duty cycle, while the LB250 is rated at 200A CO₂ and 180A mixed gas at the same duty cycle. The LB250 also supports a larger maximum listed wire diameter.
Does INWELT supply LB250 replacement parts?
Yes. INWELT lists replacement components including contact tips, gas nozzles, diffusers, torch heads, triggers, reel assemblies, connectors and liners.
Can INWELT manufacture OEM LB250 spool guns?
INWELT supports OEM/ODM inquiries for LB250 spool guns, including connector requirements, cable configurations, product labeling and packaging.
Can distributors purchase LB250 spool guns in bulk?
Yes. INWELT supplies LB250 spool guns and replacement components for wholesale, OEM and industrial purchasing projects.
Request an LB250 MIG Spool Gun Quote
Looking for an LB250 MIG spool gun manufacturer or wholesale supplier for aluminum welding equipment?
INWELT supplies LB250 welding spool guns, matching replacement components and OEM/ODM options for distributors, importers and industrial buyers.
For an accurate quotation, please provide:
Required model: LB250
Welding power source and wire feeder model
Connector and control-wire requirements
Welding wire material and diameter
Required spool size
Cable length: 3 m / 4 m / 6 m / 8 m
Required consumables or spare parts
Purchase quantity
OEM/ODM requirements
Destination market
Contact INWELT for LB250 MIG Spool Gun Specifications, Bulk Pricing, Replacement Parts and OEM/ODM Supply.
This website uses cookies and similar technologies (“cookies”). Subject to your consent, will use analytical cookies to track which content interests you, and marketing cookies to display interest-based advertising. We use third-party providers for these measures, who may also use the data for their own purposes.
You give your consent by clicking "Accept all" or by applying your individual settings. Your data may then also be processed in third countries outside the EU, such as the US, which do not have a corresponding level of data protection and where, in particular, access by local authorities may not be effectively prevented. You can revoke your consent with immediate effect at any time. If you click on "Reject all", only strictly necessary cookies will be used.
 English
 简体中文
 العربية
 Français
 Русский
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 ភាសាខ្មែរ
 Bahasa Melayu
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Čeština
 Монгол
 қазақ
 Српски
 हिन्दी
 فارسی
 Slovenčina
 Slovenščina
 Norsk
 Svenska
 українська
 Ελληνικά
 Suomi
 Latine
 Dansk
 বাংলা
 Hrvatski
 Afrikaans
 Gaeilge
 Eesti keel
 नेपाली
 Oʻzbekcha
 latviešu
 Azərbaycan dili
 Беларуская мова
 Bosanski
 Български
 ქართული
 Lietuvių