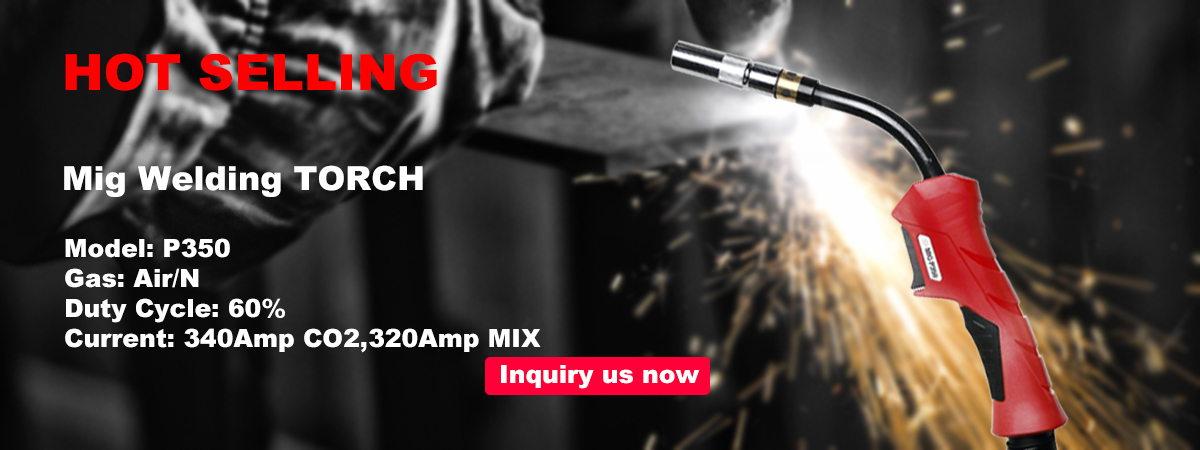
P350 Panasonic-Style MIG Welding Torch Overview
The INWELT P350 Panasonic-Style MIG Welding Torch is a gas-cooled MIG/MAG welding gun designed for manual industrial welding applications. It is rated at 340A with CO₂ shielding gas and 320A with mixed shielding gas at a 60% duty cycle.
The P350 supports Ø0.8–1.6 mm welding wire and is available with 3 m, 4 m and 5 m cable assemblies. Its insulated handle, replaceable torch neck and serviceable consumable system make it an option for fabrication workshops, manufacturing facilities and industrial welding equipment suppliers.
As part of the INWELT PANA Series, the P350 offers a higher current rating than the P180 while retaining a gas-cooled handheld torch configuration.
INWELT supplies P350 MIG welding torches, matching replacement parts and OEM/ODM solutions for distributors, importers, wholesalers and industrial buyers.
P350 MIG Welding Torch Technical Specifications
The following specifications describe the current INWELT P350 product listing.
| Specification | INWELT P350 |
| Brand | INWELT |
| Model | P350 |
| Product Type | Panasonic-Style MIG Welding Torch |
| Welding Process | MIG / MAG (GMAW) |
| Cooling Method | Gas Cooled / Air Cooled |
| CO₂ Rated Current | 340A |
| Mixed-Gas Rated Current | 320A |
| Duty Cycle | 60% |
| Welding Wire Diameter | Ø0.8–1.6 mm |
| Standard Cable Length | 3 m / 4 m / 5 m |
| Listed Connection Type | Euro Central Connector |
| Handle | Insulated Nylon Handle |
| Front-End Consumables | Gas Nozzle, Contact Tip, Ceramic Diffuser, Insulator |
| Torch Head | P350 |
| Application | Manual Industrial MIG/MAG Welding |
| Supply | Wholesale / Bulk / OEM / ODM |
The rated current must be considered together with the shielding gas and duty cycle. The P350 model designation does not mean that the torch is rated at 350A under every operating condition.
For replacement orders, the connection type, complete torch assembly and required consumable configuration should be verified before purchase.
Key Features of the INWELT P350 MIG Gun
340A CO₂ and 320A Mixed-Gas Ratings
The INWELT P350 is rated at:
These ratings make the P350 suitable for industrial MIG/MAG welding applications that fall within the specified thermal and electrical operating conditions.
The welding current should be selected according to the material, welding wire diameter, shielding gas, welding procedure and expected arc-on time.
Gas-Cooled Construction for Industrial Welding
The P350 uses a gas-cooled, commonly called air-cooled, MIG torch design.
It does not require a separate circulating water-cooling system.
This configuration can simplify equipment installation and maintenance where the welding process does not require a water-cooled torch.
However, a gas-cooled design does not permit unlimited welding time at maximum rated current. The specified duty cycle and operating conditions must be respected.
3 m, 4 m and 5 m Cable Assemblies
INWELT offers three standard cable lengths:
Cable length should be selected according to the distance from the wire feeder to the welding workstation, workpiece size and operator movement requirements.
A shorter cable may simplify routing in compact welding areas. A longer cable provides additional reach but requires proper installation to avoid excessive bends and wire-feeding resistance.
Insulated Handle and Replaceable Torch Components
The P350 uses an insulated nylon handle and a replaceable front-end torch assembly.
The handle houses the trigger mechanism and provides a gripping surface for torch positioning.
Replaceable components include the gas nozzle, contact tip, ceramic diffuser, insulator, torch head and liner.
For industrial purchasing and maintenance, replacement parts should be identified by the corresponding P350 specification and part reference.
Understanding the P350 MIG Torch Duty Cycle
The INWELT P350 is specified at a 60% duty cycle.
Duty cycle describes the proportion of a standard ten-minute operating period during which a welding torch can operate at its rated current under specified test conditions.
At a 60% duty cycle, this corresponds to six minutes of welding during a ten-minute period at the applicable rated load.
P350 with CO₂ Shielding Gas
Rated current: 340A
Duty cycle: 60%
Cooling: Gas Cooled
P350 with Mixed Shielding Gas
Rated current: 320A
Duty cycle: 60%
Cooling: Gas Cooled
These ratings should not be interpreted as permission for uninterrupted welding at the specified current.
Actual operating conditions, including ambient temperature, electrical connections, consumable condition and welding duration, may affect torch temperature.
When Is a Higher-Capacity MIG Torch Necessary?
A higher-capacity torch should be considered when the intended welding current or operating duty cycle exceeds the limits of the P350.
Buyers should compare the required welding current, shielding gas, wire diameter, cable configuration and operator requirements before selecting an alternative model.
P350 MIG Torch Cable Lengths and Complete Torch Codes
INWELT lists three complete P350 torch assemblies with different cable lengths.
| Complete Torch Code | Description | Cable Length |
| IJDU6241-36 | MIG P350 Torch PAN | 3 m |
| IJDU6247-36 | MIG P350 Torch PAN | 4 m |
| IJDU6248-36 | MIG P350 Torch PAN | 5 m |
These codes identify the complete torch options in the current INWELT P350 parts list. The final connector and assembly configuration should be confirmed against the quotation.
Which P350 Cable Length Should You Choose?
P350 3 m MIG Welding Torch
A practical option for compact welding stations where the wire feeder is positioned close to the work area.
P350 4 m MIG Welding Torch
Provides additional reach for general fabrication benches, machinery welding and workshop applications.
P350 5 m MIG Welding Torch
Suitable for workstations where additional distance is required between the operator and wire feeder.
Longer cable assemblies should be routed carefully to prevent unnecessary bends or excessive wire-feeding resistance.
For repeat orders, provide the complete torch code and existing connector details.
P350 MIG Torch Consumables and Spare Parts
The P350 uses a serviceable front-end consumable system designed around the corresponding P350 torch head.
INWELT lists replacement components for the nozzle, contact tip, diffuser, insulator, handle, trigger, cable assembly and wire liner.
P350 MIG Torch Spare Parts Reference Table
| Component | INWELT Code | Specification |
| Gas Nozzle | IJDT0407 | P350 Nozzle |
| Contact Tip | IJDV0757-10 | Ø1.0 mm E-Cu, M6 × 45 |
| Ceramic Diffuser | IJDG0987 | P350 Ceramic Diffuser |
| Insulator | IJDT6610 | P350 Insulator |
| Torch Head | IJDA0750 | P350 Torch Head |
| Torch Head Front Part | IJDG0982 | P350 Front Component |
| Handle | IJDW0861-01 | P350 / P500 Handle |
| Trigger Switch | IJGU0871 | MIG/PAN Switch |
| Joint with Spring | IJD00199-01 | Cable Joint Assembly |
| Coaxial Cable | IJGU0832 | 3 m Cable |
| Gas Connector | IJIK0704 | MIG/PAN Gas Connector |
| Wire Liner | IJJD0521 | Green Steel Liner, Ø1.0–1.2 mm, 3 m |
The table reflects the components listed for the standard P350 assembly. Alternative wire sizes, cable lengths and connectors may require different replacement parts.
For wholesale consumable orders, technical drawings, existing references or sample parts should be used to verify the exact configuration.
P350 Gas Nozzle and Contact Tip
The gas nozzle directs shielding gas around the welding arc and helps provide the required gas coverage near the weld pool.
The standard P350 gas nozzle listed by INWELT is:
The contact tip transfers welding current to the moving electrode wire.
The listed contact tip is:
For Ø0.8, Ø1.2 or Ø1.6 mm welding wire, select the corresponding contact tip and verify the required bore and thread configuration.
P350 Ceramic Diffuser and Insulator
The P350 uses a ceramic diffuser and a separate insulating component in its front-end assembly.
The ceramic diffuser helps distribute shielding gas within the torch front end.
The insulator provides electrical separation between designated torch components.
The current INWELT parts list identifies:
These components must be installed in the correct configuration for the selected torch head.
P350 Torch Head, Handle and Trigger
The torch head supports the front-end consumables and forms part of the welding-current transfer path.
The handle accommodates the trigger and provides manual control of the welding gun.
The P350 parts list includes:
When replacing these components, confirm the relevant part reference and attachment configuration.
P350 Wire Liner and Cable Assembly
The wire liner guides welding wire through the torch cable toward the contact tip.
The current standard parts list includes:
Green Steel Liner
Wire Range: Ø1.0–1.2 mm
Length: 3 m
INWELT Code: IJJD0521
Although the P350 welding torch supports Ø0.8–1.6 mm wire, the liner must match the selected wire diameter, material and cable length.
Do not assume that a standard Ø1.0–1.2 mm liner is suitable for every wire size within the torch's stated range.
For larger wire diameters or longer cable assemblies, request the correct liner specification before purchasing.
P350 Panasonic-Style MIG Torch Compatibility
The INWELT P350 belongs to the Panasonic-style MIG welding torch category.
The current technical information lists a Euro Central Connector, while the spare parts list also contains components associated with the MIG/PAN torch connection system.
Therefore, the exact connection configuration should be confirmed for the ordered assembly.
Euro Central Connector and Panasonic-Style Interface
The connector must provide compatible connections for:
Welding power
Welding wire feeding
Shielding gas
Trigger-control signals
Mechanical attachment
A Euro-type connector and a Panasonic-style connection should not be assumed to be interchangeable.
P350 Replacement Torch Compatibility Checklist
Before ordering, confirm the following information.
| Item | What to Check |
| Existing Torch Model | P350 or another model |
| Welding Machine | Manufacturer and model |
| Wire Feeder | Manufacturer and connection type |
| Power Connector | Mechanical and electrical compatibility |
| Gas Connection | Connection arrangement |
| Trigger Connector | Control wiring and contact arrangement |
| Cable Length | 3 m / 4 m / 5 m |
| Welding Wire | Diameter and material |
| Contact Tip | Thread, length and wire size |
| Nozzle and Diffuser | Front-end dimensions and attachment |
For replacement orders, provide photographs of the existing torch connector, torch head and consumables if the original model or part number is unknown.
Spare Parts Details:
| Position | Code | Ref. | Description |
| 1 | IJDT0407 |
| Nozzle P350 |
| 2 | IJGU0679 |
| Grower M21mm |
| 3 | IJDV0757-10 |
| Contact tip(D1.0mm E-CU M6X45 |
| 4 | IJDG0987 |
| Ceramic diffuser P350 |
| 5 | IJDT6610 |
| Insulator P350 |
| 6 | IJDA0750 |
| Torch head P350 |
| 6.1 | IJDG0982 |
| Torch head front part P350 |
| 7 | IJDW0861-01 |
| MIG handle P350/500 |
| 8 | IJGU0885 |
| Screw M3X10mm |
| 9 | IJIR0197 |
| Nut M4 |
| 10 | IJGU0871 |
| Switch for MIG/PAN |
| 11 | IJAI0875 |
| Spring for switch/PAN |
| 12 | IJD00199-01 |
| Joint with spring |
| 13 | IJAI7076 |
| Spring cable support |
| 14 | IJGU0832 |
| Coaxial cable 3m |
| 15 | IJIK0704 |
| Gas connector for MIG torch/PAN |
| 16 | IJGU0031 |
| Back box |
| 17 | IJGU0080 |
| Screw M4X22mm |
| 18 | IJIR0760 |
| Connector 2 holes |
| 19 | IJAU9010 |
| Connector with hexagonal nut 9/16-18 |
| 20 | IJGU0814 |
| Spring for gas tube |
| 21 | IJLI0679 |
| EPDM tube <D5x10mm 300mm |
| 22 | IJJD0521 |
| Green steel liner O1.0-1.2mm 3m |
| 23 | IJDH6011 |
| Spanner for MIG torches |
| 24 | IJDH6018 |
| Spanner for PAN torch |
|
| Complete Torch |
| IJDU6241-36 |
| MIG P350 torch 3m PAN |
| IJDU6247-36 |
| MIG P350 torch 4m PAN |
| IJDU6248-36 |
| MIG P350 torch 5m PAN |
Our Catalog:
 INWELT MIG WELDING TORCH.pdf
How to Choose the Correct P350 MIG Welding Torch
Choosing a P350 MIG welding torch requires verifying the actual welding conditions and equipment configuration.
Step 1: Confirm the Welding Current
The standard P350 is rated at 340A with CO₂ and 320A with mixed shielding gas at a 60% duty cycle.
The intended welding current must remain within the applicable rated conditions.
Step 2: Identify the Shielding Gas
Determine whether the welding process uses CO₂ or an appropriate mixed shielding gas.
The current rating differs between the two conditions.
Step 3: Confirm the Welding Wire Diameter
The P350 supports Ø0.8–1.6 mm welding wire.
Select the correct contact tip, liner and wire-feeding configuration for the required diameter and material.
Step 4: Choose the Cable Length
Select 3 m, 4 m or 5 m according to the welding workstation and required working reach.
Step 5: Verify the Connection Interface
Confirm the physical and electrical interface of the welding gun and wire feeder.
Do not select a replacement gun based solely on its appearance or model designation.
Step 6: Confirm Consumable Availability
Check the required contact tips, nozzles, ceramic diffusers, insulators and liners.
For distributor orders, including spare parts in the initial purchasing plan can simplify future maintenance and stock replenishment.
Industrial Applications of the P350 MIG Welding Gun
The P350 is intended for industrial MIG/MAG welding applications within its specified current and duty-cycle limits.
Structural Steel Fabrication
The P350 can be considered for welding structural frames, brackets and fabricated steel components where the welding parameters are suitable.
Machinery and Equipment Manufacturing
Industrial machinery production often involves welded steel assemblies and fabricated components.
The P350 provides a gas-cooled option for appropriate manual MIG/MAG welding operations.
Trailer and Vehicle Component Fabrication
The P350 can be used in compatible fabrication work involving trailers, vehicle frames and welded metal components.
The appropriate welding wire, shielding gas and current should be selected according to the welding procedure.
General Industrial Fabrication
Fabrication workshops may use the P350 for welding different steel components within the torch's operating limits.
The correct contact tip and liner should be selected for the welding wire being used.
Maintenance and Industrial Repair
The P350 can also be considered for equipment maintenance and repair operations where the welding machine interface and thermal requirements are compatible.
P180 vs. P350 vs. P500 MIG Welding Torches
The P180, P350 and P500 are manual MIG welding torch models within the INWELT PANA Series.
They differ in welding-current capacity and supported wire range.
| Specification | P180 | P350 | P500 |
| Torch Type | MIG/MAG | MIG/MAG | MIG/MAG |
| Cooling | Gas Cooled | Gas Cooled | Gas Cooled |
| CO₂ Current | 200A | 340A | 500A |
| Mixed-Gas Current | 160A | 320A | 450A |
| Duty Cycle | 60% | 60% | 60% |
| Wire Size | Ø0.8–1.2 mm | Ø0.8–1.6 mm | Ø0.8–1.6 mm |
| Cable Length | 3 / 4 / 5 m | 3 / 4 / 5 m | 3 / 4 / 5 m |
| Operation | Manual | Manual | Manual |
When Should You Choose P180?
Choose the P180 when the application requires a lower welding-current range and Ø0.8–1.2 mm welding wire is sufficient.
When Should You Choose P350?
Choose the P350 when the application requires higher current than the P180 can provide while retaining a gas-cooled manual torch configuration.
The P350 also supports a wider listed wire range than the P180.
When Should You Choose P500?
Consider the P500 when the welding application requires higher rated current than the P350.
The correct selection should always account for welding current, shielding gas, duty cycle, wire diameter and thermal conditions.
Common P350 MIG Torch Problems and Solutions
Proper maintenance and matching consumables can help prevent avoidable welding interruptions.
| Problem | Possible Cause | Recommended Check |
| Torch overheating | Excessive current, duty cycle or poor electrical connection | Verify current rating, duty cycle and connections |
| Irregular wire feeding | Worn liner, incorrect tip or excessive cable bends | Inspect liner, contact tip and cable routing |
| Contact tip burnback | Incorrect tip or wire-feeding problem | Check wire size, contact tip and settings |
| Excessive spatter | Incorrect welding parameters or shielding conditions | Inspect process settings and consumables |
| Poor shielding-gas coverage | Blocked nozzle, gas leakage or diffuser problem | Check nozzle, diffuser and gas connections |
| Unstable arc | Poor current transfer or inconsistent wire feeding | Inspect contact tip, liner and electrical connections |
| Trigger not responding | Trigger switch or control connection fault | Inspect trigger and connector |
| Cable damage | Excessive bending, abrasion or mechanical stress | Inspect and replace damaged components |
Why Does a P350 MIG Torch Overheat?
A P350 torch may overheat when the welding current, duty cycle or actual operating conditions exceed the torch's thermal capacity.
Loose electrical connections, worn components and damaged cable assemblies can also contribute to excessive heating.
If overheating occurs, stop welding and inspect the torch after it has cooled.
Why Does a P350 MIG Torch Have Wire Feeding Problems?
Wire feeding problems may occur when the liner is incorrectly sized, worn or contaminated.
An incorrect contact-tip size or excessive cable bending can also interfere with consistent wire feeding.
Check the liner and contact tip against the actual welding wire diameter and cable length.
Why Is the P350 MIG Welding Arc Unstable?
An unstable arc can result from poor electrical contact, wire-feeding irregularities, incorrect shielding gas or unsuitable welding parameters.
Inspect the contact tip, wire liner, shielding-gas system and power connections before replacing the complete torch.
P350 MIG Torch Maintenance and Consumable Replacement
Regular inspection can help maintain the P350 welding gun in appropriate operating condition.
Clean the Gas Nozzle
Remove excessive welding spatter from the nozzle opening and inspect for dents or deformation.
Inspect the Contact Tip
Check the contact-tip bore for wear and damage.
Replace the tip when its condition affects wire feeding or welding-current transfer.
Check the Ceramic Diffuser and Insulator
Inspect the diffuser and insulator for cracks, damage or contamination.
Replace damaged components with parts suitable for the corresponding P350 torch head.
Inspect the Wire Liner
Check for contamination, damage or excessive wire-feed resistance.
Confirm the correct liner size and length before installing a replacement.
Inspect the Cable and Connector
Look for damaged insulation, excessive cable bending, loose electrical connections or signs of overheating.
Check the Handle and Trigger
Inspect the handle and trigger-control mechanism for mechanical damage or improper operation.
Disconnect the equipment and allow the torch to cool before maintenance or replacement of components.
P350 MIG Welding Torches for Distributors and OEM Buyers
INWELT supplies P350 MIG welding torches and related replacement components for international B2B purchasing.
Typical customers include:
Welding equipment distributors
Industrial welding suppliers
Importers and wholesalers
Welding equipment manufacturers
OEM and private-label brands
Industrial fabrication companies
Equipment maintenance suppliers
Wholesale P350 MIG Torch Supply
INWELT offers standard P350 complete torch assemblies with 3 m, 4 m and 5 m cable lengths.
For bulk orders, buyers should confirm:
Complete torch code
Required cable length
Connector configuration
Welding wire size
Consumable specification
Order quantity
Packaging requirements
Destination market
OEM and Private-Label P350 MIG Torches
INWELT supports OEM/ODM inquiries for welding torch projects.
Customization requests may include:
Cable assembly specifications
Connector requirements
Product identification
Private-label packaging
Consumable matching
Order-specific documentation
Bulk packaging configurations
For nonstandard or replacement configurations, provide a technical drawing, existing product sample or detailed specification for review.
P350 Consumable Supply for Distributors
For long-term distributor purchasing, INWELT can discuss supply of corresponding P350 replacement parts.
The relevant components include gas nozzles, contact tips, ceramic diffusers, insulators, torch heads, handles, triggers and liners.
Using verified model codes and part references helps purchasing teams maintain consistent product identification and inventory records.
Frequently Asked Questions About P350 MIG Torches
What is a P350 MIG welding torch?
The P350 is a Panasonic-style gas-cooled MIG/MAG welding torch designed for industrial manual welding. The INWELT model is rated at 340A with CO₂ and 320A with mixed shielding gas at a 60% duty cycle.
Is the INWELT P350 a 350A MIG welding torch?
P350 is the model designation. The current INWELT specification lists 340A with CO₂ and 320A with mixed gas, both at a 60% duty cycle.
What is the duty cycle of the P350 MIG torch?
The INWELT P350 is specified at a 60% duty cycle at its stated welding-current ratings.
Is the P350 gas-cooled or water-cooled?
The INWELT P350 is a gas-cooled, or air-cooled, MIG welding torch. It does not require a separate water-cooling circuit.
What welding wire sizes does the P350 support?
The P350 supports Ø0.8–1.6 mm welding wire. Contact tips and wire liners must be selected according to the actual wire diameter and material.
What cable lengths are available for the P350?
INWELT lists 3 m, 4 m and 5 m complete P350 torch assemblies.
What are the P350 complete torch codes?
The listed complete torch codes are IJDU6241-36 for 3 m, IJDU6247-36 for 4 m and IJDU6248-36 for 5 m. Connector and assembly details should be confirmed before ordering.
Does the P350 use an M6 contact tip?
The current standard INWELT parts list includes an E-Cu contact tip with M6 × 45 dimensions and a Ø1.0 mm wire size. Other sizes require matching components.
What gas nozzle does the P350 use?
The INWELT P350 spare parts list identifies the standard P350 gas nozzle with product code IJDT0407.
Does the P350 use a ceramic gas diffuser?
Yes. The current INWELT P350 parts list includes a ceramic diffuser, product code IJDG0987.
Can the P350 use Ø1.6 mm welding wire?
The torch is specified for Ø0.8–1.6 mm welding wire. However, the standard listed contact tip and liner do not cover every wire diameter in that range. Matching consumables and wire-feeding components must be confirmed for Ø1.6 mm applications.
Is the P350 compatible with all Panasonic MIG welding machines?
No universal compatibility should be assumed. The welding machine connection, power interface, gas supply and trigger wiring must be verified for the specific equipment.
Can the P350 be supplied with a Euro connector?
The current INWELT P350 technical specification lists a Euro Central Connector. The exact connector and complete torch assembly should be confirmed when ordering.
What is the difference between P180 and P350?
The INWELT P180 is rated at 200A CO₂ and 160A mixed gas, while the P350 is rated at 340A CO₂ and 320A mixed gas. Both are listed at a 60% duty cycle.
What is the difference between P350 and P500?
The P500 has a higher listed current rating than the P350. The appropriate model depends on the welding process, required current, shielding gas, duty cycle and application.
Does INWELT supply P350 replacement parts?
Yes. INWELT lists P350 gas nozzles, contact tips, ceramic diffusers, insulators, torch heads, handles, triggers and liner components.
Can INWELT supply OEM P350 MIG welding torches?
Yes. INWELT supports OEM/ODM inquiries for P350 welding torches, including cable, connector, packaging and private-label requirements.
Can welding distributors purchase P350 torches in bulk?
Yes. INWELT supplies P350 welding torches and replacement components for distributor, wholesale and industrial purchasing projects.
Request a P350 MIG Welding Torch Quote
Looking for a P350 Panasonic-style MIG welding torch manufacturer or wholesale supplier?
INWELT supplies P350 gas-cooled MIG welding guns and replacement parts for welding equipment distributors, importers, OEM brands and industrial buyers.
To request a quotation, please provide:
Required product model: P350
Cable length: 3 m / 4 m / 5 m
Welding machine and wire feeder model
Connector type
Welding wire diameter
Required consumables or spare parts
Order quantity
OEM/ODM requirements
Destination market
Contact INWELT for P350 MIG Welding Torch Specifications, Bulk Pricing, Spare Parts and OEM/ODM Inquiries.
 English
 简体中文
 العربية
 Français
 Русский
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 ភាសាខ្មែរ
 Bahasa Melayu
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Čeština
 Монгол
 қазақ
 Српски
 हिन्दी
 فارسی
 Slovenčina
 Slovenščina
 Norsk
 Svenska
 українська
 Ελληνικά
 Suomi
 Latine
 Dansk
 বাংলা
 Hrvatski
 Afrikaans
 Gaeilge
 Eesti keel
 नेपाली
 Oʻzbekcha
 latviešu
 Azərbaycan dili
 Беларуская мова
 Bosanski
 Български
 ქართული
 Lietuvių



