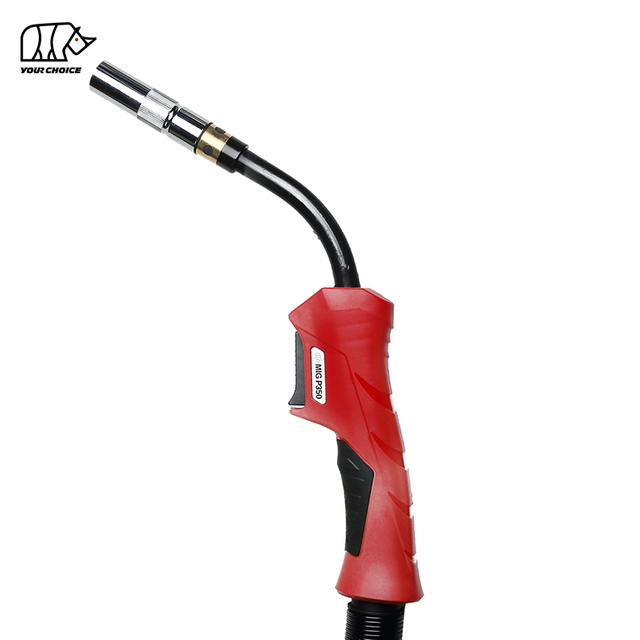
P500 Panasonic-Style MIG Welding Torch Overview
The INWELT P500 Panasonic-Style MIG Welding Torch is a heavy-duty, air-cooled MIG/MAG welding gun designed for high-current manual welding applications. It is rated at 500A with CO₂ shielding gas and 450A with mixed shielding gas at a 60% duty cycle.
The P500 supports welding wire diameters from Ø0.8 mm to Ø1.6 mm and is available with 3 m, 4 m and 5 m cable assemblies. Its gas-cooled construction allows it to operate without an external liquid-cooling system, making it an option for industrial welding applications where the required current and duty cycle fall within the torch's rated specifications.
As part of the INWELT PANA Series, the P500 is positioned above the P350 in rated welding-current capacity. It is intended for fabrication workshops, industrial manufacturing facilities, equipment maintenance providers and welding equipment distributors.
INWELT supplies P500 MIG welding guns and related replacement components for international wholesale, industrial and OEM/ODM purchasing requirements.
P500 MIG Welding Torch Technical Specifications
The following specifications describe the standard INWELT P500 product range.
| Specification | INWELT P500 |
| Brand | INWELT |
| Model | P500 |
| Product Type | Panasonic-Style MIG Welding Torch |
| Welding Process | MIG / MAG (GMAW) |
| Cooling Method | Gas Cooled / Air Cooled |
| Rated Current with CO₂ | 500A |
| Rated Current with Mixed Gas | 450A |
| Duty Cycle | 60% |
| Welding Wire Diameter | Ø0.8–1.6 mm |
| Cable Length Options | 3 m / 4 m / 5 m |
| Connection Interface | Confirm for the selected torch assembly |
| Front-End Components | Gas Nozzle, Contact Tip, Diffuser, Insulator and Torch Neck |
| Application | Industrial Manual MIG/MAG Welding |
| Supply Options | Wholesale / OEM / ODM |
The current ratings apply at the specified duty cycle and shielding-gas conditions.
The correct torch configuration should be selected according to the welding machine, wire feeder, shielding gas, required welding current, welding wire diameter and operating duration.
For replacement or bulk orders, the complete torch model, connector configuration and consumable specifications should be confirmed before production.
Key Features of the INWELT P500 MIG Gun
500A CO₂ and 450A Mixed-Gas Welding Capacity
The INWELT P500 is specified for high-current MIG/MAG welding operations.
Its rated welding-current specifications are:
These ratings help industrial buyers evaluate the P500 for applications requiring higher current capacity than lower-rated manual MIG welding torches.
The actual welding current must remain within the specified thermal and electrical operating conditions.
Air-Cooled Design for Industrial MIG Welding
The P500 uses an air-cooled, also referred to as gas-cooled, MIG welding torch configuration.
Unlike a water-cooled torch, the P500 does not require a separate cooling-water circulation system.
This can simplify the overall equipment configuration where an air-cooled torch provides sufficient current capacity and duty-cycle performance.
However, an air-cooled torch is not intended for unlimited operation at its maximum current rating.
High-current welding generates significant thermal loads in the torch neck, contact tip, front-end components and cable assembly. The specified duty cycle and appropriate consumable condition must therefore be maintained.
3 m, 4 m and 5 m Cable Length Options
The P500 is available with standard cable lengths of:
The appropriate cable length depends on the welding workstation layout, distance from the wire feeder and required operator movement.
Shorter cables can reduce unnecessary cable routing in compact welding areas.
Longer cables provide additional working reach but should be installed without excessive bending or mechanical strain.
For industrial applications, the cable assembly must also be suitable for the required welding current and wire-feeding configuration.
Serviceable Torch Handle and Front-End Components
The P500 is designed around a handheld MIG welding gun assembly with replaceable front-end consumables.
Typical serviceable components include:
These components should be selected according to the actual P500 assembly specification.
Replacement-part compatibility must be confirmed using product references, technical dimensions or approved samples.
Understanding the P500 MIG Torch Duty Cycle
The INWELT P500 has a specified 60% duty cycle.
Duty cycle describes the allowable welding time within a standard ten-minute operating period at the stated rated load and test conditions.
At a 60% duty cycle, the torch can operate for six minutes during a ten-minute period at the applicable rated conditions, followed by sufficient non-welding time to remain within its thermal limits.
P500 Duty Cycle with CO₂ Shielding Gas
Rated current: 500A
Shielding gas: CO₂
Duty cycle: 60%
P500 Duty Cycle with Mixed Shielding Gas
Rated current: 450A
Shielding gas: Mixed gas
Duty cycle: 60%
The P500 should not be assumed to have a 100% duty cycle at 500A or 450A.
What Affects P500 MIG Torch Temperature?
The operating temperature of a MIG welding gun can be influenced by:
Welding current
Arc-on time
Shielding-gas composition
Condition of electrical connections
Cable assembly condition
Contact-tip and torch-neck condition
Ambient temperature
Welding position and workpiece access
For high-current production welding, operators should check torch temperature and consumable condition as part of routine maintenance.
If the intended welding process requires continuous operation beyond the rated duty cycle, a suitable higher-duty-cycle configuration or water-cooled torch should be evaluated.
P500 MIG Welding Gun Cable and Connector Options
Connector compatibility is an important consideration when ordering a P500 replacement welding gun.
Panasonic-style welding guns may be supplied with different mechanical and electrical interfaces depending on the welding machine and wire feeder.
The complete connector configuration must be verified before confirming compatibility.
PNA-Style and Euro Connector Compatibility
PNA-style and Euro central connector systems are not automatically interchangeable.
The required connection must be checked for:
Power connection dimensions
Welding wire feed alignment
Shielding-gas connection
Trigger-control wiring
Mechanical attachment
Cable assembly configuration
Buyers should not assume that a P500 torch will connect to every MIG welding machine simply because the machine has a suitable current rating.
When replacing an existing welding gun, provide the welding machine model, wire feeder model and photographs of the existing connector.
Choosing the Correct P500 Cable Length
| Cable Length | Typical Selection Consideration |
| 3 m | Compact welding stations and shorter working distances |
| 4 m | General industrial fabrication workstations |
| 5 m | Larger work areas requiring additional operator reach |
Cable length should be evaluated together with wire-feeding performance and cable routing requirements.
For OEM applications, the final cable assembly and connector configuration should be confirmed from technical specifications.
P500 MIG Torch Consumables and Spare Parts
P500 welding gun consumables and replacement parts must be matched to the actual P500 front-end and cable assembly configuration.
Although some MIG torch product families may share certain handle or accessory designs, parts should not be assumed to be interchangeable solely because they appear similar.
For replacement orders, INWELT recommends confirming the original part reference, dimensions or product sample.
P500 Consumable and Replacement Part Categories
| Component | Main Function | Information Required for Ordering |
| Gas Nozzle | Directs shielding gas around the welding arc | Nozzle dimensions and attachment type |
| Contact Tip | Transfers welding current to the electrode wire | Wire diameter, thread and length |
| Gas Diffuser | Distributes shielding gas in the torch front end | Torch-head configuration and part dimensions |
| Insulator | Provides electrical separation where required | Matching torch-head configuration |
| Torch Neck | Supports the front-end assembly and current transfer path | Neck geometry and connection |
| Wire Liner | Guides the electrode wire through the cable | Wire diameter, wire type and cable length |
| Trigger Assembly | Controls the welding operation | Switch and handle configuration |
| Cable Assembly | Carries welding current, wire and gas through the gun | Cable length and connector requirements |
| Rear Connector | Interfaces with the wire feeder and welding system | Connector type and dimensions |
P500 Gas Nozzle and Contact Tips
The gas nozzle directs shielding gas toward the welding area and surrounds the welding arc.
A correctly selected nozzle helps establish the required shielding-gas coverage and clearance around the contact tip.
The contact tip transfers electrical current to the continuously fed welding wire.
When selecting a P500 contact tip, confirm:
The P500 supports Ø0.8–1.6 mm welding wire, but a suitable contact tip must be selected for the actual wire size.
Do not assume that one contact tip can accommodate every wire diameter in the supported range.
P500 Ceramic Diffuser, Insulator and Torch Neck
The diffuser distributes shielding gas through the torch front-end assembly.
Insulating components provide electrical separation between designated parts of the torch.
The torch neck supports the contact-tip and nozzle assembly and contributes to the welding-current transfer path.
For replacement orders, the diffuser, insulator and neck should be checked as a matched front-end system.
P350 and P500 front-end consumables should not be treated as interchangeable unless their compatibility has been technically verified.
A shared handle design, where applicable, does not establish compatibility between all torch heads, nozzles, diffusers or insulating components.
P500 Wire Liners and Cable Assemblies
The welding wire liner guides the electrode wire from the wire feeder toward the contact tip.
The correct liner depends on:
The P500 supports Ø0.8–1.6 mm welding wire. However, the liner must be selected for the intended wire size and complete cable assembly.
An incorrectly sized or damaged liner can contribute to inconsistent feeding, excessive resistance and wire blockage.
For Ø1.6 mm applications, verify the appropriate liner and contact-tip configuration before ordering.
Is the P500 Compatible with Panasonic-Style MIG Welders?
The INWELT P500 belongs to the Panasonic-style MIG welding torch category.
It can be evaluated for welding equipment requiring a corresponding P500-type gun configuration.
However, the Panasonic-style designation does not guarantee universal compatibility with every Panasonic or other MIG welding machine.
Actual compatibility depends on the connection system, wire feeder, power connection and control interface.
P500 Replacement Torch Compatibility Checklist
| Item | What to Confirm |
| Original Torch | Existing model and assembly type |
| Welding Machine | Manufacturer and model |
| Wire Feeder | Model and output connection |
| Rated Welding Current | Required current and duty cycle |
| Shielding Gas | CO₂ or mixed gas |
| Power Connector | Mechanical and electrical dimensions |
| Trigger Connector | Control wiring and plug type |
| Gas Connection | Connection configuration |
| Cable Length | 3 m / 4 m / 5 m |
| Welding Wire | Diameter and material |
| Front-End Consumables | Contact tip, nozzle, diffuser and neck |
For a replacement welding gun, provide the existing torch model and photographs of the front end and rear connector.
Spare Parts Details:
| Position | Code | Ref. | Description |
| 1 | IJDT0407 |
| Nozzle P350 |
| 2 | IJGU0679 |
| Grower M21mm |
| 3 | IJDV0757-10 |
| Contact tip(D1.0mm E-CU M6X45 |
| 4 | IJDG0987 |
| Ceramic diffuser P350 |
| 5 | IJDT6610 |
| Insulator P350 |
| 6 | IJDA0750 |
| Torch head P350 |
| 6.1 | IJDG0982 |
| Torch head front part P350 |
| 7 | IJDW0861-01 |
| MIG handle P350/500 |
| 8 | IJGU0885 |
| Screw M3X10mm |
| 9 | IJIR0197 |
| Nut M4 |
| 10 | IJGU0871 |
| Switch for MIG/PAN |
| 11 | IJAI0875 |
| Spring for switch/PAN |
| 12 | IJD00199-01 |
| Joint with spring |
| 13 | IJAI7076 |
| Spring cable support |
| 14 | IJGU0832 |
| Coaxial cable 3m |
| 15 | IJIK0704 |
| Gas connector for MIG torch/PAN |
| 16 | IJGU0031 |
| Back box |
| 17 | IJGU0080 |
| Screw M4X22mm |
| 18 | IJIR0760 |
| Connector 2 holes |
| 19 | IJAU9010 |
| Connector with hexagonal nut 9/16-18 |
| 20 | IJGU0814 |
| Spring for gas tube |
| 21 | IJLI0679 |
| EPDM tube <D5x10mm 300mm |
| 22 | IJJD0521 |
| Green steel liner O1.0-1.2mm 3m |
| 23 | IJDH6011 |
| Spanner for MIG torches |
| 24 | IJDH6018 |
| Spanner for PAN torch |
|
| Complete Torch |
| IJDU6241-36 |
| MIG P350 torch 3m PAN |
| IJDU6247-36 |
| MIG P350 torch 4m PAN |
| IJDU6248-36 |
| MIG P350 torch 5m PAN |
Our Catalog:
 INWELT MIG WELDING TORCH.pdf
How to Choose the Correct P500 MIG Welding Torch
Selecting the right P500 requires matching the welding gun to the actual welding application.
Step 1: Verify the Welding Current
Check the intended welding current against the P500 rated capacity.
The INWELT P500 is rated at 500A with CO₂ and 450A with mixed gas at a 60% duty cycle.
Step 2: Identify the Shielding Gas
Confirm whether the process uses CO₂ or mixed shielding gas.
The allowable current differs between these operating conditions.
Step 3: Evaluate the Duty Cycle
Consider the expected arc-on time and welding production schedule.
Where continuous high-current welding is required, evaluate whether a 60% duty-cycle air-cooled torch meets the operating requirements.
Step 4: Confirm the Welding Wire Diameter
The P500 supports Ø0.8–1.6 mm welding wire.
The contact tip, wire liner and feeding system must be selected for the intended wire diameter and material.
Step 5: Choose the Cable Length
Select 3 m, 4 m or 5 m according to the welding station layout and required working reach.
Step 6: Verify the Connector
Confirm the mechanical, power, gas and trigger connections.
Do not purchase a replacement torch based only on the welding machine's rated amperage.
Step 7: Confirm Replacement Parts
For industrial and distributor orders, identify the correct P500 consumables and replacement components before purchasing.
This helps support future maintenance and repeat ordering.
Industrial Applications of the P500 MIG Gun
The P500 is intended for high-current manual MIG/MAG welding applications within its rated operating limits.
Heavy Structural Steel Fabrication
The P500 can be considered for welding structural frames, beams, brackets and fabricated steel assemblies where the selected welding procedure falls within the torch's rated conditions.
Heavy Machinery Manufacturing
Industrial equipment manufacturing frequently involves welding fabricated steel components.
The P500 provides a gas-cooled torch option for suitable high-current welding operations.
Construction Equipment Fabrication
The torch can be evaluated for compatible welding applications involving equipment frames, fabricated parts and structural assemblies.
The final torch selection should reflect the workpiece material, welding wire, shielding gas and required production conditions.
Shipbuilding and Large Steel Assemblies
High-current MIG/MAG welding is used in shipbuilding and large-scale steel fabrication.
The P500 may be considered for suitable manual welding operations, provided that its 60% duty cycle and other operating limits are respected.
Industrial Maintenance and Repair
The P500 can be used in compatible equipment repair and industrial maintenance applications where the welding machine, wire feeder and torch connection match.
High-Current Production Welding
For repetitive or production welding, the P500 should be selected according to the required current, arc-on time, operator access and consumable maintenance requirements.
A water-cooled welding gun may be preferable for applications requiring higher continuous thermal capacity.
P350 vs. P500 MIG Welding Torch
The INWELT P350 and P500 are Panasonic-style gas-cooled MIG welding torches within the PANA Series.
They share the same general product family but offer different rated welding-current capacities.
| Specification | P350 | P500 |
| Product Type | Panasonic-Style MIG Torch | Panasonic-Style MIG Torch |
| Cooling Method | Gas Cooled | Gas Cooled |
| CO₂ Rated Current | 340A | 500A |
| Mixed-Gas Rated Current | 320A | 450A |
| Duty Cycle | 60% | 60% |
| Welding Wire Diameter | Ø0.8–1.6 mm | Ø0.8–1.6 mm |
| Standard Cable Lengths | 3 / 4 / 5 m | 3 / 4 / 5 m |
| Main Selection Factor | Medium-to-high-current welding | Higher-current welding |
When Should You Choose P350?
Choose P350 when the required welding current and duty cycle are within the P350 rated specifications.
It may be the more suitable choice where a 500A-class torch is unnecessary.
When Should You Choose P500?
Choose P500 when the welding application requires higher current capacity than the P350 can provide, while remaining within the P500 rated operating conditions.
Are P350 and P500 Consumables Interchangeable?
Not necessarily.
The two models should be treated as separate front-end consumable configurations unless the exact parts have been confirmed as interchangeable.
Always verify the nozzle, diffuser, insulator, torch neck and contact-tip specifications.
Common P500 MIG Torch Problems and Solutions
High-current MIG welding places significant demands on the gun, cable and consumable system.
Regular inspection and correct component selection can help identify problems before they lead to unnecessary replacement.
| Problem | Possible Cause | Recommended Check |
| Torch overheating | Excessive current, duty cycle or electrical resistance | Check current, operating time and connections |
| Contact tip burnback | Wire-feeding problems or incorrect contact-tip selection | Inspect tip, wire size and welding parameters |
| Irregular wire feeding | Worn liner, wrong liner size or tight cable bends | Check liner and cable routing |
| Excessive spatter | Incorrect process settings or shielding conditions | Inspect welding settings and consumables |
| Poor shielding-gas coverage | Nozzle blockage, leaks or diffuser damage | Inspect nozzle, diffuser and gas connections |
| Unstable arc | Inconsistent wire feeding or current transfer | Check tip, liner and power connections |
| Trigger failure | Trigger switch or control-wire fault | Inspect switch and connector |
| Cable overheating | Loose connection or damaged cable conductor | Inspect cable and electrical terminations |
Why Does a P500 MIG Welding Torch Overheat?
A P500 MIG torch may overheat if the welding current or arc-on time exceeds its rated operating conditions.
Other causes may include loose electrical connections, damaged cable assemblies or worn front-end components.
If overheating occurs, stop welding, allow the equipment to cool and inspect the complete torch assembly.
Why Does a P500 MIG Gun Have Wire Feeding Problems?
Wire-feeding problems may be caused by incorrect liner size, liner contamination, contact-tip wear or excessive cable bending.
Inspect the liner, contact tip and drive system together.
For larger welding wire diameters, confirm that the liner and contact tip are matched to the required wire size.
Why Is the P500 Welding Arc Unstable?
An unstable MIG welding arc may result from inconsistent wire feeding, poor electrical contact, unsuitable shielding-gas flow or incorrect welding parameters.
Check the welding machine settings, contact tip, gas delivery system and electrical connections before replacing the entire welding gun.
P500 MIG Torch Maintenance and Consumable Replacement
Routine maintenance helps keep the P500 welding gun in suitable operating condition.
Clean the Gas Nozzle
Remove excessive welding spatter from the nozzle opening.
Inspect the nozzle for dents, deformation or damage that may affect shielding-gas coverage.
Inspect the Contact Tip
Check the contact-tip bore for excessive wear or damage.
Replace the tip when its condition affects electrical contact or welding wire feeding.
Check the Gas Diffuser and Insulator
Inspect the front-end components for cracks, damage or contamination.
Use components matched to the selected P500 torch head.
Inspect the Torch Neck
Check for damage, loose connections or signs of abnormal heating.
A damaged torch neck should be replaced with a compatible component.
Inspect the Wire Liner
Check for contamination, wear, incorrect dimensions or excessive wire-feeding resistance.
Use a liner matched to the welding wire diameter and cable length.
Inspect the Cable Assembly
Check cable insulation, strain-relief components and electrical connections.
Avoid excessive bending, abrasion and other mechanical damage.
Check the Trigger and Rear Connector
Verify the trigger operation and inspect the rear connection components for looseness or visible damage.
Disconnect the welding equipment and allow the gun to cool before maintenance or replacement of components.
P500 MIG Welding Torches for Distributors and OEM Buyers
INWELT supplies P500 MIG welding guns and related welding torch components for international B2B purchasing requirements.
Typical customers include:
Welding equipment distributors
Industrial welding suppliers
Importers and wholesalers
Welding equipment manufacturers
OEM and private-label brands
Industrial fabrication companies
Equipment maintenance suppliers
Wholesale P500 MIG Welding Torch Supply
INWELT offers P500 MIG welding guns with 3 m, 4 m and 5 m cable length options.
For bulk orders, buyers should confirm:
OEM and Private-Label P500 MIG Torches
INWELT supports OEM/ODM inquiries for MIG welding torch projects.
Customization requirements may include:
For nonstandard configurations, please provide the relevant sample, drawing or detailed specification for technical review.
Replacement Consumable Supply
INWELT can discuss the required P500 consumables and replacement parts as part of a wholesale or OEM purchasing project.
For repeat orders, confirmed part numbers and approved technical specifications help maintain consistent product identification and purchasing records.
Frequently Asked Questions About P500 MIG Welding Torches
What is a P500 MIG welding torch?
The P500 is a Panasonic-style gas-cooled MIG/MAG welding torch designed for high-current manual welding applications. The INWELT P500 is rated at 500A with CO₂ and 450A with mixed shielding gas at a 60% duty cycle.
Is the P500 a 500A MIG welding gun?
Yes. The INWELT P500 is rated at 500A with CO₂ shielding gas at a 60% duty cycle. Its mixed-gas rating is 450A at the same duty cycle.
What is the duty cycle of the P500 MIG torch?
The INWELT P500 has a 60% duty cycle at its stated current ratings.
Is the P500 air-cooled or water-cooled?
The P500 is an air-cooled, or gas-cooled, MIG welding gun. It does not require a separate water-cooling system.
What welding wire sizes does the P500 support?
The P500 supports Ø0.8–1.6 mm welding wire. Contact tips and liners must be selected for the actual wire diameter and material.
What cable lengths are available for the P500?
INWELT offers P500 cable length options of 3 m, 4 m and 5 m.
Can the P500 use CO₂ and mixed shielding gases?
Yes. The INWELT P500 has separate rated welding-current specifications for CO₂ and mixed shielding gases.
Is the P500 compatible with all Panasonic MIG welding machines?
No universal compatibility should be assumed. The connector, wire feeder, power connection, gas connection and trigger-control system must be verified for the specific equipment.
Can the P500 be supplied with a Euro connector?
A Euro connector configuration should be confirmed with INWELT before ordering. Compatibility depends on the complete torch assembly and the welding machine interface.
Are P350 and P500 MIG torch spare parts interchangeable?
Not automatically. The exact component dimensions, torch-head configuration and part references must be verified before using parts from one model on the other.
What consumables does a P500 MIG welding gun use?
The P500 uses a front-end consumable system including a gas nozzle, contact tip, diffuser and insulating components. The exact parts should be selected according to the P500 torch configuration.
Can I use Ø1.6 mm welding wire with the P500?
The P500 is specified for welding wire up to Ø1.6 mm. A suitable Ø1.6 mm contact tip, liner and wire-feeding configuration must be confirmed before use.
What is the difference between P350 and P500?
The P350 is rated at 340A with CO₂ and 320A with mixed gas, while the P500 is rated at 500A with CO₂ and 450A with mixed gas. Both are listed at a 60% duty cycle.
Is the P500 suitable for continuous 500A welding?
The P500 is rated at 500A with CO₂ at a 60% duty cycle, not 100%. For continuous high-current operation, the welding gun must be selected according to the required duty cycle and thermal conditions.
Can the P500 be used for aluminum MIG welding?
The P500 supports MIG welding wire within its specified diameter range, but aluminum welding suitability depends on the entire wire-feeding system, liner, contact tip, shielding gas and welding procedure. A conventional steel-wire liner should not automatically be used for aluminum wire.
Does INWELT offer OEM P500 MIG welding torches?
Yes. INWELT supports OEM/ODM inquiries for P500 welding guns, including cable assembly, connector, labeling and packaging requirements.
Can distributors purchase P500 MIG welding guns in bulk?
Yes. INWELT supplies P500 MIG welding guns for wholesale, distributor and industrial purchasing projects.
Request a P500 MIG Welding Torch Quote
Looking for a P500 Panasonic-style MIG welding torch manufacturer or wholesale supplier?
INWELT supplies P500 air-cooled MIG welding guns and related replacement components for welding equipment distributors, importers, OEM brands and industrial buyers.
For an accurate quotation, please provide:
Required product model: P500
Cable length: 3 m / 4 m / 5 m
Welding machine and wire feeder model
Required connector type
Welding wire diameter
Shielding gas and operating current
Required consumables or spare parts
Order quantity
OEM/ODM requirements
Destination market
Contact INWELT for P500 MIG Welding Torch Specifications, Bulk Pricing, Replacement Parts and OEM/ODM Inquiries.
 English
 简体中文
 العربية
 Français
 Русский
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 ភាសាខ្មែរ
 Bahasa Melayu
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Čeština
 Монгол
 қазақ
 Српски
 हिन्दी
 فارسی
 Slovenčina
 Slovenščina
 Norsk
 Svenska
 українська
 Ελληνικά
 Suomi
 Latine
 Dansk
 বাংলা
 Hrvatski
 Afrikaans
 Gaeilge
 Eesti keel
 नेपाली
 Oʻzbekcha
 latviešu
 Azərbaycan dili
 Беларуская мова
 Bosanski
 Български
 ქართული
 Lietuvių