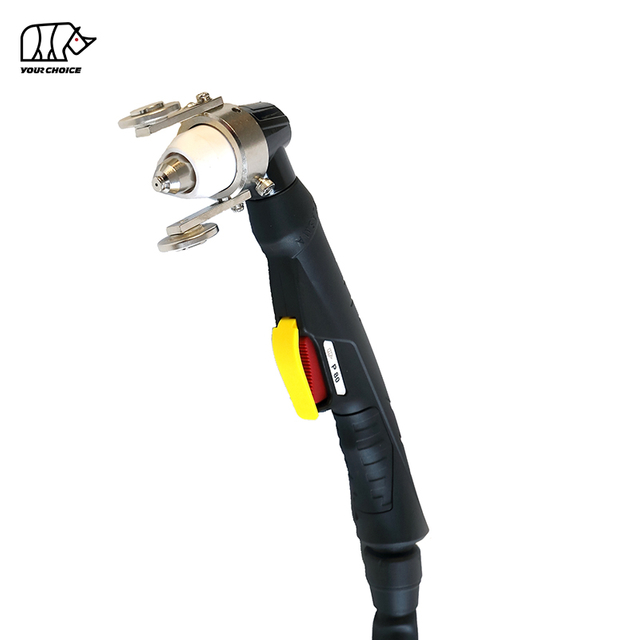
P80 Coated Contact Cutting Plasma Nozzle – Anti-Slag Tip
Share to:
INWELT P80 Coated Contact Cutting Plasma Nozzles are copper-based replacement cutting tips designed for compatible P80 air plasma torch configurations. Their anti-slag surface coating is intended to help reduce molten-metal adhesion and support easier consumable maintenance. The published range includes 1.1, 1.3, 1.5 and 1.7 mm orifices, with catalog current references of 40A, 60A, 80A and 100A. Buyers should verify torch rating, electrode, shield and contact-cutting arrangement before installation. INWELT welcomes bulk orders and OEM packaging inquiries from plasma consumable distributors, equipment suppliers and industrial buyers.
INWELT P80 Plasma Cutting Nozzles | Contact Cutting Type | Anti-Slag Coating | Copper Body | OEM & Bulk Supply
The INWELT P80 Coated Contact Cutting Plasma Nozzle is a copper-based plasma cutting consumable with a protective surface coating designed to help reduce molten-slag adhesion during cutting.
Developed for compatible P80 air plasma torch configurations, this coated nozzle is offered for contact-cutting applications using the correct torch front-end assembly.
The published product range includes nozzle orifices of 1.1 mm, 1.3 mm, 1.5 mm and 1.7 mm, with catalog current references from 40A to 100A.
The correct nozzle must be selected according to the plasma cutter, torch model, operating current, electrode, shield arrangement and cutting application.
INWELT welcomes wholesale, distributor and OEM inquiries for coated P80 plasma cutting nozzles and related consumables.
What Is a P80 Coated Contact Cutting Nozzle?
A P80 coated contact cutting nozzle is a replaceable plasma torch consumable designed to direct and constrict the plasma arc through a precision-sized opening.
The nozzle is manufactured with a copper-based body and a surface coating intended to reduce the tendency of molten cutting slag to adhere to exposed areas.
This product is a coated contact-cutting nozzle variant, rather than a complete plasma cutting torch or a plasma electrode.
Its contact-cutting designation refers to an intended cutting configuration. The complete assembly must be verified before the torch is operated in contact with the workpiece.
How Does the Anti-Slag Coating Work?
During air plasma cutting, molten metal and spatter can reach the torch front end.
Deposits on a cutting nozzle or shield may affect gas flow, interfere with the cutting arc and increase the frequency of consumable inspection or replacement.
The surface coating on the INWELT P80 nozzle is intended to help reduce slag adhesion compared with an untreated surface under suitable operating conditions.
Potential operational benefits include:
Reduced tendency for molten slag to adhere to the coated surface
Easier inspection of the nozzle front end
Support for more consistent consumable maintenance
Additional surface protection in suitable cutting applications
Actual performance depends on coating condition, cutting current, air quality, workpiece material and operating technique.
Coating performance and service-life improvements should be evaluated using controlled comparative tests rather than assumed from the presence of a coating alone.
Is Contact Cutting the Same as Contact-Start Ignition?
No.
Contact cutting describes the relationship between the torch front end and the workpiece during the cutting operation.
Contact-start ignition refers to how the plasma arc is initially established.
A P80 torch may use a high-frequency starting method while its front-end consumable arrangement is configured for a particular cutting technique.
The presence of a contact-cutting nozzle does not change the power source's ignition system.
Only use the nozzle with an approved contact-cutting consumable assembly.
P80 Coated Plasma Nozzle Technical Specifications
Parameter
Specification
Product Name
P80 Coated Contact Cutting Plasma Nozzle
Brand
INWELT
Product Type
Plasma Cutting Nozzle / Cutting Tip
Torch Family
P80
Nozzle Body
Copper-Based
Surface Treatment
Anti-Slag Coating
Intended Configuration
Contact Cutting
Nozzle Orifice Options
1.1 / 1.3 / 1.5 / 1.7 mm
Catalog Current References
40A / 60A / 80A / 100A
Cutting Process
Air Plasma Cutting
Primary Application
Cutting Electrically Conductive Metals
Operating Method
Manual Cutting; other applications subject to configuration
Compatible Consumables
Matching P80 Electrode, Shield and Retaining Components
Coating Specification
To Be Confirmed
Product Part Numbers
To Be Confirmed
Standard Packaging
To Be Confirmed
Bulk Supply
Available for Inquiry
OEM / ODM
Subject to Project Confirmation
Specification Note: The listed nozzle orifice and current combinations are taken from INWELT's existing public product information. Confirm the exact nozzle variant, torch rating and consumable configuration before ordering.
P80 Nozzle Orifice Sizes and Current Selection
The nozzle orifice diameter is a critical factor in plasma cutting performance.
It influences the plasma jet geometry and must be matched with the intended cutting current and torch configuration.
P80 Coated Nozzle Size Chart
Nozzle Orifice
Catalog Current Reference
Typical Selection
1.1 mm
40A
Lower-current cutting configurations
1.3 mm
60A
Medium-current cutting configurations
1.5 mm
80A
Higher-current P80 cutting configurations
1.7 mm
100A
Separate compatible higher-current configurations
The 100A listing is a nozzle-series reference only. It does not increase the rated capacity of an 80A P80 torch.
The equipment manufacturer’s approved operating limits always take precedence over a nozzle catalog current reference.
How Does Nozzle Diameter Affect Plasma Cutting?
A smaller nozzle opening is generally associated with lower-current cutting configurations.
A larger opening may be required for a higher operating current, provided that the torch and power source support that configuration.
Using the wrong nozzle size can contribute to:
Unstable arc behavior
Excessive nozzle wear
Poor kerf consistency
Increased edge bevel
Unwanted dross formation
Premature consumable failure
The correct diameter must be selected together with gas flow, air pressure, arc characteristics and material thickness.
Key Features of INWELT Coated P80 Cutting Tips
Anti-Slag Coated Surface
The coating is designed to help limit the adhesion of cutting slag to the nozzle surface.
This feature is relevant to cutting operations where molten-metal deposits make consumable inspection and maintenance more frequent.
Copper-Based Nozzle Construction
The nozzle uses a copper-based body.
Copper is commonly used in air plasma cutting consumables because of its thermal and electrical properties.
Material grade and exact coating composition should be confirmed through the product's technical specification.
Multiple Orifice Options
The published coated nozzle range includes four orifice sizes:
1.1 mm
1.3 mm
1.5 mm
1.7 mm
This allows purchasing teams to identify nozzle options by specification rather than ordering only by the general P80 model name.
Intended for Contact-Cutting Configurations
The nozzle is marketed for P80 contact-cutting arrangements.
Correct use requires a matching shield, retaining system and complete torch front-end configuration.
A contact-cutting designation should not be interpreted as permission to drag an exposed nozzle directly against a workpiece.
Industrial Replacement Consumable
P80 nozzles are replaceable consumables.
Regular inspection and correct replacement help support consistent cutting performance and reduce the risk of damage to related torch components.
Coated vs Standard P80 Plasma Cutting Nozzles
Both coated and standard P80 nozzles perform the same basic function: constricting and directing the plasma arc.
Their main distinction is the surface treatment.
Feature
Coated P80 Nozzle
Standard P80 Nozzle
Main Function
Constrict and direct plasma arc
Constrict and direct plasma arc
Nozzle Body
Copper-based
Commonly copper-based
Surface
Protective anti-slag coating
Standard surface finish
Intended Benefit
Reduced slag adhesion
Conventional cutting performance
Inspection Requirements
Regular inspection
Regular inspection
Compatibility
Requires matching P80 assembly
Requires matching P80 assembly
Service Life
Depends on actual conditions
Depends on actual conditions
When Should You Choose a Coated P80 Nozzle?
A coated nozzle may be worth evaluating when molten slag frequently accumulates around the front-end consumables.
It may also be relevant to distributors seeking a differentiated product option alongside conventional P80 nozzles.
However, coating alone does not guarantee better cut quality or longer nozzle life.
Air quality, consumable alignment, correct current settings and cutting technique remain essential.
Contact Cutting vs Standoff Plasma Cutting
Contact cutting and standoff cutting are different ways of positioning the plasma torch relative to the workpiece.
Contact Cutting
Contact cutting uses a designated front-end consumable arrangement that permits the intended contact or drag-cutting technique.
The correct shield or contact structure maintains the required relationship between the nozzle and the workpiece.
The torch manufacturer's approved configuration must be followed.
Standoff Cutting
Standoff cutting maintains a defined gap between the torch front end and the workpiece.
The required distance depends on the torch, consumables, current and cutting process.
Which Method Is Better?
Neither method is universally better.
The correct choice depends on:
Torch design
Consumable configuration
Cutting current
Workpiece thickness
Required cut quality
Manual or mechanized operation
Do not interchange contact-cutting and standoff-cutting components without confirming the complete consumable assembly.
What Materials Can P80 Coated Nozzles Cut?
When used with a compatible air plasma cutting system, P80 consumables can be used to cut electrically conductive metals.
Carbon Steel Plasma Cutting
Air plasma cutting is commonly used for carbon steel fabrication, repair and plate cutting.
Correct nozzle selection helps maintain a suitable plasma jet for the selected current and plate thickness.
Stainless Steel Plasma Cutting
P80 plasma systems can cut stainless steel using appropriate process parameters.
Cutting quality depends on consumable condition, gas supply, current and travel speed.
Aluminum Plasma Cutting
Aluminum can be cut with a suitable plasma system.
Operators should verify the cutting setup, current and nozzle selection for the material thickness and desired finish.
Scrap Metal and Maintenance Cutting
Contact-cutting configurations may be relevant to certain manual repair and metal-processing applications when the complete torch system supports the operating technique.
Applications should be evaluated according to the specific P80 assembly and cutting procedure.
How to Choose the Correct P80 Coated Nozzle
Step 1: Confirm the Plasma Torch Model
Identify the installed torch model.
A plasma cutting machine labeled CUT80 does not necessarily use a P80 torch.
Different torch families may have different nozzle dimensions, electrode arrangements and starting systems.
Step 2: Confirm the Operating Current
Check the power source output and the torch’s rated current.
Select a nozzle size suitable for the verified operating configuration.
Do not exceed the rated capacity of the torch or its approved consumables.
Step 3: Confirm the Nozzle Orifice Diameter
Choose the correct nozzle opening according to the required current and consumable specification.
Common catalog options include 1.1, 1.3, 1.5 and 1.7 mm.
Step 4: Verify the Contact-Cutting Assembly
Confirm that the torch supports the selected contact-cutting setup.
Check the correct shield, retaining cap, electrode and other front-end components.
Do not assume that a coated nozzle alone makes a standard torch suitable for drag cutting.
Step 5: Check the Compressed-Air Supply
Use compressed air that meets the requirements of the plasma cutter and torch.
Moisture, oil and contamination can negatively affect arc stability and consumable life.
Step 6: Inspect the Nozzle Before Installation
Check for:
Damaged coating
Blocked nozzle orifice
Out-of-round nozzle opening
Visible cracks
Excessive slag accumulation
Incorrect nozzle dimensions
Damaged seating surfaces
Replace worn or damaged consumables according to the operating instructions.
Common P80 Plasma Nozzle Problems and Solutions
Why Does Slag Stick to My Plasma Nozzle?
Molten metal deposits can accumulate because of cutting conditions, incorrect torch height, piercing technique or the condition of the nozzle and shield.
A coated surface may help reduce adhesion, but it cannot eliminate slag formation under every operating condition.
Why Does My P80 Nozzle Wear Out Quickly?
Possible causes include:
Excessive cutting current
Incorrect nozzle orifice
Poor compressed-air quality
Incorrect cutting distance
Frequent piercing too close to the plate
Worn electrodes
Incompatible consumable components
Inspect the complete cutting system before assuming the nozzle material is the cause.
Why Is My Plasma Cut Beveled or Uneven?
Uneven kerf geometry may result from worn consumables, incorrect torch angle, excessive travel speed, unsuitable cutting height or inconsistent gas flow.
Check nozzle wear and alignment together with the cutting parameters.
Why Does the Plasma Arc Become Unstable?
Possible causes include:
Worn electrode
Incorrect or damaged nozzle
Inconsistent air pressure
Moisture in compressed air
Poor grounding
Incorrect consumable assembly
The nozzle is one component in a complete plasma cutting system.
When Should I Replace a Coated P80 Nozzle?
Replace the nozzle when its opening becomes damaged, excessively eroded or visibly distorted.
A coating that remains intact does not necessarily mean the nozzle orifice is still within usable limits.
Inspect the nozzle and matching electrode regularly.
P80 Coated Plasma Nozzles for Wholesale and OEM Supply
INWELT supports international customers sourcing plasma cutting torches and replacement consumables.
The coated P80 nozzle range is relevant to:
Plasma cutting equipment distributors
Welding and cutting consumable wholesalers
Industrial importers
Plasma torch suppliers
CNC cutting equipment integrators
OEM brands
Maintenance and repair suppliers
Industrial metal fabrication businesses
Bulk P80 Coated Nozzle Purchasing
Customers can request quotations based on nozzle size, quantity, packaging and destination.
For repeat orders, buyers should confirm the exact nozzle type and reference code rather than specifying only “P80 nozzle.”
OEM and Private-Label Supply
INWELT welcomes inquiries for OEM and private-label supply projects.
Possible requirements include:
Customer-specific packaging
Product identification labels
Barcode labels
Distributor part numbers
Customized carton markings
Bulk packaging arrangements
Availability, minimum order quantities and customization requirements should be confirmed for each project.
Technical and Quality Documentation
Industrial buyers can specify required documentation during the quotation process.
Depending on the project, this may include:
Product dimensions
Nozzle orifice specifications
Material information
Coating information
Dimensional inspection records
Batch identification
Packaging specifications
Applicable technical documents
Any claimed coating-performance improvement should be supported by appropriate test data.
Frequently Asked Questions About P80 Coated Plasma Nozzles
What is a P80 coated contact cutting nozzle?
It is a copper-based P80 plasma cutting nozzle with a protective surface coating intended to reduce slag adhesion. It is designed for compatible contact-cutting consumable configurations.
What is the difference between a coated P80 nozzle and a standard P80 nozzle?
The main difference is the surface treatment. A coated nozzle is intended to reduce molten-slag adhesion, while a standard nozzle uses its conventional surface finish. Actual performance depends on operating conditions.
What nozzle sizes are listed for the INWELT coated P80 range?
The published product range includes 1.1 mm, 1.3 mm, 1.5 mm and 1.7 mm nozzle orifices.
Which P80 nozzle size should I use for 80A?
The published INWELT coated nozzle reference chart associates the 1.5 mm option with 80A. Confirm the complete torch assembly and equipment recommendations before use.
Can I use a 100A nozzle with an 80A P80 torch?
A nozzle series may include a 100A variant, but this does not increase an 80A torch's rated capacity. All components must be matched to a verified operating configuration.
Is a contact-cutting nozzle the same as a contact-start nozzle?
No. Contact cutting describes the cutting configuration, while contact-start refers to the arc ignition method. They are different characteristics.
Can I drag a coated P80 nozzle directly on the workpiece?
Only when the complete torch and consumable assembly is approved for the intended contact-cutting technique. The coating alone does not make direct contact safe.
Does the anti-slag coating improve nozzle life?
The coating is intended to reduce slag adhesion. Any actual increase in service life depends on cutting conditions and should be confirmed through comparative testing.
Can P80 coated plasma nozzles cut stainless steel and aluminum?
They can be used in a compatible plasma cutting system for electrically conductive metals, including steel, stainless steel and aluminum. Actual performance depends on the complete cutting setup.
Are P80 nozzles interchangeable with PT80 or IPT80 consumables?
Not automatically. Different torch series can use different front-end consumables, starting methods and retaining components. Confirm the exact torch model and part dimensions.
Does INWELT offer wholesale P80 coated plasma nozzles?
INWELT welcomes bulk purchasing inquiries from distributors, wholesalers, industrial suppliers and OEM customers.
Can I request OEM packaging for P80 plasma nozzles?
OEM and private-label packaging requests can be evaluated according to quantity, product specification and project requirements.
Request a Quote for P80 Coated Contact Cutting Nozzles
Looking for P80 coated plasma cutting nozzles for industrial distribution, equipment maintenance or OEM supply?
INWELT welcomes inquiries from professional welding and cutting equipment buyers.
For an accurate quotation, please provide:
Product Type: P80 Coated Contact Cutting Nozzle
Nozzle Orifice: 1.1 / 1.3 / 1.5 / 1.7 mm
Operating Current: Required amperage
Plasma Torch Model: Exact model or product photo
Consumable Configuration: Contact cutting or other approved arrangement
Order Quantity: Required number of pieces
Packaging: Standard, bulk or private-label requirements
Destination Country: For quotation and shipping evaluation
Technical Requirements: Any required material, dimensional or coating documentation
Contact INWELT for coated P80 plasma nozzle specifications, wholesale quotations and OEM supply inquiries.
This website uses cookies and similar technologies (“cookies”). Subject to your consent, will use analytical cookies to track which content interests you, and marketing cookies to display interest-based advertising. We use third-party providers for these measures, who may also use the data for their own purposes.
You give your consent by clicking "Accept all" or by applying your individual settings. Your data may then also be processed in third countries outside the EU, such as the US, which do not have a corresponding level of data protection and where, in particular, access by local authorities may not be effectively prevented. You can revoke your consent with immediate effect at any time. If you click on "Reject all", only strictly necessary cookies will be used.
 English
 简体中文
 العربية
 Français
 Русский
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 ភាសាខ្មែរ
 Bahasa Melayu
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Čeština
 Монгол
 қазақ
 Српски
 हिन्दी
 فارسی
 Slovenčina
 Slovenščina
 Norsk
 Svenska
 українська
 Ελληνικά
 Suomi
 Latine
 Dansk
 বাংলা
 Hrvatski
 Afrikaans
 Gaeilge
 Eesti keel
 नेपाली
 Oʻzbekcha
 latviešu
 Azərbaycan dili
 Беларуская мова
 Bosanski
 Български
 ქართული
 Lietuvių