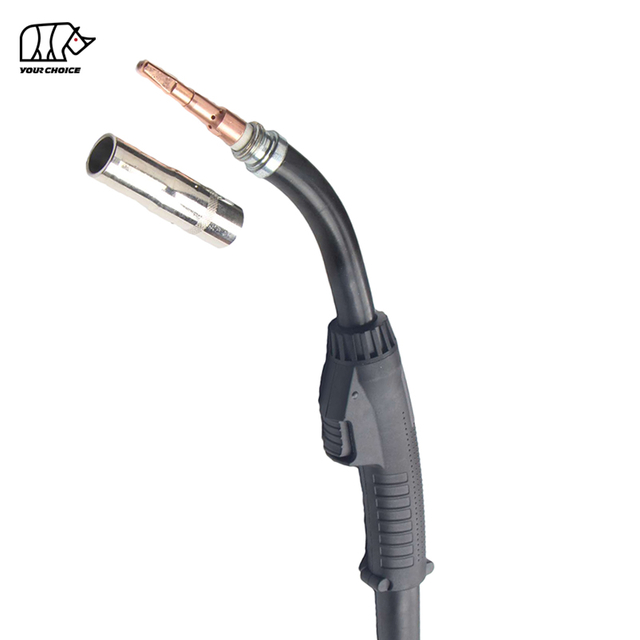
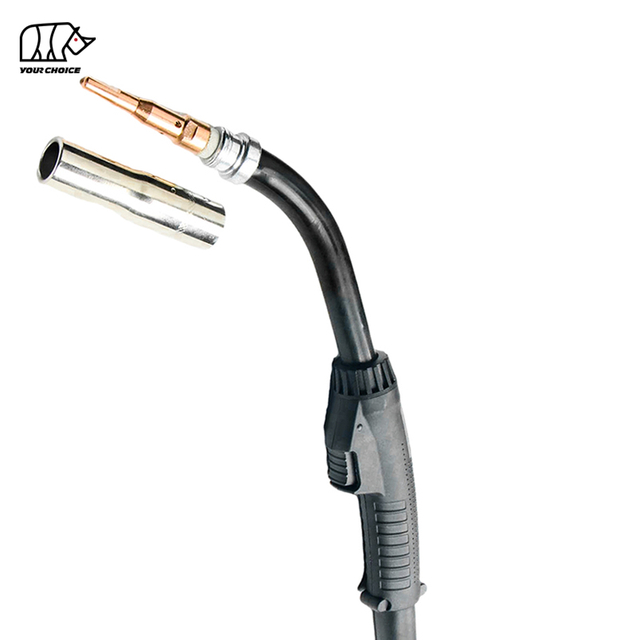
350A Air-Cooled MIG Welding Torch for Professional Fabrication
The INWELT TR300 is an air-cooled MIG/MAG welding torch designed for professional fabrication, manufacturing, maintenance and repair applications.
The current INWELT configuration is rated at 350A with CO₂ shielding gas and 200A with mixed gas at a 60% duty cycle and supports welding wire from Ø0.8 mm to Ø1.6 mm.
The TR300 uses a modular front-end system with replaceable contact tips, gas nozzles, diffuser, nozzle retainer, neck insulator and liner components. Different swan-neck angles and rear connection options allow the torch to be configured for a range of welding machines and wire feeders.
INWELT supplies TR300 assemblies with 45° and 60° neck options and connection configurations suitable for Euro, Miller, Lincoln and Tweco-style feeder interfaces.
For welding equipment manufacturers, distributors and importers, custom gun lengths, connector configurations, OEM/ODM manufacturing and private-label supply are also available.
INWELT TR300 Technical Specifications
| Specification | INWELT TR300 |
| Product Type | Air-Cooled MIG/MAG Welding Torch |
| Model | TR300 |
| Brand | INWELT |
| Cooling | Air / Gas Cooled |
| Rated Current with CO₂ | 350 A |
| Rated Current with Mixed Gas | 200 A |
| Duty Cycle | 60% |
| Wire Diameter | Ø0.8–1.6 mm |
| Welding Process | MIG / MAG |
| Neck Options | 45° / 60° |
| Gas Diffuser Thread | 1/4-20 |
| Connector Options | Euro / Miller / Lincoln / Tweco-style |
| Liner Options | According to wire size and torch length |
| Gun Length | Custom configurations available |
| OEM / ODM | Available |
| Private Label | Available |
Before ordering, confirm the welding machine or wire feeder, welding current, shielding gas, wire diameter, cable length and rear connection.
Why Choose the TR300 Air-Cooled MIG Gun?
The TR300 is designed for applications where professional welding capacity is required without the additional hoses and coolant equipment used by a water-cooled torch.
350A CO₂ Welding Capacity
The current INWELT specification rates the TR300 at:
Shielding-gas composition influences torch heat load, so CO₂ and mixed-gas ratings should be treated separately rather than presenting one universal amperage value.
Air-Cooled Construction
The TR300 is an air-cooled MIG welding gun.
It does not use an internal liquid-cooling circuit or require a separate water cooler.
This provides a simpler welding system for suitable manual MIG/MAG applications.
For applications that routinely exceed the verified TR300 current or duty-cycle rating, a higher-capacity or water-cooled torch may be more appropriate.
Ø0.8–1.6 mm Welding Wire Range
The TR300 supports wire diameters from Ø0.8 mm to Ø1.6 mm according to the selected contact tip, liner and welding configuration.
This range covers many common professional MIG/MAG fabrication applications.
45° and 60° TR300 Swan Neck Options
Torch-neck geometry affects weld access, operator posture and wire feeding.
INWELT offers two primary TR300 neck configurations.
45° Swan Neck
A 45° neck provides a relatively open torch angle and can be suitable for:
General fabrication
Flat welding
Butt joints
Long welds
Large open assemblies
60° Swan Neck
A 60° neck provides a steeper approach angle and may improve access for:
The best neck angle depends on joint geometry and operator preference rather than one angle being universally better.
Custom neck configurations can also be evaluated for qualified OEM projects.
TR300 Gas Nozzle Options for Different Weld Access Requirements
The current INWELT TR300 parts system includes several copper and brass nozzle configurations.
Available dimensions include examples such as:
3/8 in. / 9.5 mm
1/2 in. / 12.7 mm
5/8 in. / 15.9 mm
3/4 in. / 19 mm
Available geometries include:
Flush
Recessed
Stick-out configurations
Copper nozzles
Brass nozzles
Nozzle selection can affect:
A smaller nozzle can improve access, while a larger nozzle can provide broader shielding-gas coverage for suitable applications.
Always match nozzle geometry to the welding procedure and shielding-gas requirement.
TR300 Contact Tips for Ø0.8–1.6 mm MIG Wire
The contact tip transfers welding current to the continuously fed wire.
The current TR300 range includes contact-tip sizes for:
Ø0.8 mm / .030 in.
Ø0.9 mm / .035 in.
Ø1.0 mm / .040 in.
Ø1.2 mm / .045 in.
Ø1.4 mm / .052 in.
Ø1.6 mm / 1/16 in.
The contact-tip bore should match the welding wire.
A tip that is too small can increase feeding resistance or cause burnback.
A heavily worn or oversized tip can contribute to:
Replace contact tips according to actual wear rather than waiting for complete failure.
TR300 Gas Diffuser, Nozzle Retainer and Neck Insulator
The TR300 front-end assembly includes more than the contact tip and nozzle.
Gas Diffuser
The current INWELT product information lists a 1/4-20 threaded gas diffuser.
The diffuser supports the contact tip and distributes shielding gas through the torch front end.
Keep diffuser gas passages clean and replace damaged threads or heavily contaminated components.
Nozzle Retainer
The nozzle-retaining component helps hold the selected nozzle in the correct position relative to the contact tip and diffuser.
Inspect it whenever the nozzle becomes loose or difficult to install.
Neck Insulator
The neck insulator electrically separates appropriate torch components.
Damaged insulation should be replaced before the torch returns to service.
Do not continue welding with cracked or burned insulating components.
MIG Gun Liners and Wire-Feeding Performance
Consistent wire feeding is essential to stable MIG/MAG welding.
The liner guides welding wire through the cable assembly from the feeder to the torch neck.
The current TR300 page lists liner configurations including:
Additional configurations should be selected according to the actual wire diameter and torch length.
Why Correct Liner Selection Matters
A liner that is too small can create excessive wire resistance.
A liner that is too large may provide poor wire guidance.
Liner condition can affect:
Current professional Tregaskiss/Bernard platforms similarly treat wire size, liner and power-pin configuration as key ordering variables rather than secondary accessories.
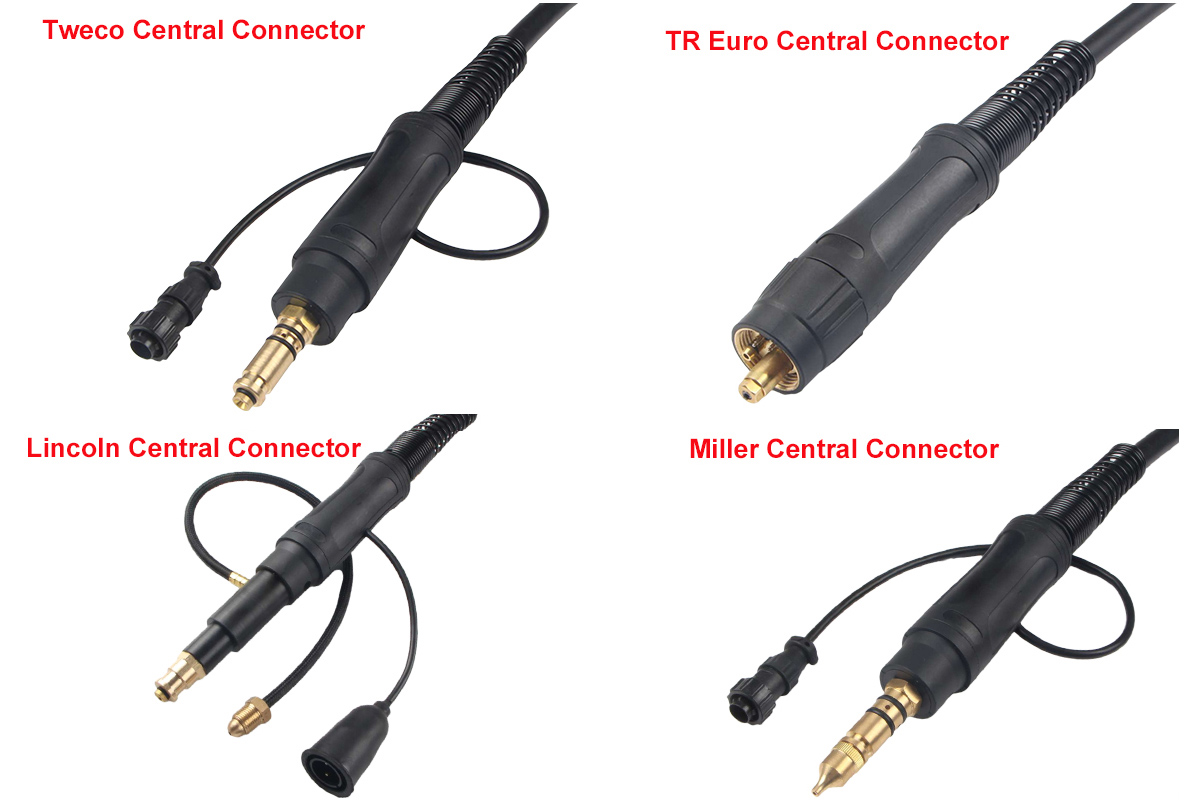
TR300 Rear Connections for Different Welding Machines
A MIG gun should not be selected only by amperage or physical appearance.
The rear connection must match the wire feeder and welding machine.
The current INWELT TR300 range includes configurations for:
Euro central connection
Miller-style connection
Lincoln-style connection
Tweco-style connection
Euro Connection
Euro central connections combine primary torch interfaces into a common connection format widely used on MIG/MAG welding systems.
Miller-Style Connection
A dedicated rear connector and control lead can be supplied for compatible Miller-type feeder interfaces.
Lincoln-Style Connection
Lincoln-style configurations use their corresponding connection and control-wire arrangement.
Tweco-Style Connection
Tweco-style rear connections are also available according to the target wire feeder.
Professional MIG gun manufacturers similarly treat the power pin and feeder model as essential compatibility criteria.
Before ordering, provide INWELT with the welding machine or wire-feeder model and photographs of the existing connection if the interface is uncertain.
Is the INWELT TR300 Compatible with Tregaskiss MIG Gun Systems?
The TR300 is designed as a Tregaskiss-style replacement MIG welding torch configuration, but complete compatibility should be verified by specification rather than brand name alone.
Check:
Gun amperage
Duty cycle
Wire diameter
Contact-tip system
Nozzle and diffuser
Neck design
Liner
Cable length
Power pin
Control lead
Wire feeder
Current genuine Tregaskiss/Bernard air-cooled products offer multiple neck, liner, consumable and feeder/power-pin combinations, demonstrating why a visually similar MIG gun is not automatically a direct replacement.
For a replacement order, provide the original gun model or part number whenever possible.
TR300 vs. Typical 300A Tregaskiss-Style MIG Guns
The TR300 should be evaluated using its own verified INWELT specifications rather than assuming every 300-series gun has identical ratings.
| Feature | INWELT TR300 | Typical 300A-Class Industrial Gun |
| Cooling | Air Cooled | Air Cooled |
| INWELT CO₂ Rating | 350 A | Varies by manufacturer |
| INWELT Mixed Gas Rating | 200 A | Varies by manufacturer |
| INWELT Duty Cycle | 60% | Manufacturer specific |
| Wire Range | Ø0.8–1.6 mm | Often up to 1.6–2.0 mm |
| Neck Options | 45° / 60° | Multiple options common |
| Connector Options | Euro / Miller / Lincoln / Tweco-style | Power-pin dependent |
| Replaceable Consumables | Yes | Yes |
Current Tregaskiss documentation lists its 300A air-cooled gun at 300A mixed gas/60%, while BTB documentation lists 300A CO₂ at 100% and 300A mixed gas at 60%.
Those are competitor specifications—not INWELT ratings.
INWELT should retain 350A CO₂ / 200A mixed gas @60% only if those values are supported by your own product testing.
How to Choose the Correct TR300 Configuration
Professional buyers should evaluate several parameters before placing an order.
1. Welding Current
Confirm the typical welding current and arc-on time.
The torch should operate within the verified rating for the shielding gas being used.
2. Shielding Gas
Specify whether the application primarily uses:
Do not use the CO₂ amperage rating as the mixed-gas rating.
3. Wire Diameter
Choose the appropriate contact tip and liner for:
0.8 mm
0.9 mm
1.0 mm
1.2 mm
1.4 mm
1.6 mm
4. Torch Neck
Choose 45° or 60° according to joint access and operator preference.
5. Cable / Gun Length
Select the shortest length that provides sufficient working reach.
Excessive cable length can add weight and wire-feeding resistance.
6. Rear Connection
Specify Euro, Miller-style, Lincoln-style, Tweco-style or another required connection.
Providing the existing feeder model or connector photo helps reduce configuration errors.
What Materials Can the TR300 MIG Torch Weld?
When connected to a suitable MIG/MAG welding system and configured with the correct wire, liner, contact tip and shielding gas, the TR300 can be used for common industrial materials including:
Material compatibility depends on the complete welding procedure rather than the torch alone.
For specialized wires or softer wire such as aluminum, confirm liner, contact-tip, feeder and cable requirements before ordering.
A standard steel liner should not automatically be used for every wire material.
Typical Applications for the TR300 MIG Welding Torch
The TR300 is suited to professional manual MIG/MAG welding where an air-cooled torch matches the required current and duty cycle.
Typical applications include:
General metal fabrication
Structural steel
Machinery manufacturing
Construction equipment
Agricultural machinery
Railway fabrication and repair
Truck and trailer manufacturing
Automotive production and repair
Industrial maintenance
General engineering
Heavy fabrication
The application name alone should not determine torch selection.
Always match the torch to actual current, duty cycle, wire diameter and welding-machine interface.
Air-Cooled vs. Water-Cooled MIG Torch
The TR300 is an air-cooled torch.
This distinction should be made very clear because the current page incorrectly contains water-cooled feature text.
Advantages of an Air-Cooled MIG Gun
An air-cooled system does not require:
This can provide:
Simpler setup
Easier maintenance
Better portability
Lower system complexity
When to Consider a Water-Cooled Torch
A water-cooled MIG torch may be more suitable when:
Welding current is continuously high
Arc-on time is very long
Production welding creates excessive torch heat
Operator heat exposure becomes uncomfortable
The duty cycle exceeds the air-cooled torch rating
Do not add water-cooling terminology to the TR300 unless there is a separate verified water-cooled version.
TR300 MIG Gun Maintenance
Regular inspection helps maintain stable wire feeding, shielding gas and electrical transfer.
Check the Contact Tip
Replace tips that are:
Heavily worn
Burned
Enlarged
Damaged by burnback
Clean the Gas Nozzle
Remove spatter regularly.
Excessive spatter accumulation can restrict shielding-gas flow and cause electrical shorting between front-end components.
Inspect the Diffuser
Check gas passages and threads.
Replace a damaged diffuser rather than overtightening the contact tip into worn threads.
Inspect the Liner
Check the liner if wire feeding becomes inconsistent.
Contamination, kinks and wear can increase feeding resistance.
Inspect the Cable Assembly
Look for:
Cuts
Abrasion
Heat damage
Severe kinks
Loose rear fittings
Gas leakage
Avoid tightly coiling the cable during welding because sharp bends can increase wire-feeding resistance.
Common TR300 MIG Welding Problems and Troubleshooting
Wire Feeds Irregularly
Check:
Drive-roll tension
Liner condition
Contact-tip size
Cable bends
Wire condition
Contact Tip Overheats
Possible causes include:
Excessive Spatter
Check:
Voltage
Wire-feed speed
Shielding gas
Contact-tip condition
Torch angle
Material cleanliness
Poor Shielding Gas Coverage
Inspect:
Gas nozzle
Nozzle spatter
Diffuser
Gas hose
Rear connection
Gas-flow setting
MIG Gun Gets Too Hot
Check:
Actual welding current
Shielding gas
Arc-on time
Duty cycle
Electrical connections
Cable condition
If the torch repeatedly overheats during normal production, a higher-capacity or water-cooled model may be more suitable.
Technical Data
| Position | Description |
| 1 | Swan Neck 45°; Swan Neck 60° |
| 2 | Torch Body Assembly |
| 3 | Handle |
| 4 | Switch |
| 5 | Switch The Trigger |
| 6 | End Fitting |
| 7 | Cone Nut |
| 8 | Cable Ball Joint & Support Spring Big |
| 9 | Cable Assembly |
| 10 | Euro Direct Plug Kit |
| 10-1 | Rear Handle |
| 10-2 | Adaptor nut |
| 10-3 | Euro Central Connector |
| 11 | Rear Handle American Brand |
| 12 | Control Wire (Tweco/Miller) |
| 12-1 | Control Wire (Lincoln) |
| 13 | Tweco Central Connector |
| 14 | Miller Central Connector |
| 15 | Lincoln Central Connector |
| 15-1 | Gas Tube |
|
|
| A | Nozzle 3/8″ 9.5mm Flush Copper |
| Nozzle 1/2″ 12.7mm 1/8″ Recess Copper |
| Nozzle 5/8” 15.9mm 1/8” Recess Copper |
| Nozzle 3/4” 19mm 1/8″ Recess Copper |
| Nozzle 5/8” 15.9mm 1/8” Stick Out Brass |
| Nozzle 5/8” 15.9mm 1/4” Stick Out Copper |
| Nozzle 1/2” 12.7mm 1/4” Stick Out Brass |
| Nozzle 1/2” 12.7mm 1/8” Stick Out Brass |
| Nozzle 1/2″ 12.7mm 1/8” Recess Brass |
| Nozzle 3/8″ 9.5mm 1/16” Recess Brass |
| B | Contact Tip .230” 0.6mm |
| Contact Tip .030” 0.8mm |
| Contact Tip .035” 0.9mm |
| Contact Tip .040” 1.0mm |
| Contact Tip .045” 1.2mm |
| Contact Tip .052” 1.4mm |
| Contact Tip 1/16” 1.6mm |
| C | Gas Diffuser (1/4-20Thd) |
| D | Nozzle Retainer |
| E | Neck Insulator |
| F | Liner for .035″-.045″(0.9-1.2mm) 10FT(3.0m) |
| Liner for .035″-.045″(0.9-1.2mm) 15FT(4.6m) |
|
|
| Technical Data | Rating: 350A CO2/200A Mixed Gases |
| Duty Cycle: 60% |
| Wire Size: .030”-1/16”(0.8-1.6mm) |
| Type | TR300 MIG GUN Miller Connector |
| TR300 MIG GUN Tweco Connector |
| TR300 MIG GUN Lincoln Connector |
| TR300 MIG GUN Euro Connector |

Our Catalog:
 INWELT MIG WELDING TORCH.pdf
TR300 Consumables for Distributor and Aftermarket Supply
For welding distributors, the installed MIG gun creates ongoing demand for replacement consumables.
A complete TR300 supply program can include:
Providing both the complete gun and replacement parts allows distributors to support customers throughout the service life of the torch.
It also creates a clearer aftermarket product program than selling the complete TR300 gun alone.
OEM Tregaskiss-Style MIG Gun Manufacturing by INWELT
INWELT supplies MIG/MAG welding torches and replacement parts to professional B2B customers including:
Welding equipment manufacturers
Welding machine brands
Importers
Distributors
Wholesalers
Industrial supply companies
Welding repair businesses
Private-label brands
OEM and ODM configurations can be evaluated according to machine interface and target-market requirements.
OEM and Private-Label Options
Customization may include:
For OEM projects, provide the wire feeder model, required current, shielding gas, wire diameter, connector and estimated purchasing volume.
Why Source TR300 MIG Guns from INWELT?
INWELT manufactures multiple professional MIG torch platforms and corresponding replacement components.
For distributors and equipment brands, sourcing complete TR300 guns together with consumables can simplify:
The TR300 range also provides multiple connection systems and front-end options, allowing one product family to support several welding-machine interfaces.
Frequently Asked Questions About the TR300 MIG Welding Torch
Is the TR300 MIG welding torch air cooled?
Yes.
The INWELT TR300 on this page is an air-cooled MIG/MAG welding torch.
It does not require an external water-cooling system.
What is the amperage rating of the INWELT TR300?
The current INWELT specification lists:
350A with CO₂
and
200A with mixed shielding gas
at a 60% duty cycle.
These values should be used only if confirmed by INWELT product testing.
Why is the mixed-gas rating lower than the CO₂ rating?
Different shielding gases influence heat transfer and torch temperature differently.
For this reason, MIG gun manufacturers often publish separate CO₂ and mixed-gas duty-cycle ratings.
What wire sizes does the TR300 support?
The INWELT TR300 supports welding wire from Ø0.8 mm to Ø1.6 mm.
The contact tip and liner should match the wire diameter.
What neck angles are available?
Current INWELT configurations include 45° and 60° swan necks.
What connector options are available?
The current product system includes:
Euro
Miller-style
Lincoln-style
Tweco-style
Machine compatibility should be confirmed before ordering.
Is the TR300 compatible with Tregaskiss consumables?
The TR300 is designed in a Tregaskiss-style configuration, but consumable compatibility should be confirmed by part dimensions and specifications rather than product appearance alone.
Provide the existing part number where possible.
Is TR300 a genuine Tregaskiss product?
No.
INWELT TR300 is an INWELT-manufactured replacement/style product and should not be represented as a genuine Tregaskiss-manufactured gun.
Tregaskiss and related product names are trademarks of their respective owners.
Can the TR300 weld stainless steel?
Yes, when the complete MIG/MAG system is configured with appropriate stainless-steel wire, shielding gas, liner and welding parameters.
Can the TR300 weld aluminum?
Potentially, but soft aluminum wire requires the correct liner, feeder, contact tip and cable configuration.
Confirm the application with INWELT before ordering a standard TR300 for aluminum wire.
What is the difference between TR300 and a water-cooled MIG gun?
TR300 is air cooled and does not require a coolant circulation system.
A water-cooled gun is generally better suited to prolonged high-current production where thermal load exceeds the capacity of an air-cooled torch.
How often should the contact tip be replaced?
There is no universal replacement interval.
Replace the contact tip according to wear, electrical contact, wire feeding and arc stability.
Does INWELT offer custom TR300 gun lengths?
Yes.
The current INWELT product information states that custom gun lengths are available.
Does INWELT manufacture OEM TR300 MIG guns?
Yes.
OEM/ODM and private-label configurations are available for qualified equipment manufacturers, welding brands, distributors, importers and wholesalers.
Request a Quote for the INWELT TR300 MIG Welding Torch
Looking for a Tregaskiss-style air-cooled MIG gun, replacement TR300 assembly, compatible consumables or an OEM MIG torch manufacturer?
For faster technical confirmation, provide:
Welding machine or wire-feeder brand and model
Required welding current
CO₂ or mixed shielding gas
Wire diameter
Required gun length
45° or 60° neck
Rear connector type
Contact-tip requirement
Consumable requirements
Estimated order quantity
INWELT or private-label branding
INWELT can then confirm the appropriate TR300 configuration for your MIG/MAG welding system.
 English
 简体中文
 العربية
 Français
 Русский
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 ភាសាខ្មែរ
 Bahasa Melayu
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Čeština
 Монгол
 қазақ
 Српски
 हिन्दी
 فارسی
 Slovenčina
 Slovenščina
 Norsk
 Svenska
 українська
 Ελληνικά
 Suomi
 Latine
 Dansk
 বাংলা
 Hrvatski
 Afrikaans
 Gaeilge
 Eesti keel
 नेपाली
 Oʻzbekcha
 latviešu
 Azərbaycan dili
 Беларуская мова
 Bosanski
 Български
 ქართული
 Lietuvių