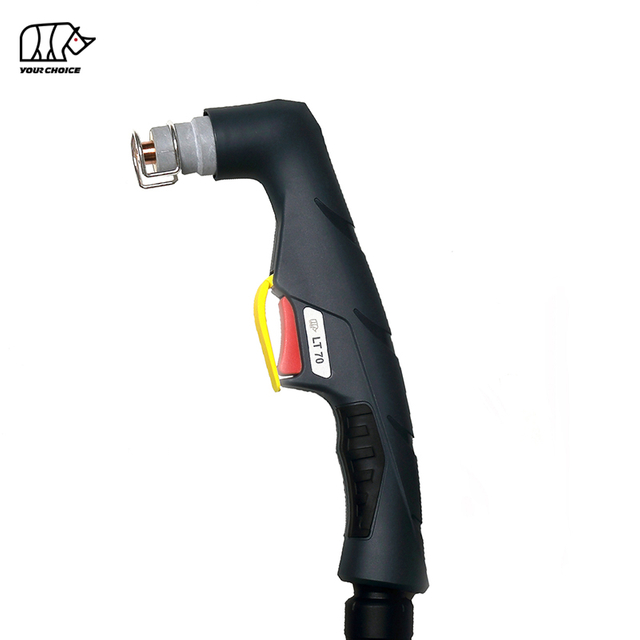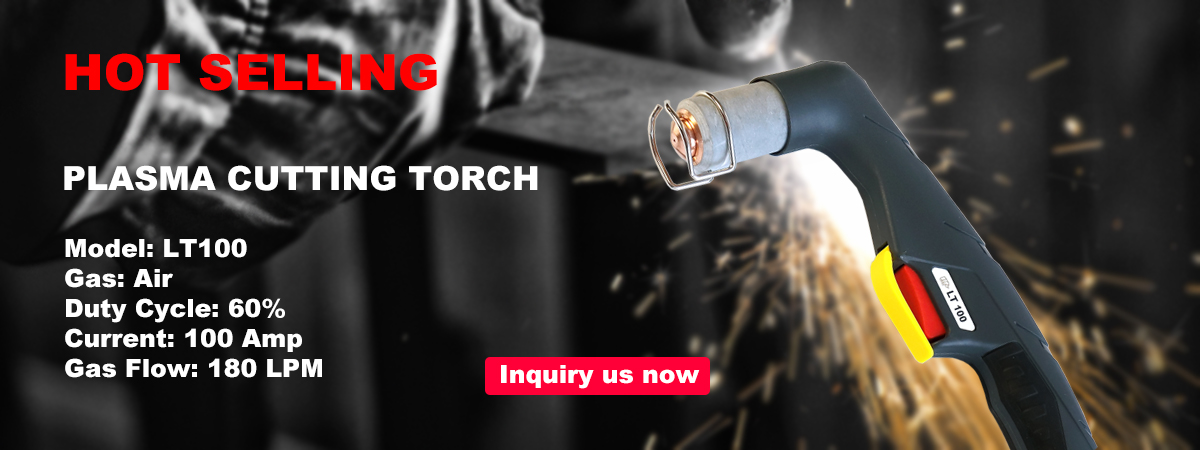
100A HF Manual Plasma Cutting Torch for Professional Metal Cutting
The INWELT LT100 is an air-cooled manual plasma cutting torch designed for professional metal fabrication, maintenance, repair and industrial cutting applications.
The LT100 is rated at 100A with a 60% duty cycle and uses a high-frequency (HF) arc-starting system.
The current INWELT configuration includes:
100A rated current
60% duty cycle
Compressed-air operation
HF arc starting
Approx. 4.5–5.0 bar operating pressure
Approx. 180 L/min airflow
Approx. 100-second recommended post-flow
Standard 6 m torch lead
Multiple rear-connection options are available, including 1/8G, 1/4G, M14×1, M16×1.5 and central-adapter configurations.
The LT100 should be positioned specifically as a manual / handheld plasma cutting torch. For fixed CNC and mechanized applications, use the corresponding INWELT machine-torch model.
INWELT LT100 Technical Specifications
| Specification | INWELT LT100 |
| Product Type | Manual / Handheld Plasma Cutting Torch |
| Model | LT100 |
| Brand | INWELT |
| Rated Current | 100 A |
| Duty Cycle | 60% |
| Cooling | Air |
| Process Gas | Compressed Air |
| Arc Starting | HF |
| Gas Pressure | Approx. 4.5–5.0 bar |
| Gas Flow | Approx. 180 L/min |
| Recommended Post-Flow | Approx. 100 seconds |
| Standard Lead Length | 6 m |
| Operation | Manual / Handheld |
| Connector Options | 1/8G / 1/4G / M14×1 / M16×1.5 / Central Adapter |
| Standard Tip Family | Ø1.1 / Ø1.4 / Ø1.7 mm |
| Extended Consumables | Available |
| OEM / ODM | Available |
| Private Label | Available |
Before ordering, confirm the plasma power source, output current, HF starting architecture, power/gas connector, pilot-arc connection and trigger wiring.
LT100 vs. LTM100: Manual Torch vs. Machine Torch
LT100 and LTM100 belong to the same broader plasma torch family but should be treated as separate complete products.
| Feature | LT100 | LTM100 |
| Operation | Manual / Handheld | CNC / Mechanized |
| Torch Geometry | Handheld torch | Straight machine torch |
| Start Control | Operator trigger | Machine controlled |
| Mounting | Handheld | Fixed torch holder |
| Torch Height | Operator controlled | CNC / THC controlled |
| Main Application | Manual cutting | Automated cutting |
Some consumables may be shared between related torch families.
However, complete torch heads, handles, machine bodies and cable assemblies should not automatically be treated as interchangeable.
For website internal links, use clear anchor text such as:
LT100 Manual Plasma Cutting Torch
and
LTM100 CNC Plasma Cutting Torch
rather than describing both products simply as LT100.
How the LT100 HF Plasma Cutting Torch Works
The LT100 works as part of a complete plasma cutting system consisting of the plasma power source, torch, compressed-air supply and work connection.
Compressed air passes through the torch head, diffuser, electrode and cutting nozzle.
Electrical energy ionizes the gas and forms a high-temperature plasma arc.
The cutting nozzle constricts this arc into a concentrated plasma jet that melts electrically conductive metal while high-velocity air removes molten material from the kerf.
High-Frequency Arc Starting
The LT100 uses HF ignition.
A high-frequency electrical signal helps establish the initial plasma arc without requiring the cutting nozzle to mechanically strike the workpiece.
The plasma power source must therefore support a compatible HF starting system.
HF, non-HF and back-striking plasma torches should not be treated as automatically interchangeable.
Why Choose the LT100 for 100A Manual Plasma Cutting?
The LT100 is designed for professional manual cutting applications requiring more current capacity than lower-output LT50 and LT70 platforms.
100A Rated Current
The LT100 is rated at 100A.
The torch should be paired with a compatible plasma power source and operated within its verified current range.
60% Duty Cycle
The current specification lists a 60% duty cycle at 100A.
Actual thermal load can also be influenced by:
Operating current
Ambient temperature
Arc-on time
Airflow
Number of starts
Consumable condition
Do not operate the torch above its verified rating simply because the plasma power source can provide more current.
Air-Cooled Construction
The LT100 does not require a separate liquid-cooling circuit.
Compressed air functions as the process gas and also contributes to heat removal from the torch front end.
6 m Standard Lead
The standard 6 m torch lead provides practical working reach for fabrication shops, industrial maintenance and repair applications.
LT100 Connection Options
The LT100 platform is available with several rear-connection configurations.
Current options include:
1/8G
1/4G
M14×1
M16×1.5
Central Adapter
These options allow distributors and equipment manufacturers to support different plasma power-source interfaces.
A connector that physically fits does not automatically confirm electrical compatibility.
The complete torch interface must be checked.
How to Check LT100 Plasma Cutter Compatibility
Do not select a replacement LT100 only because the plasma cutter is rated at approximately 100A.
Confirm HF Starting
The plasma power source must support an HF torch system.
Confirm Rated Current
The LT100 is rated at 100A.
The power source and consumables should be operated within the verified torch range.
Confirm the Power and Gas Connection
Check whether the machine requires:
1/8G
1/4G
M14×1
M16×1.5
Central adapter
Confirm the Pilot-Arc Connection
Different plasma cutters may use different pilot-arc arrangements even when the main torch connection appears similar.
Confirm Trigger Wiring
The trigger/control circuit must match the plasma power source.
Information to Provide for Compatibility Confirmation
For replacement orders, provide:
This is more reliable than selecting the torch by amperage or connector appearance alone.
LT100 Standard Cutting Tips
The LT100 consumable platform includes several standard cutting-tip diameters.
Ø1.1 mm Cutting Tip
INWELT Code: IJWV0617-11
Reference: PD0101-11
Ø1.4 mm Cutting Tip
INWELT Code: IJWV0617-14
Reference: PD0101-14
Ø1.7 mm Cutting Tip
INWELT Code: IJWV0617-17
Reference: PD0101-17
Different nozzle diameters are intended for different operating conditions.
The correct tip should be selected according to:
Cutting current
Plasma power source
Material
Front-end configuration
Required cutting process
Do not select a nozzle only because it physically fits the torch head.
Which Cutting Tip Should Be Used at 100A?
The current LT100 consumable family includes Ø1.1 mm, Ø1.4 mm and Ø1.7 mm cutting tips.
Comparable 100A HF torch platforms commonly associate an intermediate nozzle size with approximately 100A operation.
However, INWELT should publish a final amperage-to-nozzle chart only after confirming its own engineering and cutting-test data.
The strongest future consumable table should show:
| INWELT Code | Tip Diameter | Recommended Current | Electrode | Shield / Retainer | Process |
| Verified Code | Verified Size | Verified Current | Matching Part | Matching Part | Cutting Mode |
This provides more useful first-party information than generic statements such as “multiple nozzle sizes available.”
LT100 Extended Cutting Tips
The LT100-related consumable family also includes extended cutting tips.
Current parts include:
IJWV0673-14 / PD0117-14 – Extended Tip Ø1.4 mm
IJWV0673-17 / PD0117-17 – Extended Tip Ø1.7 mm
The wider family also includes an extended 50A tip configuration.
Extended tips can provide additional access where a standard-length consumable cannot easily reach the cutting area.
Use extended tips only with the corresponding electrode and front-end consumables.
LT100 Standard Electrode
The standard electrode is:
INWELT Code: IJWC0617
Reference: PR0101
The electrode transfers electrical energy through the torch and gradually wears during repeated arc starts and cutting.
Replace the electrode before excessive center wear causes:
Difficult arc starting
Unstable plasma arc
Accelerated nozzle wear
Inconsistent cutting
Do not grind or modify a worn electrode to extend its service life.
LT100 Extended Electrode
The extended electrode is:
INWELT Code: IJWC0672
Reference: PR0116
This component is intended for compatible extended-tip configurations.
Do not mix a standard electrode and extended cutting tip unless the combination has been technically verified.
LT100 Gas Diffuser
The current gas diffuser is:
INWELT Code: IJWG0617
Reference: PE0101
The diffuser controls process-gas distribution around the electrode and cutting nozzle.
Correct airflow helps maintain:
Arc stability
Consumable cooling
Plasma-jet shape
Cutting consistency
Replace the diffuser if it becomes cracked, distorted, burned or heavily contaminated.
LT100 Outside Nozzle and Retaining Components
The LT100 consumable family includes:
IJWT0677 / PC0111 – Outside Nozzle
and
IJWT0691 / PC0130 – Contact Nozzle Retaining Cap
These components help protect and position the internal consumable stack.
Replace front-end components if they show:
LT100 Stand-Off and Contact-Cutting Accessories
The LT100 platform includes several front-end positioning accessories.
Current parts include:
IJTN0069 / CV0014 – Four-Point Spacer
IJTN0078 / CV0012 – Double-Point Spacer
IJTN0077 / CV0011 – Spacer Spring
IJTN0089 / CV0023 – Contact-Cutting Spacer
Stand-Off Cutting
Stand-off accessories help maintain a controlled distance between the cutting nozzle and the workpiece.
Correct stand-off can help protect consumables and maintain plasma-arc geometry.
Contact Cutting
Contact-cutting components use a different front-end relationship with the workpiece.
Do not drag an exposed standard cutting nozzle directly across the material unless the specific consumable configuration is designed for contact cutting.
LT100 Torch Head and Hand-Control Components
The LT100 manual torch system includes serviceable torch-head and handle components.
Current parts include:
IJWA0606 – Plasma Torch Head
IJGU0697 / EA0131 – Silicone O-Ring
IJHW0046 – Manual Plasma Handle
IJIK0733 – Trigger Protection Component
IJIR0081 – Trigger
IJIK0805 – Handle Joint
These replaceable components allow distributors and repair companies to service the torch without replacing the complete assembly every time a single component is damaged.
LT100 Cable Assembly Options
The LT100 manual-torch family includes dedicated cable assemblies.
Current examples include:
IJWO00210077-00 – LT100/LT101 / 10 mm² / 6 m / 1/8G
IJWO00210071-00 – LT100/LT101 / 10 mm² / 6 m / Central Adapter
Machine-torch cable assemblies should be presented on the corresponding LTM product page rather than mixed into the primary LT100 manual-torch table.
This keeps the LT100 product entity clear for both professional buyers and search engines.
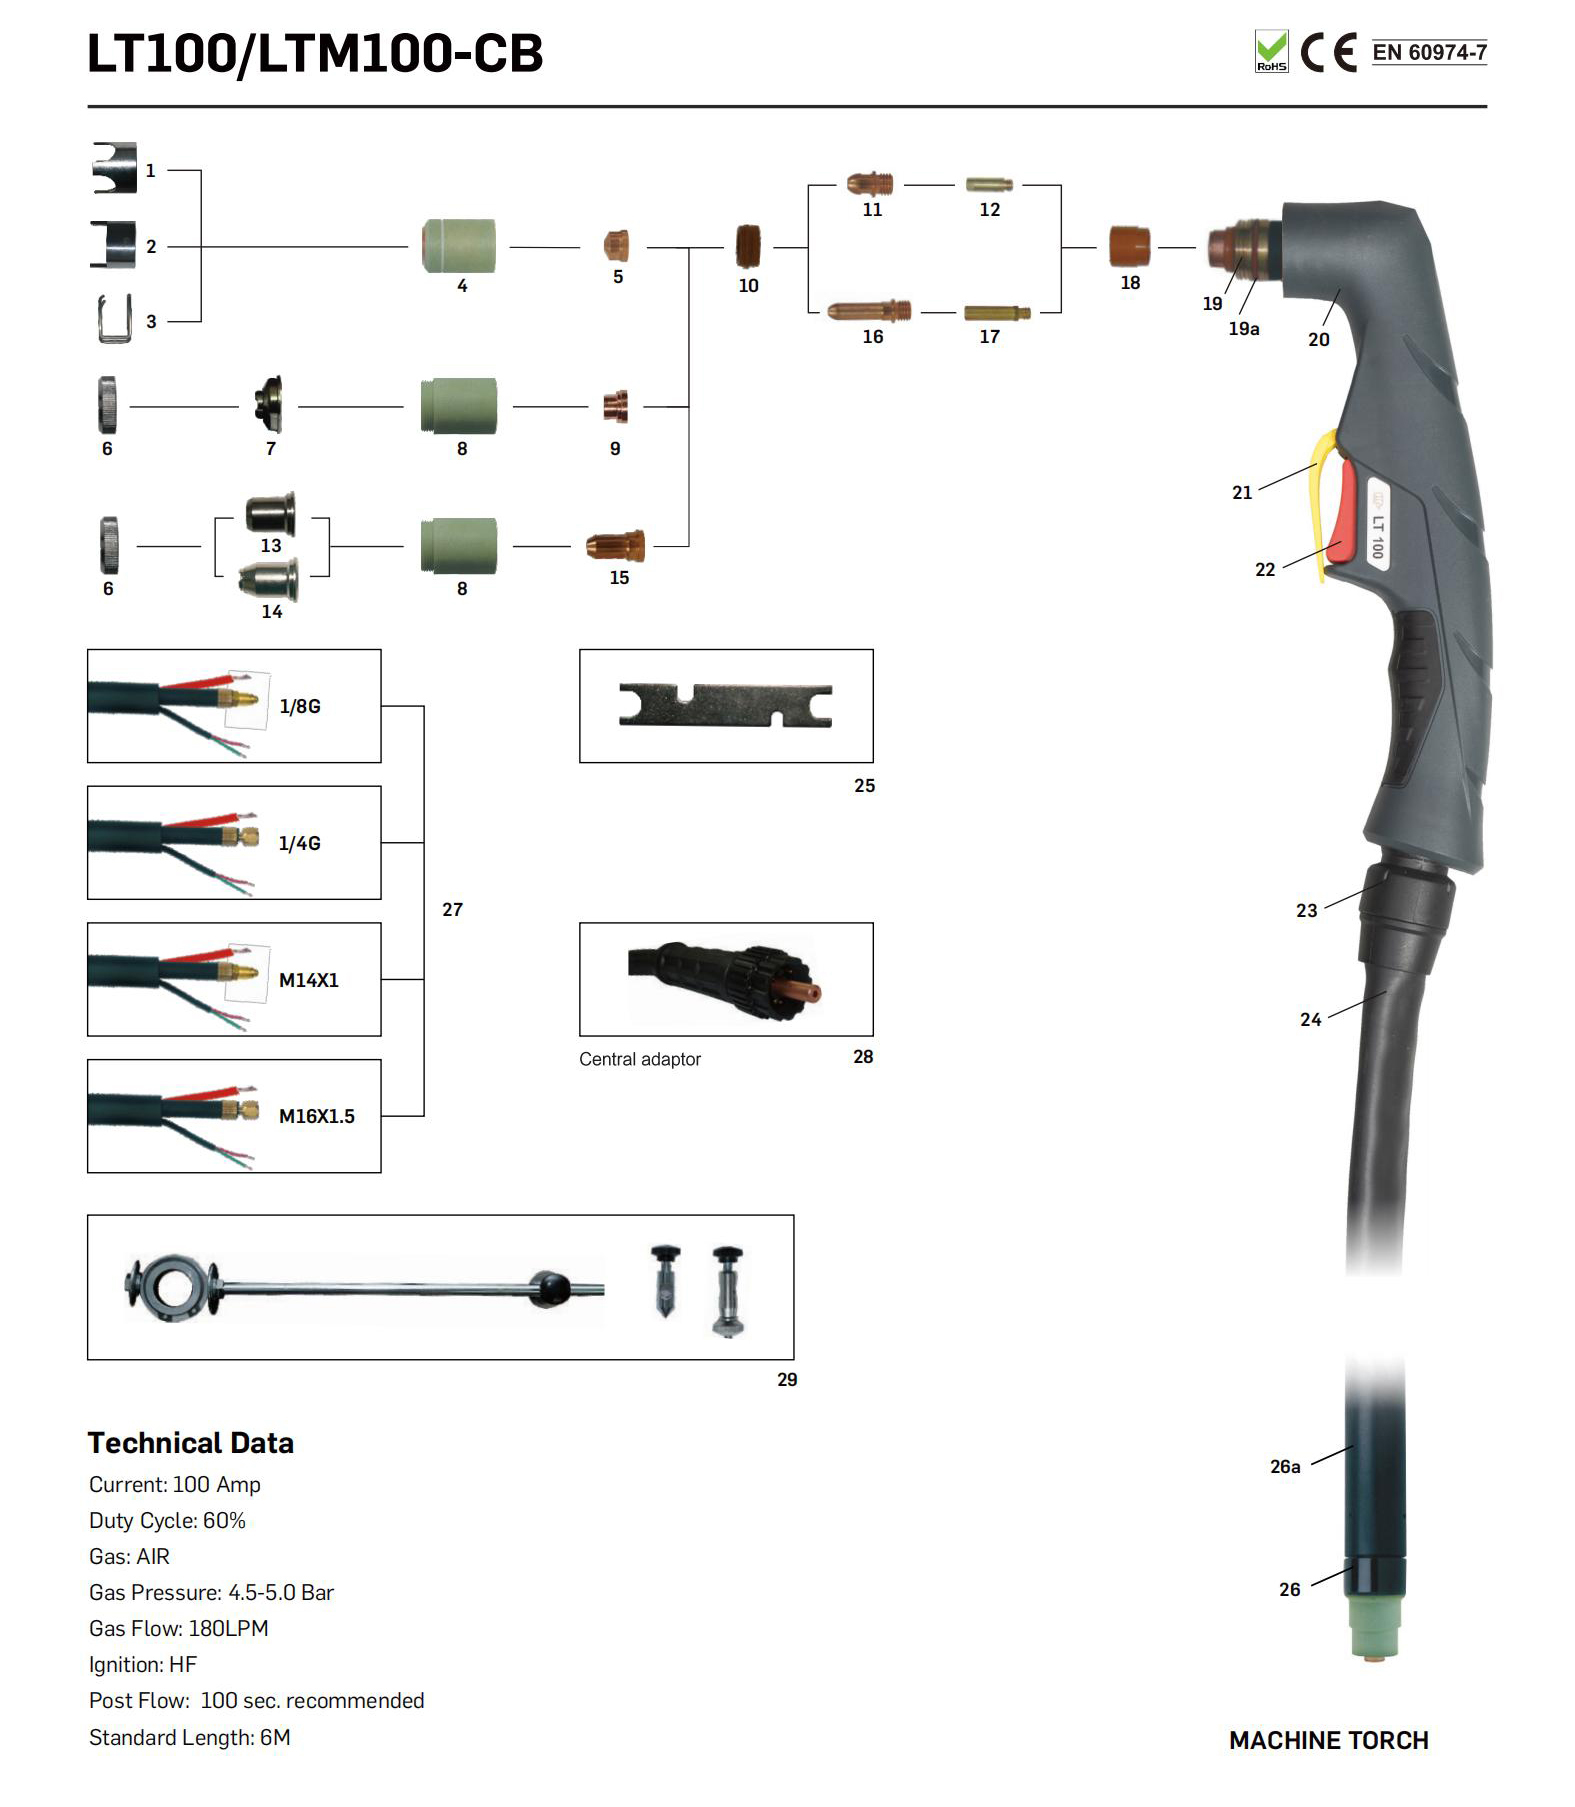
Spare Parts Details:
| HAND TORCH |
| Code | Ref. | Description |
| IJWU6961 | PA1450 | Plasma cutting torch LT100/6m 1/8G |
| IJWU6967 |
| Plasma cutting torch LT100/6m 1/4G |
| IJWU6968 | PA1452 | Plasma cutting torch LT100/6m M14×1 |
| IJWU6969 |
| Plasma cutting torch LT100/6m M16×1.5 |
| IJWU6960 |
| Plasma cutting torch LT100/6m central adaptor |
| Machine | Torch |
|
| Code | Ref. | Description |
| IJWU0671 | PA0110 | Plasma cutting auto torch LTM100/6m 1/8G |
| IJWU0677 | PA0111 | Plasma cutting auto torch LTM100/6m M14×1 |
| IJWU0692 |
| Plasma cutting auto torch LTM100/6m M16×1.5 |
| IJWU0693 |
| Plasma cutting auto torch LTM100/6m central adaptor |
| IJWU0694 |
| Plasma cutting auto torch LTM100/6m 1/4G |
|
| Position | Code | Ref. | Description |
| 1 | IJTN0069 | CV0014 | Four point edspacer/LT100-150 |
| 2 | IJTN0078 | CV0012 | Double point edspacer/LT100-150 |
| 3 | IJTN0077 | CV0011 | Spacer spring LT100-150 |
| 4 | IJWT0677 | PC0111 | Outside nozzle LT101 |
| 5 | IJTN0095 | CV0039 | Four point crown shield with insulator/LT101-141 |
| 6 | IJTN0089 | CV0023 | Spacer for contact cutting/LT101-141 |
| 7 | IJWT0691 | PC0130 | Contact nozzle retaining cap/LT101 |
| 8 |
|
| Tip |
| 8.1 | IJWV0617-11 | PD0101-11 | Tip Φ1.1mm LT101-141 |
| 8.2 | IJWV0617-14 | PD0101-14 | Tip Φ1.4mm LT101-141 |
| 8.3 | IJWV0617-17 | PD0101-17 | Tip Φ1.7mm LT101-141 |
| 9 | IJWG0617 | PE0101 | Diffuser LT101-141 |
| 10 | IJWC0617 | PR0101 | Electrode Plasma LT101-141 |
| 11 | IJAO0770 |
| Airtube/LT100-101 |
| 12 | IJTN0000 |
| Locking nut |
| 13 | IJTN0014 | CV0008 | Contact cutting attachment/LT101-151 |
| 14 | IJTN0015 | CV0009 | Long contact cutting attachment/LT101-151 |
| 15 |
|
| Tip |
| 15.1 | IJWV0673-14 | PD0117-14 | Extended tip Φ1.4mm/LT101-151 |
| 15.2 | IJWV0673-17 | PD0117-17 | Extended tip Φ1.7mm/LT101-151 |
| 15.3 | IJWV0677 |
| Extended tip 50A/LT101-151 |
| 16 | IJWC0672 | PR0116 | Extended electrode Plasma LT101 |
| 17 | IJWA0606 |
| Plasma torch head LT101 |
| 17a | IJGU0697 | EA0131 | “O”ring Φ18.77x1.78mm in silicon |
| 17b | IJWG9017 |
| Frontin sulator/LT101 |
| 18 | IJHW0046 |
| Plasma hand lemanual/ASeries/Red |
| 19 | IJIK0733 |
| Protection part/Plasma/Yellow |
| 20 | IJIR0081 | 185.0031 | Trigger |
| 21 | IJIK0805 |
| Joint/big/new type |
| 22 |
|
| Cable assembly |
| 22.1 | IJWO00210077-00 |
| Cable assembly/LT100-101/10MMQ/6MATT.1/8G |
| 22.2 | IJWO00210071-00 |
| Cable assembly/LT100-101/10MMQ/6M central adaptor |
| 22.3 | IJWO10210077-00 |
| Cable assembly/LTM100-101/10MMQ/6MATT.1/8G |
| 22.4 | IJWO10210071-00 |
| Cable assembly/LTM100-101/10MMQ/6M central adaptor |
| 22.5 | IJWO0642 |
| Cable assembly/LT100-101/6M/central adaptor |
| 23 | IJDH6017 |
| Spanner for Plasma |
| 24 | IJWA0676 |
| Plasma torch head LTM101 |
| 24a | IJHW0024 | W0300144 | Fiber glass position tube/LTM |
| 25 |
|
| Cable assembly LTM |
| 25.1 | IJAU5698 |
| Connecting adaptor 1/8G-1/4G |
| 25.2 | IJAU5697 |
| Connecting adaptor 1/8G-3/8G |
| 25.3 | IJAU5699 |
| Connecting adaptor 1/8G-M14×1 |
| 25.4 | IJAU5690 |
| Connecting adaptor 1/8G-M16×1.5 |
| 26 IJAY0089 FY0023 Central adaptor torch side Plasma 5pins |
| 27 IJTN0088 CV0022 Circle cutting attachment/LT100-151 |
Our Catalog:
 INWELT PLASMA TORCH CATALOG.pdf
What Metals Can the LT100 Plasma Torch Cut?
When paired with a compatible plasma cutting power source, the LT100 can be used to cut electrically conductive metals such as:
Mild steel
Carbon steel
Stainless steel
Aluminum
Copper
Brass
Galvanized steel
Actual cutting speed, edge quality and practical thickness vary according to the complete plasma system.
How Thick Can a 100A LT100 Plasma Torch Cut?
The plasma torch alone does not determine one universal maximum cutting thickness.
Actual cutting capacity depends on:
Plasma power source
Input power
Material
Actual cutting current
Cutting-tip diameter
Air pressure
Airflow
Travel speed
Torch-to-work distance
Consumable condition
Required edge quality
Professional plasma specifications normally distinguish between three different performance levels.
Recommended Cutting Capacity
Material thickness that can be cut productively with suitable speed and edge quality.
Maximum Cutting Capacity
Thicker material that can still be cut at reduced speed.
Severance Capacity
The maximum thickness that can be separated, normally with lower edge quality.
Specific LT100 thickness figures should therefore be published only when supported by an INWELT complete-system cutting test.
Build an INWELT LT100 Cutting Chart
A first-party LT100 cutting chart would be one of the strongest technical and GEO additions to this product page.
Recommended fields include:
| Parameter | Data to Publish |
| Material | Mild Steel / Stainless Steel / Aluminum |
| Thickness | Tested thickness |
| Current | Actual tested current |
| Tip Code | INWELT part number |
| Tip Diameter | mm |
| Air Pressure | bar |
| Air Flow | L/min |
| Travel Speed | mm/min |
| Torch Stand-Off | mm |
| Cut Result | Recommended / Maximum / Severance |
Use measured INWELT test results rather than copying another manufacturer's cutting data.
Recommended Air Supply for the LT100
The current INWELT LT100 specification uses compressed air.
Recommended operating data includes:
Gas: Compressed Air
Gas Pressure: Approx. 4.5–5.0 bar
Gas Flow: Approx. 180 L/min
Recommended Post-Flow: Approx. 100 seconds
Use Clean and Dry Compressed Air
Moisture, compressor oil and particles can negatively affect:
Arc stability
Electrode life
Cutting-tip life
Cut consistency
Use appropriate filtration and moisture separation.
Check Pressure While Air Is Flowing
Static regulator pressure may differ from the pressure available during cutting.
Filters, regulators, fittings and long air hoses can create pressure loss.
Set the air supply according to the complete plasma system's operating procedure.
Typical Applications for the LT100 Manual Plasma Torch
The LT100 is designed for professional manual plasma cutting applications including:
The correct torch should be selected according to the plasma power source and cutting requirement rather than application name alone.
LT100 Maintenance and Consumable Inspection
Inspect the Electrode
Check the electrode regularly for excessive center wear.
Replace it before severe erosion causes poor starting or damages the cutting nozzle.
Inspect the Cutting Tip
Check for:
Enlarged nozzle opening
Oval orifice
Burn damage
Heavy contamination
A damaged nozzle can contribute to unstable cutting and excessive bevel.
Inspect the Diffuser
Keep gas passages clean.
Replace cracked or heat-damaged components.
Inspect the Outside Nozzle
Do not operate the torch with severely cracked or damaged insulating parts.
Inspect O-Rings
Replace hardened, cut or damaged seals if gas leakage occurs.
Inspect the Torch Cable
Check for:
Abrasion
Cuts
Heat damage
Tight bends
Loose connections
Common LT100 Plasma Cutting Problems
Difficult HF Arc Starting
Check:
Electrode condition
Cutting tip
HF starting circuit
Air pressure
Work connection
Torch connector
Excessive Dross
Check:
Travel speed
Cutting current
Material thickness
Torch stand-off
Airflow
Consumable condition
Angled Cut
Possible causes include:
Worn nozzle
Incorrect torch angle
Damaged diffuser
Disturbed gas flow
Incorrect travel speed
Short Consumable Life
Check:
Compressed-air quality
Tip/current matching
Torch stand-off
Number of arc starts
Electrode wear
Torch Overheating
Possible causes include:
Stop cutting and identify the cause before continuing.
LT100 Consumables for Distributor and Aftermarket Supply
A complete LT100 aftermarket program can include:
For distributors, supplying the complete torch together with replacement consumables creates a more complete aftermarket product program.
Exact INWELT part numbers also help reduce replacement and ordering errors.
OEM LT100 Plasma Cutting Torch Manufacturing by INWELT
INWELT supplies plasma cutting torches and replacement consumables to professional B2B customers including:
Plasma cutter manufacturers
Welding and cutting equipment brands
Importers
Distributors
Wholesalers
Industrial suppliers
Repair companies
Aftermarket consumable brands
OEM and ODM projects can be evaluated according to the plasma power-source interface and target-market requirements.
OEM and Private-Label Options
Customization may include:
Customer branding
Handle marking
Product labels
Torch cable configurations
1/8G connection
1/4G connection
M14×1 connection
M16×1.5 connection
Central adapter
Consumable kits
Private-label packaging
Instructions and technical labels
Barcode and carton requirements
For OEM projects, provide the plasma cutter specification, HF starting method, connector requirements and estimated order quantity.
Why Source LT100 Torches and Consumables from INWELT?
The LT100 platform supports both complete manual torch assemblies and replacement consumables.
The product system includes:
Multiple complete-torch connector configurations
Ø1.1 / Ø1.4 / Ø1.7 mm cutting tips
Extended cutting tips
Standard and extended electrodes
Gas diffuser
Outside nozzle
Retaining components
Contact-cutting accessories
Torch head
Handle and trigger components
Cable assemblies
Connection adapters
For equipment brands, distributors and importers, sourcing complete torches and spare parts from the same supply program can simplify purchasing and aftermarket support.
Frequently Asked Questions About the LT100 Plasma Cutting Torch
What amperage is the INWELT LT100?
The LT100 is rated at 100A according to the current INWELT technical specification.
What is the LT100 duty cycle?
The current specification lists a 60% duty cycle.
Does the LT100 use HF ignition?
Yes.
The LT100 uses high-frequency arc starting.
Is the LT100 a hand torch or a machine torch?
The LT100 is a manual / handheld plasma cutting torch.
The related LTM-series model should be used for CNC or mechanized cutting.
What gas does the LT100 use?
The current configuration uses compressed air.
What air pressure does the LT100 require?
Approximately 4.5–5.0 bar.
What airflow does the LT100 require?
The current INWELT specification lists approximately 180 L/min.
What post-flow time is recommended?
Approximately 100 seconds.
What torch lead length is standard?
The standard LT100 lead is 6 m.
What connector options are available?
Current configurations include:
1/8G
1/4G
M14×1
M16×1.5
Central adapter
What cutting-tip sizes are available?
The current consumable family includes:
Extended tip configurations are also available.
Which electrode does the LT100 use?
The standard electrode is:
IJWC0617 / PR0101
The extended electrode is:
IJWC0672 / PR0116
Is the LT100 compatible with every 100A plasma cutter?
No.
The HF starting architecture, main connector, pilot-arc connection, trigger wiring and air requirements must also match.
Can the LT100 cut stainless steel?
Yes, when used with a compatible plasma power source and suitable operating parameters.
Can the LT100 cut aluminum?
Yes.
Aluminum is electrically conductive and can be plasma cut with an appropriate plasma system.
How thick can the LT100 cut?
There is no universal cutting thickness determined by the torch alone.
Use verified recommended, maximum and severance data from the complete plasma cutting system.
What is the difference between LT100 and LTM100?
LT100 is the manual / handheld configuration.
LTM100 is the related machine / CNC configuration.
Does INWELT provide LT100 spare parts?
Yes.
INWELT supplies cutting tips, electrodes, diffusers, outside nozzles, spacers, torch-head components, cable assemblies and related accessories.
Does INWELT offer OEM LT100 plasma torches?
Yes.
OEM/ODM, private-label, connector, cable and consumable-kit configurations are available for qualified equipment manufacturers, distributors and importers.
Request a Quote for the INWELT LT100 Plasma Cutting Torch
For faster compatibility confirmation, provide:
Plasma cutter manufacturer and model
Rated output current
Existing torch model
HF starting method
Main connector photo
Pilot-arc connection photo
Trigger/control connector photo
Required torch lead
Required consumables
Estimated purchasing quantity
INWELT or private-label branding
INWELT can then confirm the appropriate LT100 complete torch and replacement-consumable configuration.
 English
 简体中文
 العربية
 Français
 Русский
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 ភាសាខ្មែរ
 Bahasa Melayu
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Čeština
 Монгол
 қазақ
 Српски
 हिन्दी
 فارسی
 Slovenčina
 Slovenščina
 Norsk
 Svenska
 українська
 Ελληνικά
 Suomi
 Latine
 Dansk
 বাংলা
 Hrvatski
 Afrikaans
 Gaeilge
 Eesti keel
 नेपाली
 Oʻzbekcha
 latviešu
 Azərbaycan dili
 Беларуская мова
 Bosanski
 Български
 ქართული
 Lietuvių